

[Efficient Pneumatic Conveying Solutions for Coffee Powder Transport]
For coffee processing facilities, managing the transportation of coffee powder efficiently is a critical operational challenge. Traditional methods like manual handling or mechanical conveyors often struggle with issues such as dust generation, product contamination, and uneven flow control. These problems can lead to increased labor costs, reduced product quality, and potential safety hazards in the production environment.
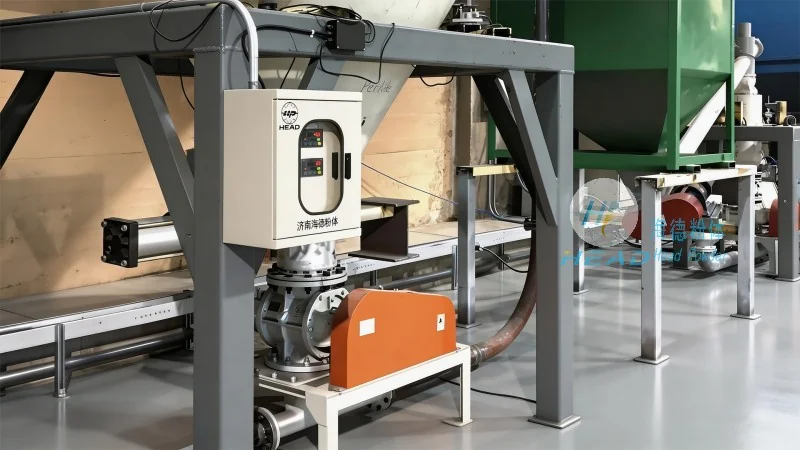
Coffee Powder Handling Challenges and the Need for Advanced Solutions
In the coffee industry, coffee powder is a delicate product that requires careful handling to preserve its flavor, aroma, and texture. Conventional transport methods may introduce moisture, temperature fluctuations, or physical damage, compromising the final product's quality. Additionally, the fine particles of coffee powder can create dust clouds, posing health risks to workers and requiring extensive cleaning measures. These challenges highlight the need for a reliable, hygienic, and efficient system that can handle coffee powder without compromising its integrity.
Pneumatic Conveying Systems: A Superior Approach to Coffee Powder Transport
Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder) specializes in developing and implementing advanced pneumatic conveying systems tailored for coffee powder applications. Pneumatic conveying uses air to transport bulk materials through a pipeline system, offering a hygienic, dust-free, and controlled method of handling coffee powder. This technology eliminates the need for manual handling, reduces product exposure to contaminants, and ensures consistent flow rates, which are essential for maintaining product quality and operational efficiency.
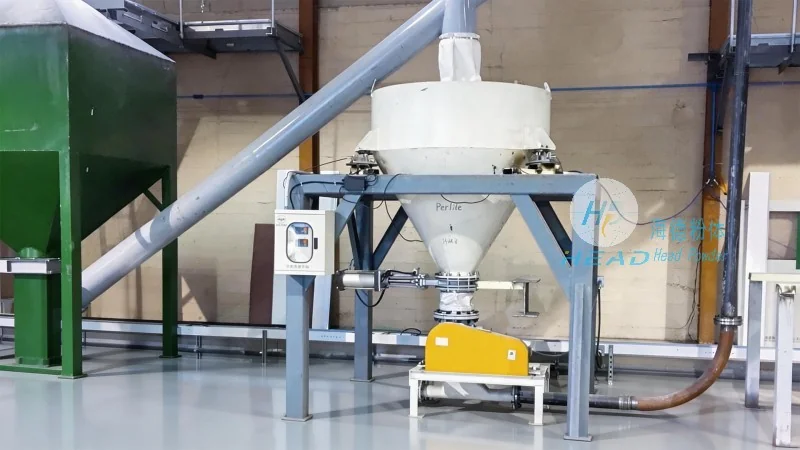
Key Features and Benefits of HeadPowder's Pneumatic Conveying Solutions
HeadPowder's pneumatic conveying systems are designed with several key features that address the specific needs of coffee powder handling. The systems utilize positive or negative pressure air flow to move coffee powder from storage silos to processing equipment, packaging lines, or storage areas. This approach provides precise control over the conveying rate, allowing operators to adjust flow based on production demands. Additionally, the enclosed pipeline design prevents dust dispersion, ensuring a clean and safe working environment. The systems are also equipped with filtration and cleaning mechanisms to maintain hygiene standards, which is crucial for food-grade applications.
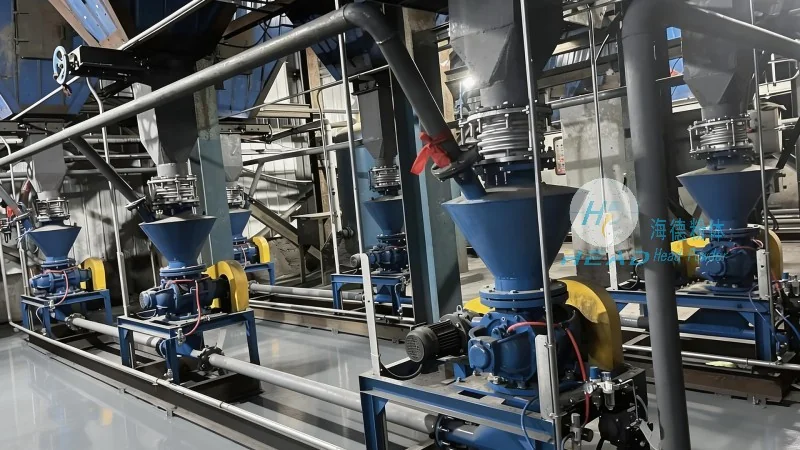
Customized Solutions for Diverse Coffee Processing Needs
HeadPowder understands that coffee processing facilities vary in size, production capacity, and operational requirements. Therefore, the company offers customized pneumatic conveying solutions that can be tailored to specific coffee powder handling challenges. Whether it's a small-scale roasting facility or a large industrial plant, HeadPowder's systems can be designed to handle different volumes and types of coffee powder, from freshly ground to pre-ground products. The company's engineering team works closely with clients to assess their current infrastructure, production processes, and future expansion plans, ensuring that the chosen system is both effective and scalable.
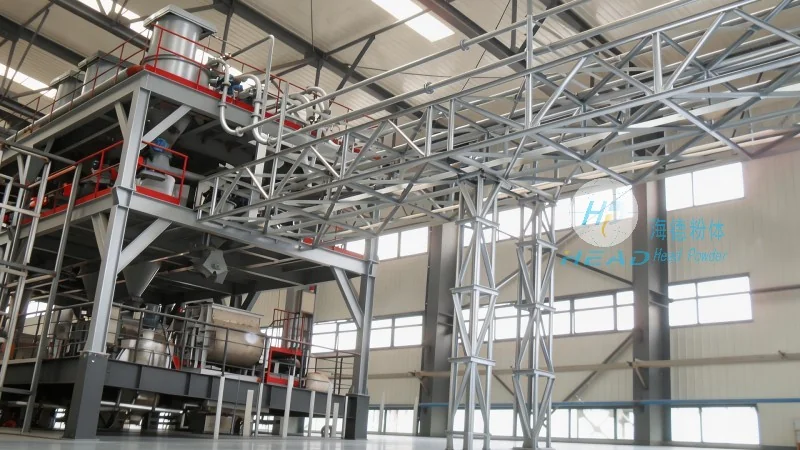
Ensuring Product Integrity and Compliance with Industry Standards
Preserving the quality of coffee powder is paramount for coffee manufacturers. HeadPowder's pneumatic conveying systems are built with materials that are food-grade and easy to clean, such as stainless steel, to prevent contamination and meet regulatory standards. The systems are also designed to minimize temperature changes during transport, which helps maintain the coffee's flavor and aroma. Furthermore, the enclosed design reduces exposure to external factors like humidity and air pollutants, further protecting the product's quality. By adhering to industry standards and best practices, HeadPowder ensures that its solutions not only improve operational efficiency but also maintain the highest quality of the coffee powder.
Conclusion: Enhancing Coffee Powder Handling with Pneumatic Conveying
Efficient coffee powder transport is essential for maintaining product quality, reducing operational costs, and ensuring a safe working environment in coffee processing facilities. Shandong HeadPowder Engineering Co., Ltd. provides advanced pneumatic conveying systems that address the unique challenges of coffee powder handling. By leveraging the benefits of pneumatic technology, HeadPowder's solutions help coffee manufacturers streamline their operations, improve product integrity, and achieve greater efficiency. With a focus on customized, hygienic, and reliable systems, HeadPowder is a trusted partner for coffee processing facilities seeking to enhance their coffee powder handling capabilities.