

Pneumatic Conveying in the Application of Bulk Transport for Coke and Stone Powder
Efficient and reliable bulk material handling is crucial in industrial processes, especially when dealing with materials like coke and stone powder. Pneumatic conveying technology offers a versatile solution that addresses the challenges of transporting these materials over long distances or within complex production environments. This method utilizes air to move powders and granules through a pipeline system, providing advantages such as reduced equipment wear, minimal product contamination, and the ability to handle a wide range of material types.
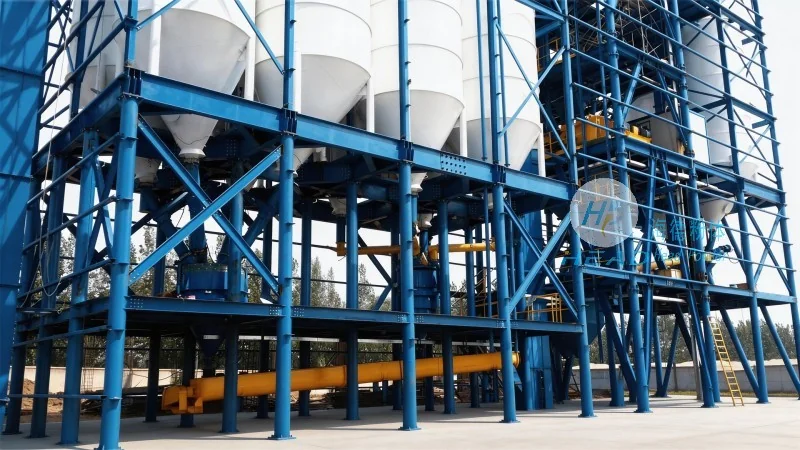
Key Benefits of Pneumatic Conveying for Coke and Stone Powder
When transporting coke and stone powder, traditional methods like belt conveyors or bucket elevators may face limitations due to material characteristics. Pneumatic conveying systems, however, excel in these scenarios. They eliminate the need for multiple transfer points, which can be prone to blockages or spillage. The enclosed pipeline design ensures that the material remains contained, preventing dust emissions and maintaining a clean working environment. Additionally, these systems can operate at varying pressures, allowing for flexible control over the flow rate and distance of transport. This adaptability makes them suitable for both short-distance and long-distance applications, from plant-wide material movement to inter-site logistics.
HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced pneumatic conveying systems tailored to the unique requirements of coke and stone powder industries. With years of experience in the field, the company has developed a comprehensive range of solutions that cater to different operational needs. HeadPowder's systems are engineered to handle the abrasive nature of coke and the fine particle size of stone powder, ensuring long-term durability and performance. The company's approach involves a thorough understanding of the material's physical properties, such as density, moisture content, and flowability, which are critical factors in optimizing the conveying process.
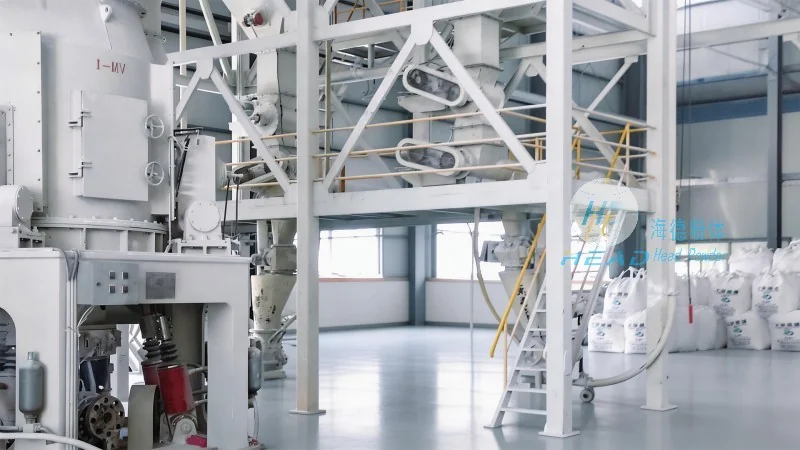
Customized Solutions for Diverse Applications
HeadPowder recognizes that each industrial facility has distinct operational parameters and space constraints. Therefore, the company offers customized pneumatic conveying solutions that are tailored to specific project requirements. Whether the application involves transporting coke from a storage silo to a furnace or moving stone powder from a quarry to a processing plant, HeadPowder's engineers work closely with clients to design systems that maximize efficiency and minimize operational costs. The solutions may include different types of pneumatic conveying technologies, such as pressure or vacuum systems, depending on the distance and material characteristics. For example, pressure systems are often used for long-distance transport, while vacuum systems are suitable for shorter distances or when handling materials with lower flowability.
Ensuring Safety and Compliance
Industrial safety is a top priority in the design and operation of pneumatic conveying systems for coke and stone powder. HeadPowder's solutions incorporate safety features that comply with industry standards and regulations. These include dust suppression systems to control airborne particles, pressure relief valves to prevent over-pressurization, and emergency shut-off mechanisms. The company also adheres to environmental regulations by implementing measures to minimize dust emissions and ensure proper waste disposal. By prioritizing safety and compliance, HeadPowder provides clients with reliable systems that not only enhance operational efficiency but also contribute to a safer working environment.
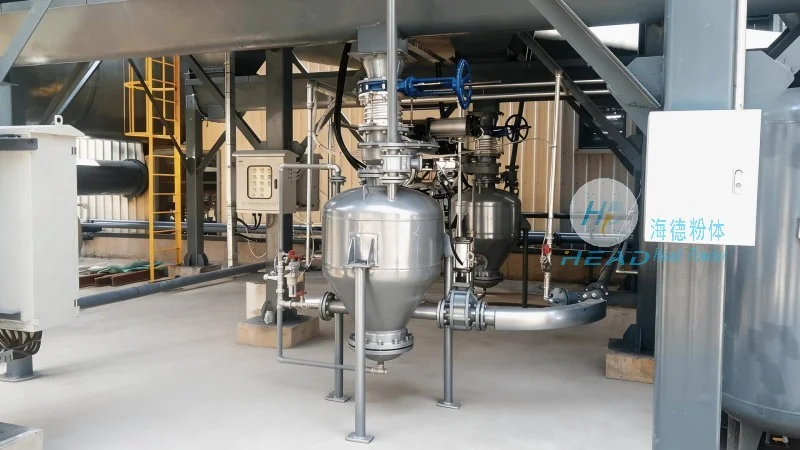
Case Studies and Real-World Applications
HeadPowder's expertise is demonstrated through successful implementations in various industrial settings. For instance, a steel plant in China utilized a pneumatic conveying system to transport coke from a storage facility to the blast furnace, achieving a significant reduction in handling time and labor costs. Similarly, a quarry processing plant implemented a system to move stone powder to a grinding mill, improving production throughput and reducing material loss. These case studies highlight the effectiveness of HeadPowder's solutions in addressing the specific challenges faced by coke and stone powder industries. The company's commitment to quality and customer satisfaction is evident in the positive feedback from clients who have experienced enhanced operational performance and cost savings.
Conclusion: Choosing the Right Pneumatic Conveying System
For industries dealing with coke and stone powder, selecting the appropriate pneumatic conveying system is essential for optimizing material handling processes. HeadPowder Engineering Co., Ltd. stands out as a trusted partner, offering customized solutions that leverage advanced technology and industry expertise. By understanding the unique properties of coke and stone powder, HeadPowder designs systems that ensure efficient, safe, and cost-effective transport. Whether for short or long-distance applications, the company's solutions provide the reliability needed to support continuous production and meet growing demand. With a focus on quality, safety, and customer satisfaction, HeadPowder continues to be a leader in providing pneumatic conveying solutions for the coke and stone powder sectors.