

Principle of Stone Aggregate Pneumatic Conveying System
The stone aggregate pneumatic conveying system is a sophisticated technology designed to transport bulk materials like stone aggregates, gravel, and similar granular substances through a pipeline using air as the conveying medium. This method offers significant advantages over traditional mechanical conveying systems, such as reduced equipment wear, lower energy consumption, and enhanced safety in handling abrasive materials. The system operates by creating a flow of air within the pipeline, which lifts and transports the material particles through the system. Understanding the core principles of this technology is essential for optimizing its application in various industrial settings.
Core Components and Working Mechanism
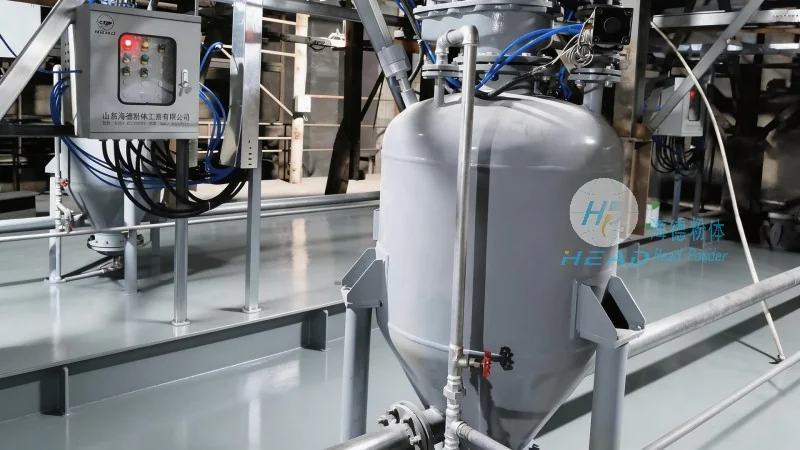
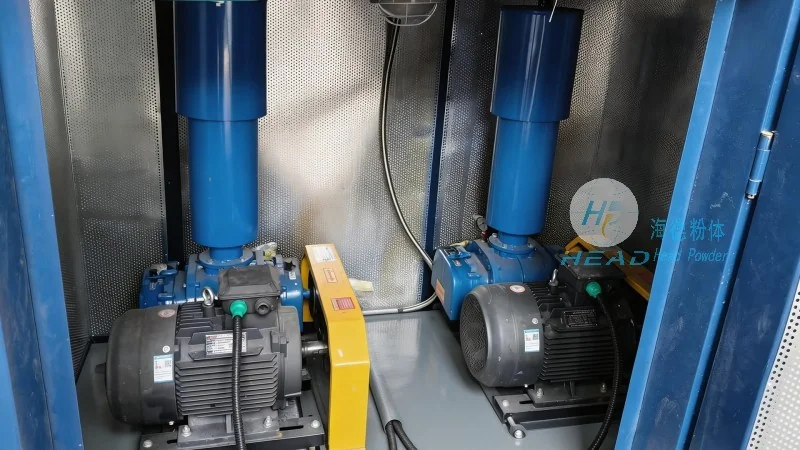
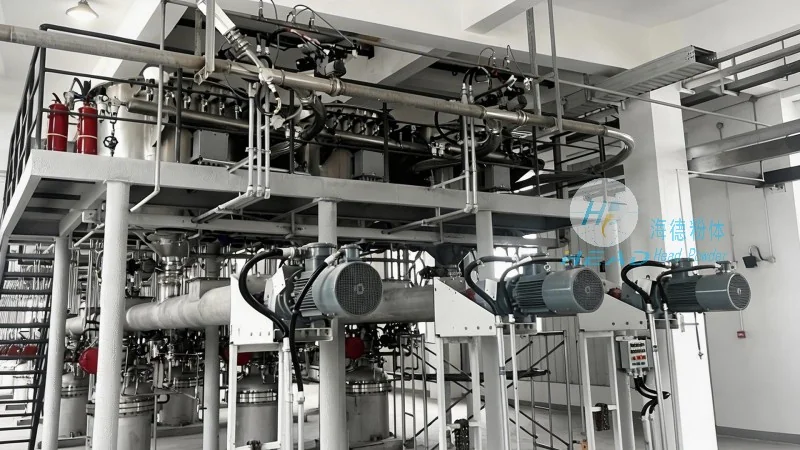
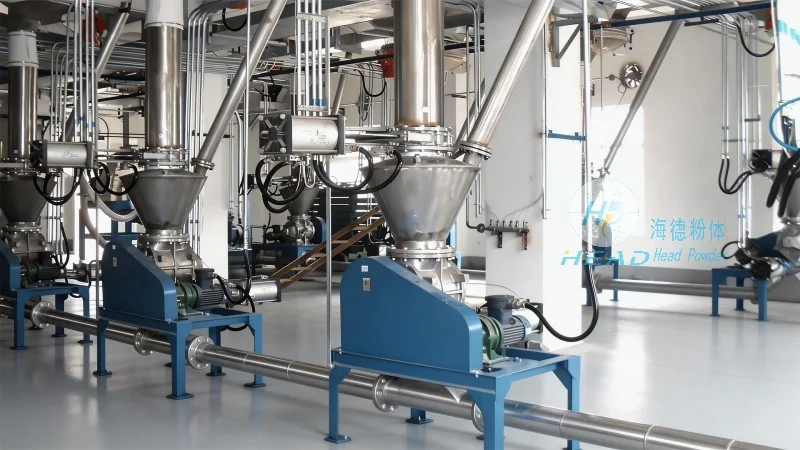
The pneumatic conveying system for stone aggregates typically consists of several key components, each playing a crucial role in the overall operation. The primary components include a material hopper, a feeder, a conveying pipeline, a pressure or vacuum source, and a receiver or discharge unit. The material hopper stores the stone aggregates and feeds them into the system at a controlled rate. The feeder, often a rotary valve or a screw feeder, regulates the flow of material into the pipeline. The conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, transports the material and air mixture. The pressure or vacuum source, such as a blower or a vacuum pump, generates the necessary air flow to move the material. The receiver or discharge unit collects the conveyed material at the end of the pipeline.
The working mechanism involves the feeder introducing the stone aggregates into the pipeline while the air source creates a pressure differential. In a pressure system, the air is forced through the pipeline, carrying the material particles forward. In a vacuum system, the air is drawn through the pipeline, pulling the material from the hopper to the receiver. The air velocity within the pipeline must be sufficient to overcome the gravitational forces and frictional losses, ensuring the material is fully suspended and transported efficiently. The system's design, including the pipeline diameter, length, and air flow rate, is critical to achieving optimal conveying performance and minimizing material degradation.
Advantages of Pneumatic Conveying for Stone Aggregates
Compared to traditional mechanical conveying methods like belt conveyors or bucket elevators, the pneumatic conveying system offers several distinct advantages for handling stone aggregates. One of the most significant benefits is the reduction in equipment wear and tear. Since the material is conveyed within a pipeline without direct contact with mechanical components, the system experiences less abrasion and corrosion, leading to longer equipment life and lower maintenance costs. Additionally, pneumatic conveying systems are more energy-efficient, as they can transport materials over longer distances with less power consumption compared to mechanical systems. The system also provides better safety in handling abrasive materials, as there are no moving parts that could cause injury or material spillage. Furthermore, the system allows for flexible and compact installation, as the pipeline can be routed around obstacles and in tight spaces, making it suitable for various industrial applications.
Application Scenarios and Industrial Use Cases
The stone aggregate pneumatic conveying system is widely used in various industries that require the transport of bulk materials. In the construction industry, it is commonly used to transport gravel, sand, and other aggregates from storage silos to concrete mixing plants or batching stations. The system can also be used in mining operations to transport crushed stone or ore from processing facilities to storage areas or for further processing. In the chemical and pharmaceutical industries, the system is used to transport raw materials like limestone or silica sand, which are often abrasive and require gentle handling. The system is also suitable for applications in the food and agricultural sectors, where it can transport grains, seeds, or other bulk food products. The flexibility and efficiency of the pneumatic conveying system make it an ideal choice for industries that require reliable and low-maintenance material transport solutions.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related industrial equipment. The company specializes in designing and manufacturing customized solutions for various bulk material handling applications, including stone aggregate transportation. With years of experience in the industry, headpowder has developed a reputation for quality, reliability, and innovation. The company's products are designed to meet the specific needs of different industries, ensuring optimal performance and efficiency. Headpowder's team of engineers and technicians work closely with clients to understand their requirements and provide tailored solutions that address their unique challenges. The company's commitment to quality and customer satisfaction has made it a trusted partner for many businesses in the bulk material handling sector.
Technical Specifications and Customization Options
Headpowder offers a range of pneumatic conveying systems for stone aggregates, with technical specifications tailored to different application requirements. The systems can be customized in terms of pipeline diameter, length, and air flow rate to suit the specific needs of the client. The company uses high-quality materials, such as stainless steel and corrosion-resistant alloys, to ensure the durability and longevity of the equipment. The systems are also equipped with advanced control systems that allow for precise regulation of the material flow and air pressure, ensuring optimal performance. Headpowder's technical team provides comprehensive support, including installation, commissioning, and maintenance services, to ensure the smooth operation of the system. The company's focus on customization and technical expertise makes it a preferred choice for businesses looking for reliable and efficient stone aggregate conveying solutions.