

What is a cement raw material handling system? And what are its design principles?
Cement raw material handling systems are integral to the cement production process, responsible for the efficient transport of raw materials from their source to the grinding and mixing stages. These systems are crucial for maintaining the continuity of cement manufacturing, which is vital for construction projects worldwide. The design and implementation of such systems directly impact the efficiency, cost-effectiveness, and overall performance of a cement plant.
Core Components of Cement Raw Material Handling Systems
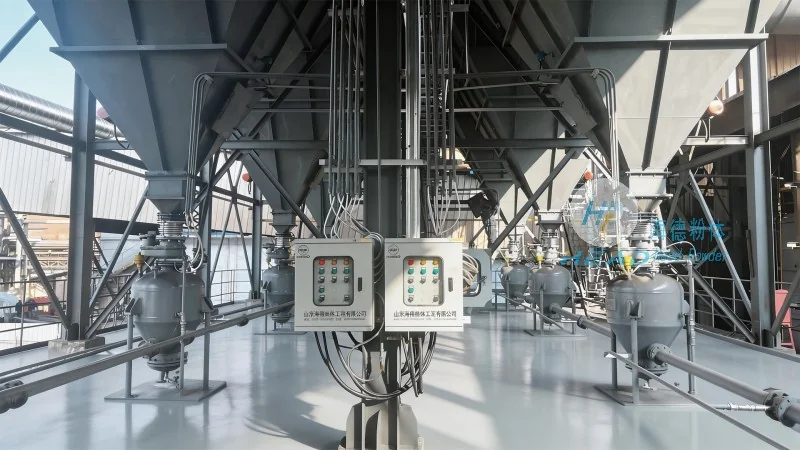
The fundamental components of a cement raw material handling system typically include raw material storage facilities, conveyors, feeders, and processing equipment. Raw materials like limestone, clay, and iron ore are first stored in large silos or stockpiles to ensure a steady supply. From these storage areas, materials are transported to the grinding mills using various types of conveyors. Belt conveyors are commonly used for long-distance horizontal transport due to their high capacity and low maintenance requirements. Bucket elevators, on the other hand, are ideal for vertical transport, efficiently lifting materials to elevated processing levels. Feeders, such as rotary or vibratory types, regulate the flow of materials into the grinding mills, ensuring consistent feed rates that optimize grinding efficiency and prevent equipment overload.
Design Principles for Optimal Material Handling
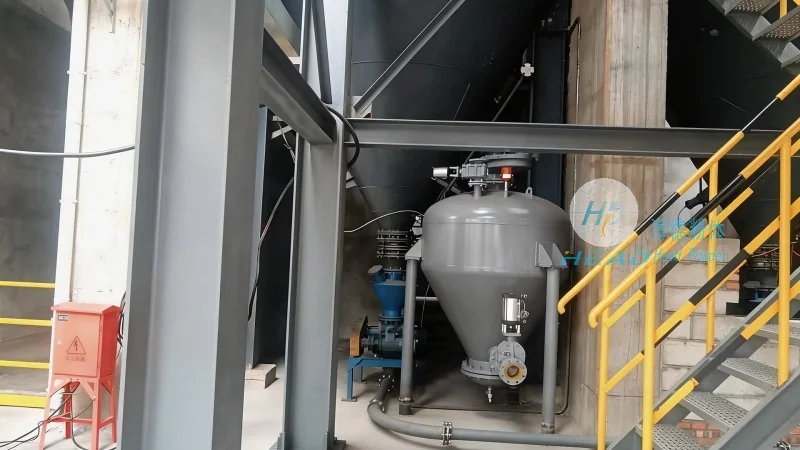
The design of a cement raw material handling system is guided by several key principles aimed at maximizing efficiency, minimizing energy consumption, and ensuring operational reliability. One of the primary principles is the optimization of material flow, which involves designing a layout that minimizes the total distance materials travel and reduces the number of transfer points. This approach not only lowers energy costs but also reduces the risk of material degradation or loss during transport. Another critical principle is the selection of appropriate equipment based on the physical properties of the raw materials, such as particle size distribution, moisture content, and bulk density. For instance, heavy-duty belt conveyors are often preferred for transporting large volumes of limestone, while bucket elevators may be more suitable for handling fine powders like clay. Additionally, the design considers factors like material compatibility with equipment components to prevent wear and tear, ensuring longer equipment life and lower maintenance costs.
Customized Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a reputable manufacturer specializing in industrial material handling solutions, offers comprehensive services for cement raw material handling systems. The company's approach is centered on understanding the unique requirements of each cement plant, providing tailored designs that enhance production efficiency and reduce operational costs. HeadPowder's team of experienced engineers leverages advanced engineering principles and industry best practices to develop systems that meet the specific needs of clients. The company's product line includes a wide range of equipment, from belt conveyors and bucket elevators to feeders and storage silos, all designed to work in harmony to create a seamless material handling process. By focusing on durability and low maintenance, HeadPowder ensures that its systems can withstand the harsh operating conditions typical of cement production environments. The company's commitment to quality is evident in its adherence to international standards and rigorous testing protocols, ensuring that each system is reliable and long-lasting. With offices and operations based in Shandong, China, HeadPowder serves clients globally, providing expert consultation and support throughout the entire project lifecycle. The company's dedication to customer satisfaction has earned it a strong reputation in the cement industry, making it a trusted partner for plants seeking to upgrade or expand their material handling capabilities.
Conclusion: The Role of Well-Designed Systems in Cement Production
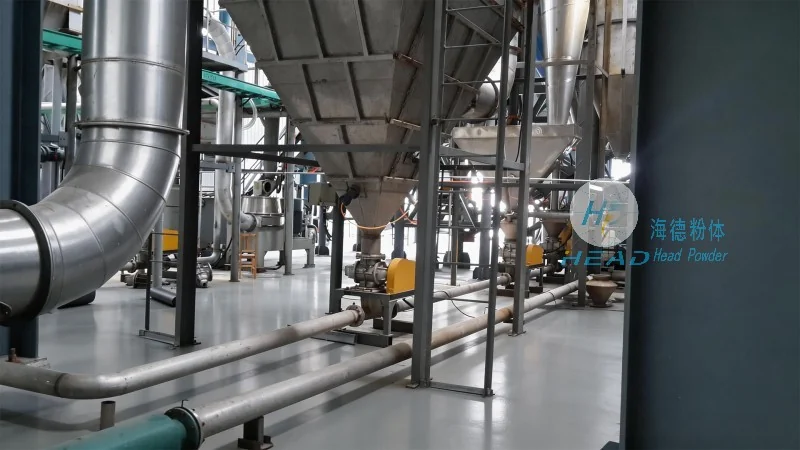
In summary, cement raw material handling systems are essential to the success of cement manufacturing operations. Their design must balance efficiency, cost, and reliability to support the high demands of modern cement production. By adhering to sound engineering principles and leveraging advanced technology, manufacturers can achieve optimal material flow, reduce energy consumption, and minimize downtime. Shandong HeadPowder Engineering Co., Ltd. exemplifies the industry's commitment to providing high-quality, customized solutions that meet the evolving needs of cement plants. Through its expertise and dedication to excellence, HeadPowder continues to contribute to the advancement of cement production technology, helping plants worldwide improve their productivity and maintain a competitive edge in the market.