

Working Principle and Characteristics of Ammonium Nitrate Pneumatic Conveying
Ammonium nitrate (AN) is a critical industrial chemical used extensively in fertilizer production, explosives, and various chemical processes. The efficient and safe handling of AN is paramount for industrial operations, and pneumatic conveying systems have become a preferred solution for transporting this material. This article delves into the working principle and key characteristics of ammonium nitrate pneumatic conveying, offering a comprehensive overview of how these systems function and their advantages in industrial settings.
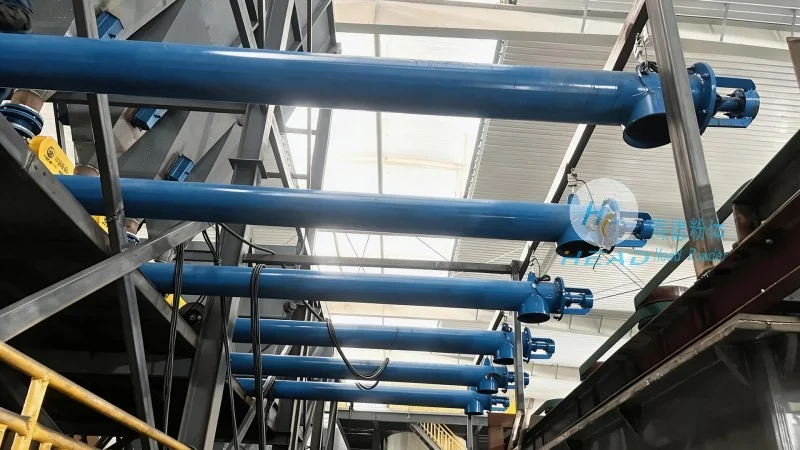
The Working Principle of Ammonium Nitrate Pneumatic Conveying
The operation of an ammonium nitrate pneumatic conveying system revolves around the use of air or gas to transport solid particles. The process begins with the material being fed from a hopper or feeder into the system. A fan or blower then generates a high-velocity airflow, which draws the ammonium nitrate particles into the conveying pipeline. The air-particle mixture travels through the pipeline, with the air providing the necessary force to move the material. At the discharge point, the air is separated from the powder, typically using a cyclone separator or filter, and the air is either recirculated or vented. This continuous process ensures consistent and reliable transport of the ammonium nitrate, minimizing material loss and maintaining safety due to the chemical's properties.
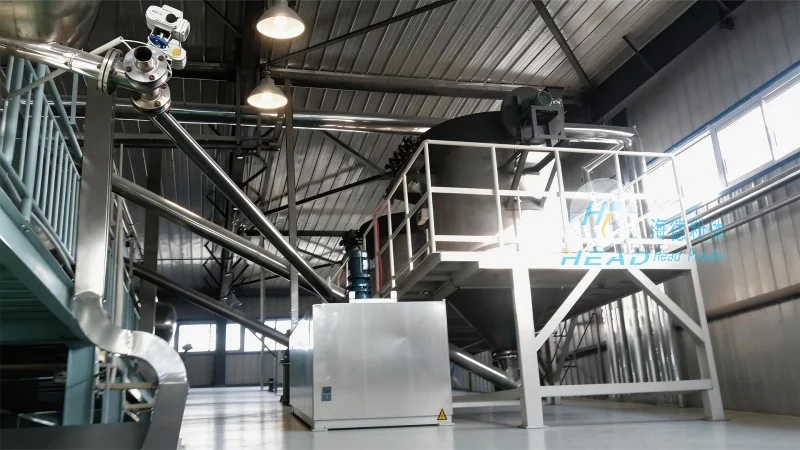
Key Characteristics of Ammonium Nitrate Pneumatic Conveying Systems
Ammonium nitrate pneumatic conveying systems possess several distinct characteristics that make them ideal for industrial applications. One of the primary benefits is the ability to handle fine powders without the need for mechanical components that could cause wear or contamination. The system's design minimizes the risk of dust explosions by maintaining a controlled environment and utilizing explosion-proof materials. Additionally, pneumatic conveying offers flexibility in layout, as the conveying lines can be configured to suit the plant's specific layout requirements. Another notable characteristic is the system's efficiency in terms of energy consumption and material throughput. Modern systems are equipped with advanced controls that optimize air flow and pressure, reducing energy costs while ensuring high transport speeds. The integrated safety features, such as explosion-proof fans and proper ventilation, are also crucial for handling ammonium nitrate, which is a hazardous material under certain conditions.
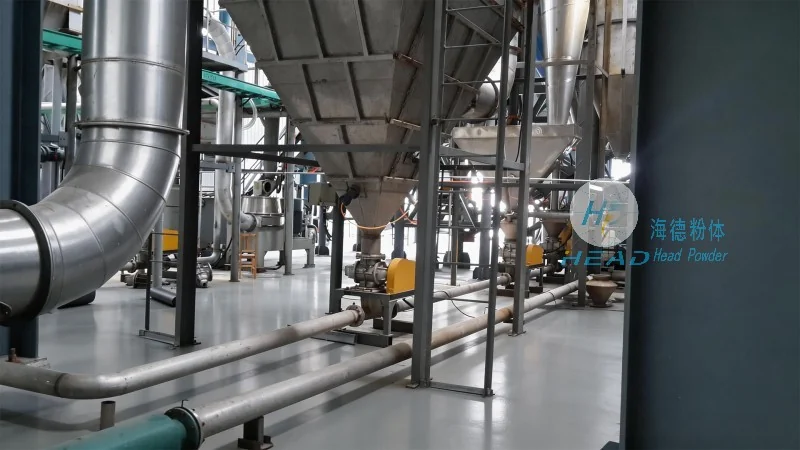
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer and supplier of industrial conveying solutions, specializing in systems for handling ammonium nitrate and other bulk materials. HeadPowder has built a reputation for innovation and customer-centric approaches, developing advanced pneumatic conveying technologies tailored to the unique needs of the fertilizer and chemical industries. The company's expertise lies in designing and manufacturing systems that ensure safe, efficient, and reliable transport of ammonium nitrate, adhering to stringent safety and quality standards. HeadPowder's facilities are located in Shandong, China, where it leverages local resources and technical expertise to deliver high-quality products and services to clients globally.