

Working Principle and Features of Corn Starch Pneumatic Conveying Systems
Corn starch is a widely used raw material in various industries, including food processing, pharmaceuticals, and chemical manufacturing. The efficient and reliable transportation of corn starch from storage to processing units is crucial for maintaining production efficiency and product quality. Pneumatic conveying systems have emerged as a preferred solution for handling corn starch due to their ability to transport powders in a closed, dust-free environment. This article explores the working principle and key features of corn starch pneumatic conveying systems, highlighting how they enhance operational performance and safety in industrial settings.
Working Principle of Corn Starch Pneumatic Conveying Systems
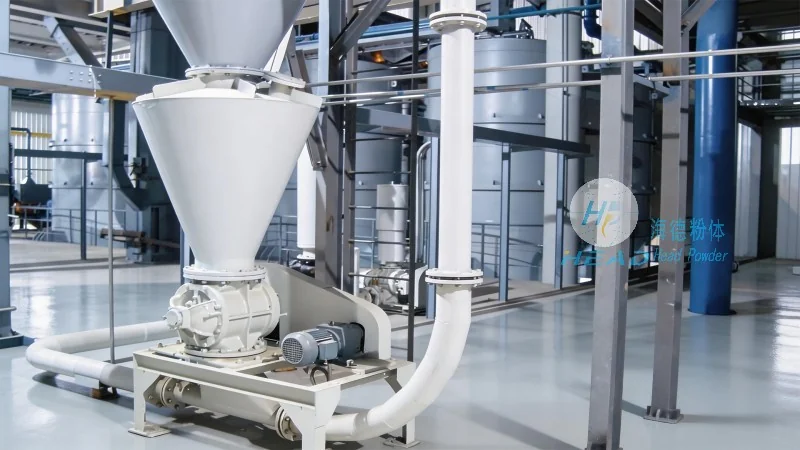
The core of a corn starch pneumatic conveying system is the use of compressed air to move the starch particles through a pipeline. The system typically consists of a hopper, a feeder, a conveying line, and a receiver. The process begins when corn starch is fed into the hopper from a storage silo. The feeder then meters the starch at a controlled rate into the conveying line. Compressed air, supplied by a blower or air compressor, is introduced into the line, creating a pressure differential that propels the starch particles forward. The air and starch mixture travels through the pipeline, with the air providing the necessary force to overcome friction and gravity. At the receiving end, the air is separated from the starch, often using a cyclone separator or a filter, and the starch is deposited into the target container. The air is then either recirculated or vented to the atmosphere, depending on the system design. This closed-loop operation ensures minimal dust generation and environmental contamination, making it ideal for handling fine powders like corn starch.
Key Features of Corn Starch Pneumatic Conveying Systems
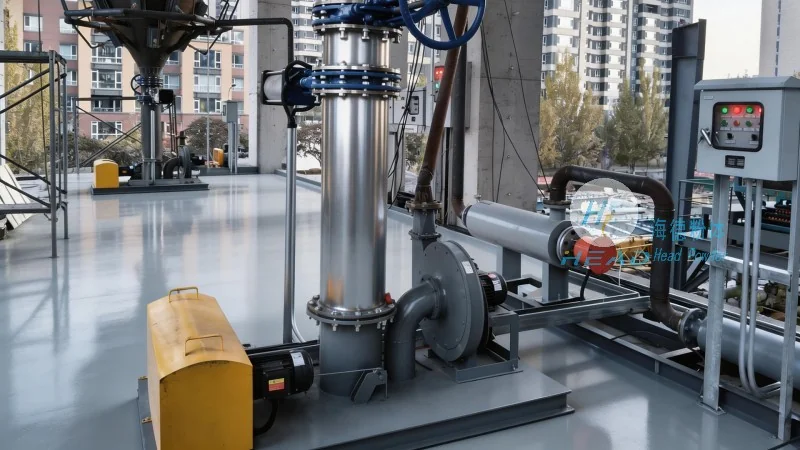
Several key features distinguish corn starch pneumatic conveying systems from other material handling methods. First, the closed system design eliminates the risk of dust dispersion, which is critical for maintaining a safe working environment and complying with environmental regulations. Second, the system offers high transport efficiency, with the ability to move large volumes of starch over long distances with minimal energy consumption compared to traditional methods like bucket elevators or belt conveyors. Third, the gentle handling of the starch particles prevents agglomeration and degradation, preserving the quality and properties of the product. Fourth, the system is highly flexible, allowing for easy integration with existing production lines and the ability to adjust flow rates and pressure settings to meet varying production demands. Additionally, the use of stainless steel or other corrosion-resistant materials in the construction of the conveying lines ensures durability and resistance to the acidic or alkaline properties of corn starch, extending the system's service life. These features collectively contribute to improved operational efficiency, reduced maintenance costs, and enhanced product quality in corn starch processing facilities.
Applications and Benefits in Industrial Settings
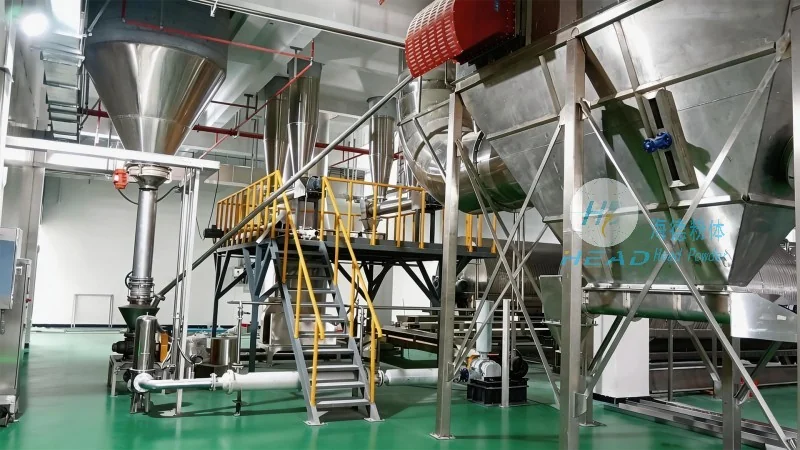
Corn starch pneumatic conveying systems are widely adopted in industries where the handling of fine powders is essential. In the food industry, they are used to transport starch from storage to mixing and processing equipment, ensuring a hygienic and efficient workflow. In the pharmaceutical sector, the closed system design is particularly important for maintaining product purity and preventing contamination, as even small amounts of dust can affect the quality of medicinal products. Similarly, in the chemical industry, the system's ability to handle corrosive or sensitive powders makes it suitable for applications involving starch-based chemicals. The benefits of these systems extend beyond operational efficiency; they also contribute to cost savings through reduced material loss, lower energy consumption, and minimized downtime due to maintenance. Furthermore, the system's compact design allows for space optimization in industrial facilities, making it suitable for both new installations and retrofitting existing plants. By integrating a corn starch pneumatic conveying system, companies can achieve improved productivity, enhanced safety, and compliance with industry standards, ultimately leading to a competitive advantage in their respective markets.
Conclusion
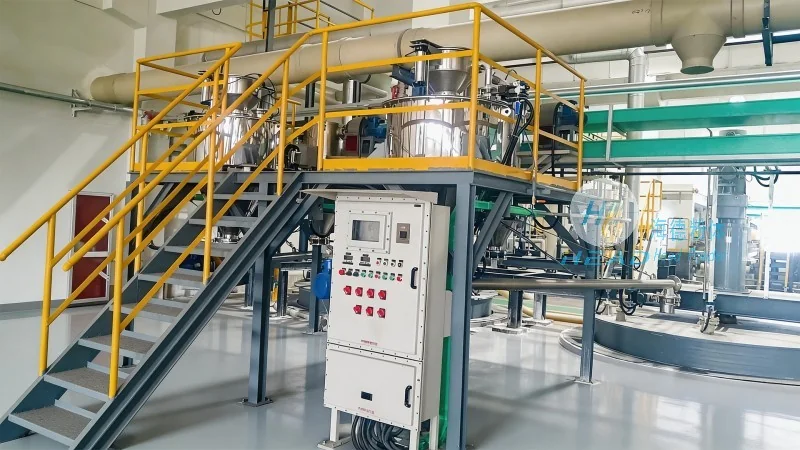
In summary, corn starch pneumatic conveying systems represent a sophisticated and efficient solution for the transportation of fine powders in industrial applications. Their working principle, based on compressed air and a closed pipeline system, ensures reliable and dust-free operation, while their key features, such as high efficiency, gentle handling, and flexibility, address the specific needs of corn starch processing. The adoption of such systems by companies like Shandong HeadPowder Engineering Co., Ltd. has proven to enhance operational performance and product quality, contributing to the overall success of corn starch processing operations. As the demand for efficient material handling solutions continues to grow, the role of pneumatic conveying systems in the corn starch industry is likely to expand, making them an indispensable component of modern industrial processes.