

Working Principle and Features of Multi-functional Pneumatic Conveying Equipment
Multi-functional pneumatic conveying equipment is a critical component in modern material handling systems, designed to efficiently transport bulk materials through the use of air pressure. Understanding its working principle and key features is essential for industries seeking reliable and versatile solutions for material movement. This article provides an in-depth look at how these systems operate and the advantages they offer.
Working Principle of Multi-functional Pneumatic Conveying Equipment
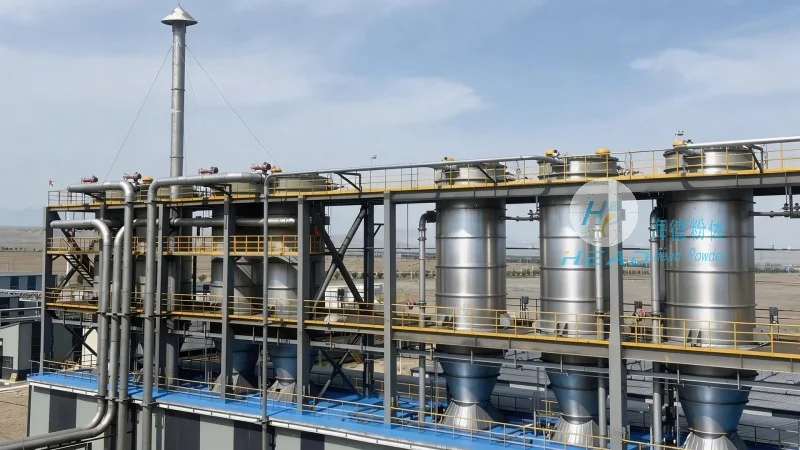
The core mechanism of multi-functional pneumatic conveying equipment involves the use of compressed air to move materials from a source to a destination. The process typically begins with the material being introduced into a hopper or feeder, where it is then fed into a pipeline. Compressed air, generated by a blower or compressor, is introduced into the pipeline, creating a flow that propels the material forward. This method, known as pneumatic conveying, relies on the air's kinetic energy to transport dry, free-flowing materials such as powders, granules, and small particles. The equipment often includes components like airlocks, cyclones, and filters to ensure efficient material transfer and to maintain system cleanliness. The working principle can be categorized into two main types: pressure and vacuum systems. Pressure systems use compressed air to push material through the pipeline, while vacuum systems use suction to draw material from the source. Multi-functional models may incorporate both types, allowing for greater flexibility in handling different material properties and system configurations.
Key Features of Multi-functional Pneumatic Conveying Equipment
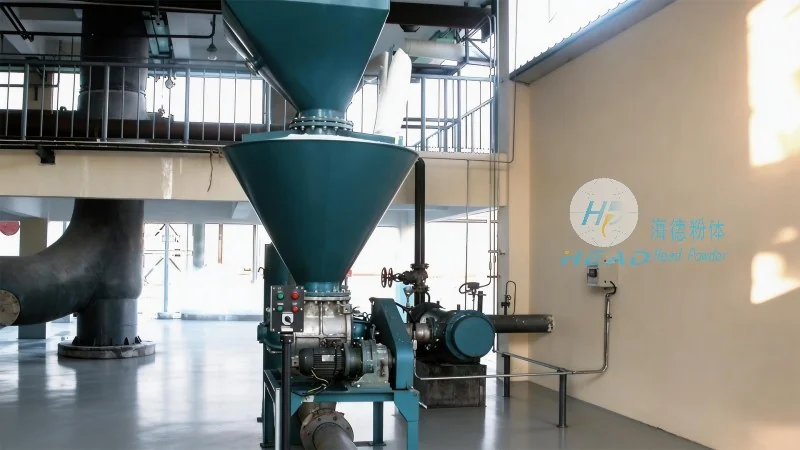
Multi-functional pneumatic conveying equipment offers several distinct features that enhance its performance and adaptability. One of the primary advantages is its ability to handle a wide range of materials, including fine powders, coarse granules, and even sticky or abrasive substances. This versatility makes it suitable for various industries, such as food processing, pharmaceuticals, chemicals, and mining. The equipment is also designed for high efficiency, with minimal material loss and low maintenance requirements. Advanced models often include adjustable air flow controls, allowing operators to optimize the conveying process for different material types and system loads. Additionally, these systems are equipped with safety features, such as pressure relief valves and air filtration systems, to ensure safe and reliable operation. The modular design of multi-functional equipment enables easy integration into existing production lines, reducing installation time and costs. Another notable feature is the ability to handle long-distance conveying, with some models capable of transporting materials over several hundred meters without significant loss of efficiency. This makes them ideal for large-scale operations where material movement over extended distances is required.
Applications and Industries
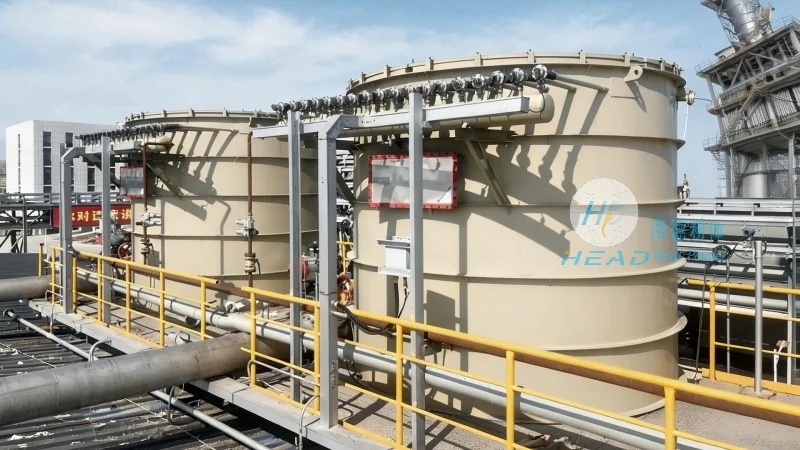
Multi-functional pneumatic conveying equipment is widely used across various industries due to its adaptability and efficiency. In the food and beverage industry, it is commonly used for transporting ingredients like flour, sugar, and spices, ensuring hygienic and dust-free handling. The pharmaceutical industry relies on these systems for conveying active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict contamination control. In the chemical industry, the equipment is used to transport powders and granules, such as fertilizers and pigments, while minimizing dust exposure and ensuring safe handling. The mining and minerals sector also benefits from these systems, as they efficiently convey raw materials like ores and coal from processing plants to storage facilities. Additionally, the equipment is used in the plastics and ceramics industries for transporting raw materials and finished products, supporting high-speed production lines. The versatility of multi-functional pneumatic conveying equipment makes it a valuable asset in any operation where material handling is a critical process.
Advantages of Choosing Multi-functional Pneumatic Conveying Equipment
Investing in multi-functional pneumatic conveying equipment offers numerous benefits for businesses. The primary advantage is the significant reduction in labor costs, as automated systems eliminate the need for manual material handling. This not only improves efficiency but also enhances workplace safety by reducing the risk of accidents associated with manual lifting and moving. The equipment also contributes to improved product quality by minimizing material contamination and degradation during transport. With precise control over air flow and pressure, operators can ensure consistent material delivery, which is crucial for maintaining product quality and meeting regulatory standards. Another key advantage is the space-saving design, as these systems can be installed in compact areas, making them ideal for facilities with limited space. The modular construction allows for easy expansion or modification as production needs change, providing long-term value and adaptability. Furthermore, the low maintenance requirements and long service life of these systems result in lower operational costs over time. The ability to handle a wide range of materials without the need for multiple systems also reduces inventory and storage costs, as businesses can rely on a single, versatile equipment for various material handling tasks.

Conclusion
Multi-functional pneumatic conveying equipment is a sophisticated and versatile solution for material handling, offering efficient, reliable, and safe transport of bulk materials. Its working principle, based on compressed air, allows for the seamless movement of various materials over long distances with minimal loss and contamination. The key features, including adaptability, efficiency, and safety, make it an ideal choice for industries ranging from food and pharmaceuticals to chemicals and mining. By understanding the working principle and advantages of these systems, businesses can make informed decisions to enhance their material handling processes and improve overall operational efficiency. For those seeking a reliable and versatile material transport solution, multi-functional pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. provides a robust and effective option, backed by years of industry expertise and commitment to quality.