

Working Principle and Features of Denitrizer Pneumatic Conveying Systems
Denitrizer pneumatic conveying systems are critical equipment in industrial processes, especially in facilities managing nitrogen oxide reduction. Understanding their working principles and key characteristics is vital for optimizing operational efficiency and ensuring compliance with environmental regulations. This article provides a detailed overview of the working principle and features of denitrizer pneumatic conveying systems, presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China.
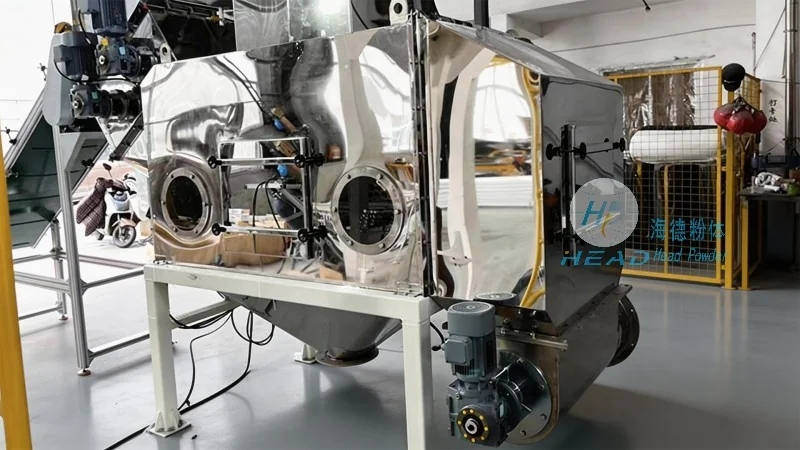
Introduction to Denitrizer Pneumatic Conveying Systems
Denitrizer pneumatic conveying systems are designed to transport denitrizer powders, such as urea or ammonia-based compounds, from storage silos or bulk containers to injection points in industrial furnaces or boilers. These systems utilize pneumatic transport principles, where a stream of air or gas moves solid particles through a pipeline network. Compared to traditional mechanical conveying, this technology offers advantages like reduced material degradation, lower maintenance needs, and enhanced safety by eliminating manual powder handling.
Working Principle of Denitrizer Pneumatic Conveying Systems
The core working principle involves creating a pressure differential between the material inlet and outlet. Systems typically operate in positive or negative pressure modes. In a positive pressure system, compressed air is introduced at the inlet, forcing the powder through the pipeline with air as a carrier. The air-powder mixture travels to the discharge point, where air is separated from the powder (e.g., via cyclone separators or filters). Negative pressure systems draw air from the discharge end, creating a vacuum to pull powder from the source. Both rely on air velocity to maintain particle suspension and prevent pipeline clogging.
Key Features of Denitrizer Pneumatic Conveying Systems
Denitrizer pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. include several key features enhancing performance and reliability:
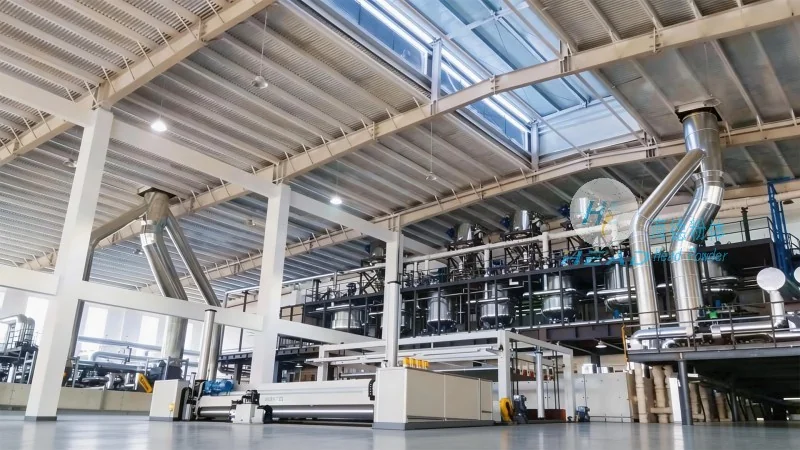
1. Adjustable Airflow and Pressure Control: Variable speed drives and pressure regulators allow operators to adjust airflow and pressure based on powder properties and conveying distance. This flexibility optimizes efficiency and prevents material degradation from excessive air velocity.
2. Durable and Corrosion-Resistant Materials: Pipeline components (hoppers, ducts, valves) use stainless steel or special alloys resistant to corrosion from denitrizer powders and air. This ensures long-term durability and minimal maintenance.
3. Advanced Filtration and Separation: High-efficiency filters and cyclone separators maintain powder purity and protect downstream equipment. They effectively separate air from powder, ensuring only denitrizer reaches injection points while air is recirculated or safely discharged.
4. Automated Control and Monitoring: Modern systems feature advanced control panels and monitoring for real-time tracking of pressure, flow rate, and material levels. This automation enhances safety and enables quick adjustments to process changes.
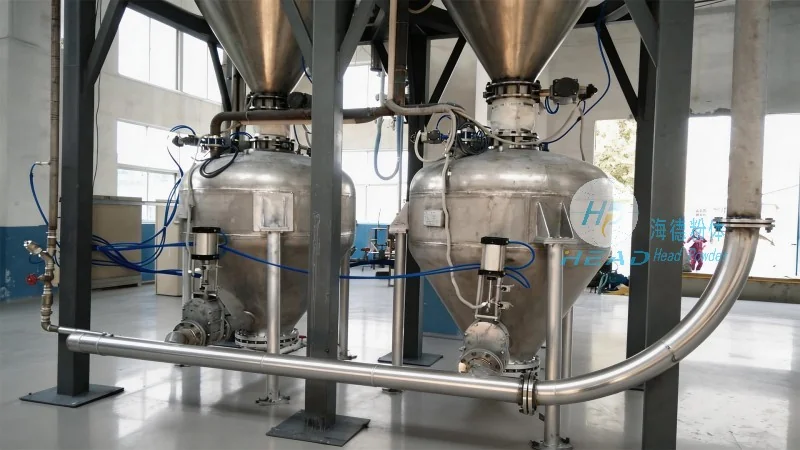
5. Compact and Space-Efficient Design: Engineered with compact layouts to minimize installation footprint, suitable for facilities with limited space. This design also simplifies integration with existing industrial infrastructure.
Applications and Benefits of Denitrizer Pneumatic Conveying Systems
Denitrizer pneumatic conveying systems are widely used in power generation, steel manufacturing, and chemical processing. Primary benefits include improved process efficiency, reduced material waste, enhanced safety from manual handling elimination, and compliance with strict environmental regulations. By ensuring consistent denitrizer supply to injection points, these systems help better control nitrogen oxide emissions, reducing environmental impact and operational costs.
Conclusion
Denitrizer pneumatic conveying systems, exemplified by products from Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated solution for efficient and safe denitrizer powder transport in industrial applications. By understanding their working principles and leveraging key features, facilities can optimize nitrogen oxide reduction processes, enhance operational performance, and meet environmental standards effectively. With a commitment to quality and innovation, Shandong HeadPowder Engineering Co., Ltd. continues to provide reliable and efficient denitrizer pneumatic conveying systems to meet evolving industrial needs.