Understanding the working principle and features of potassium hydroxide (KOH) powder conveying systems is crucial for industries that rely on efficient and safe handling of this caustic chemical. This article provides a detailed overview of how these systems operate and the key characteristics that make them effective for various applications.
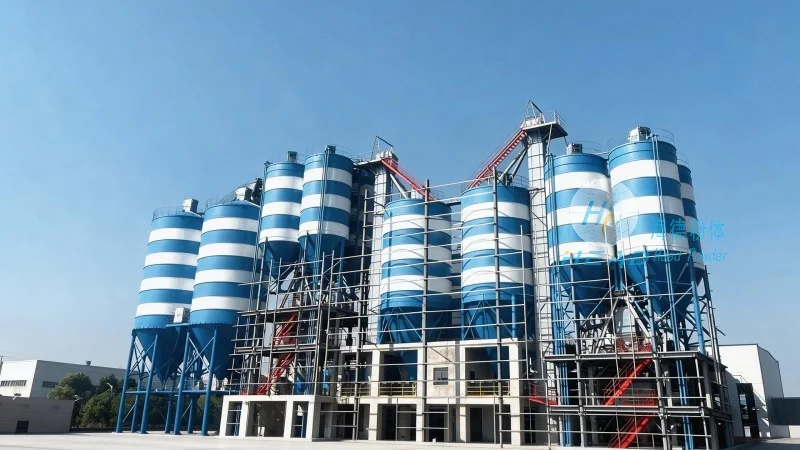
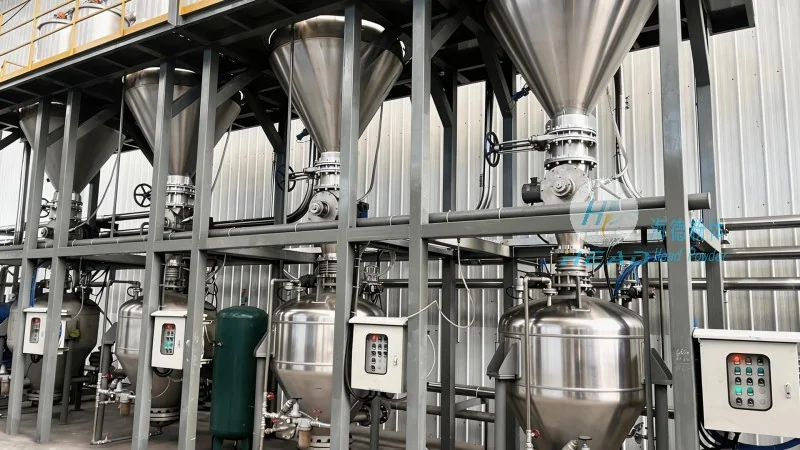
Potassium hydroxide powder conveying systems typically operate through a series of integrated components that work together to ensure efficient and safe transport. The process begins with the storage of KOH in a sealed silo or hopper, which is designed to maintain the material's quality by controlling moisture and preventing exposure to air. From the storage vessel, the powder is fed into a feeder, which regulates the flow rate and ensures a consistent supply to the conveyor. The conveyor itself is the central component of the system, with options including screw conveyors, belt conveyors, or pneumatic ducts. Screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle bulk materials without the need for external power beyond the motor driving the screw. These conveyors consist of a rotating helical screw inside a trough, which moves the powder forward by friction. Pneumatic conveyors, on the other hand, use compressed air to create a flow of the material through a pipeline, often with a combination of positive and negative pressure to control the direction and speed of the powder. The system may also include a series of valves and regulators to control the pressure and flow, ensuring that the KOH is transported at the desired rate. Additionally, the system includes safety features such as pressure relief valves, dust collection systems, and emergency shut-off mechanisms to protect against overpressure or material leakage, which is critical when handling a caustic chemical like KOH.
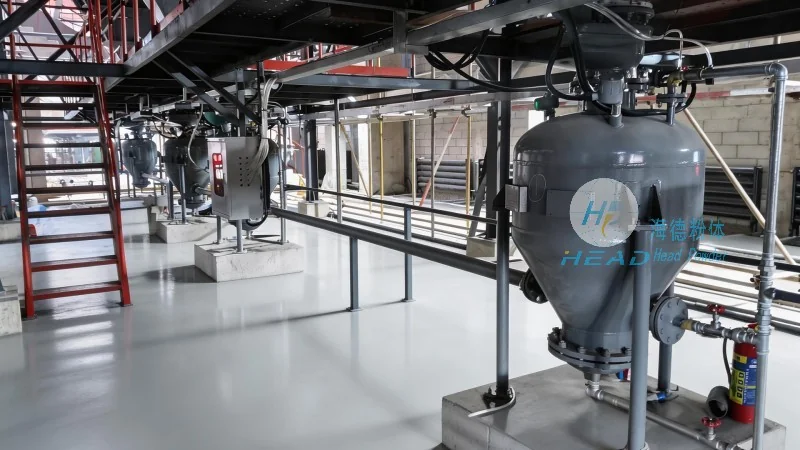
Key features of potassium hydroxide powder conveying systems are designed to address the unique challenges of handling this caustic material. One of the most important features is the use of corrosion-resistant materials, such as stainless steel or specialized alloys, to prevent degradation and ensure long-term durability. The systems are also equipped with effective sealing mechanisms to prevent dust and moisture from entering or escaping, which helps maintain the purity of the KOH and protects the environment and operators from exposure. Another critical feature is the ability to handle varying particle sizes and flow rates, which is achieved through adjustable feeders and variable speed drives. This flexibility allows the system to adapt to different production requirements, from small-scale laboratory applications to large-scale industrial processing. The systems also incorporate dust suppression and containment measures, such as cyclones and baghouses, to minimize the risk of airborne particles and ensure compliance with environmental regulations. Furthermore, modern conveying systems often include monitoring and automation capabilities, allowing for real-time tracking of material levels, flow rates, and system performance. This data-driven approach helps in optimizing operations, reducing downtime, and improving overall efficiency. The systems are also designed for easy maintenance and cleaning, with components that can be easily accessed and replaced, reducing the time and cost associated with upkeep.
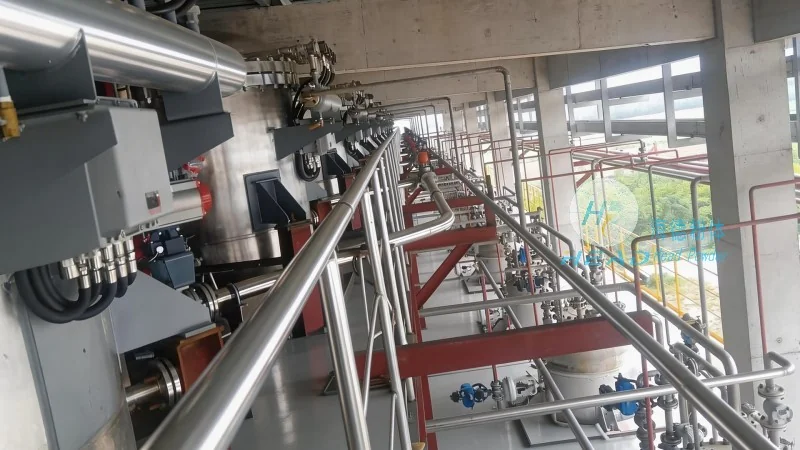
HeadPowder, the brand under Shandong HeadPowder Engineering Co., Ltd., is a trusted name in the field of powder handling equipment, specializing in the design and manufacturing of potassium hydroxide powder conveying systems. The company has a strong commitment to quality and innovation, with a team of experienced engineers and technicians who work closely with clients to understand their specific needs and provide tailored solutions. HeadPowder's systems are engineered to meet the highest standards of performance and safety, with features such as corrosion-resistant materials, effective sealing, and advanced automation capabilities. The company's facilities are equipped with state-of-the-art manufacturing and testing equipment, ensuring that each system is built to the highest quality standards. HeadPowder is dedicated to providing sustainable and efficient solutions for the chemical industry, with a focus on reducing environmental impact and improving operational efficiency. The company's products are widely used in various industries, including chemical manufacturing, pharmaceuticals, and food processing, where the safe and efficient handling of powders is critical. HeadPowder's reputation for reliability and customer satisfaction has made it a preferred choice for many clients, and the company continues to expand its product line and services to meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top