Crystal powder conveying equipment is a specialized device designed to handle and transport crystalline powders efficiently. This equipment is crucial in various industrial applications, such as pharmaceuticals, chemicals, and food processing, where precise handling of fine, fragile, or hygroscopic powders is essential. The design and operation of these systems are tailored to address the unique challenges posed by crystalline materials, ensuring reliable and consistent performance. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. (headpowder) has developed advanced crystal powder conveying equipment that meets the highest standards of efficiency and safety.
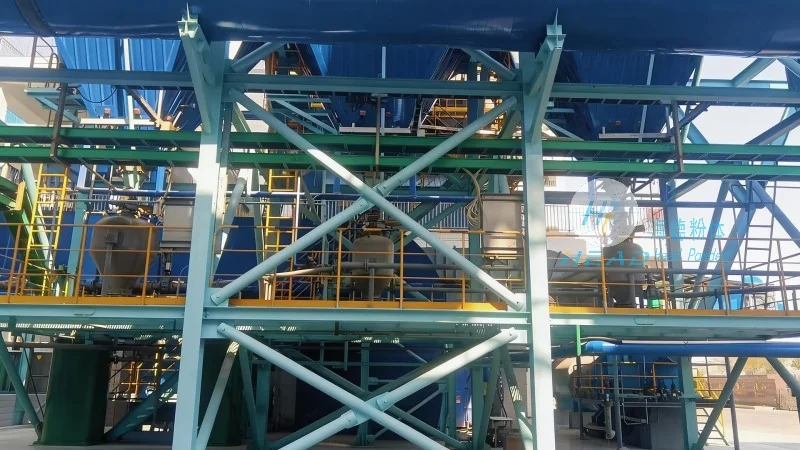
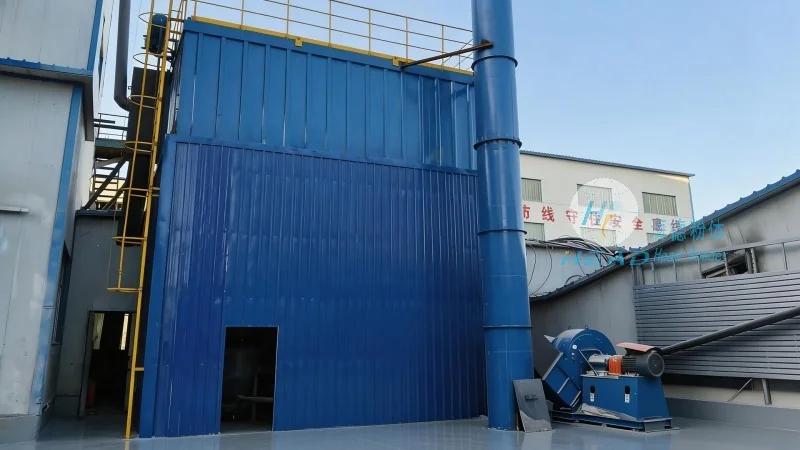
The working principle of crystal powder conveying equipment is centered on pneumatic conveying, which utilizes air as the medium to transport powders. There are primarily two types of pneumatic conveying systems: pressure and vacuum. Pressure systems use compressed air to push the powder through the pipeline, while vacuum systems use a vacuum to draw the powder into the line. For crystalline powders, pressure systems are more commonly used due to their ability to handle higher material loads and maintain consistent flow rates. The process begins with the crystalline powder being stored in a hopper. The feeder, often a rotary valve or a screw feeder, controls the flow rate of the powder into the conveying line. The compressed air is introduced at the inlet of the pipeline, creating a pressure differential that propels the powder particles forward. As the powder travels through the pipeline, it may encounter components such as bends, expansions, or special valves that help maintain the flow and prevent blockages. The conveying line is typically made of materials like stainless steel or polyethylene to prevent corrosion and ensure durability. The air and powder mixture is then separated at the discharge end using a cyclone separator or a filter. The cyclone separator uses centrifugal force to separate the powder from the air, collecting the powder in a receiving container. The separated air is then discharged or recirculated, depending on the system design. This separation process is crucial for maintaining the purity and quality of the crystalline material, as it prevents contamination from the air and ensures that the powder remains in its original state. The entire process is controlled by a system of valves, sensors, and a control panel, which allows operators to monitor and adjust the flow rate, pressure, and other parameters as needed. This level of control ensures that the equipment operates efficiently and safely, adapting to the specific requirements of the crystalline material being handled.
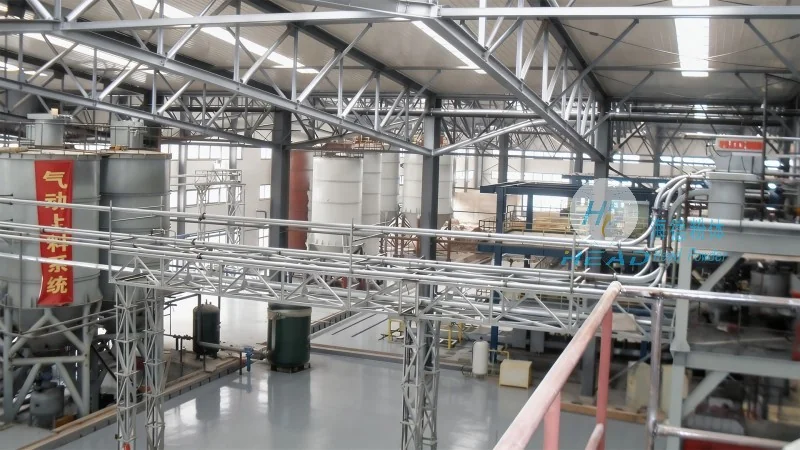
Crystal powder conveying equipment is characterized by several key features that enhance its performance and suitability for handling delicate crystalline materials. One of the primary features is its ability to handle fine powders without causing agglomeration or particle breakage. The equipment is designed with smooth, non-stick surfaces and gentle flow paths to minimize friction and impact on the powder particles. This is particularly important for hygroscopic or sensitive materials that can degrade if exposed to excessive pressure or friction. Another significant feature is the control over the conveying rate and pressure. Advanced models often include variable speed feeders and adjustable air flow controls, allowing operators to optimize the system for different powder types and application requirements. This flexibility ensures that the equipment can handle a wide range of crystalline materials, from low to high bulk density powders. The equipment also incorporates safety features to prevent dust explosions and ensure operator safety. Many systems include explosion-proof designs, dust collection systems, and pressure relief valves to mitigate risks associated with handling combustible or reactive powders. Additionally, the design of the conveying line and components is optimized for easy cleaning and maintenance, which is essential for maintaining hygiene standards in industries like pharmaceuticals and food processing. The use of stainless steel or other corrosion-resistant materials in the construction of the equipment further enhances its durability and suitability for harsh environments. These features collectively contribute to the reliability and efficiency of crystal powder conveying equipment, making it a preferred choice for industries that require precise and safe handling of crystalline powders.
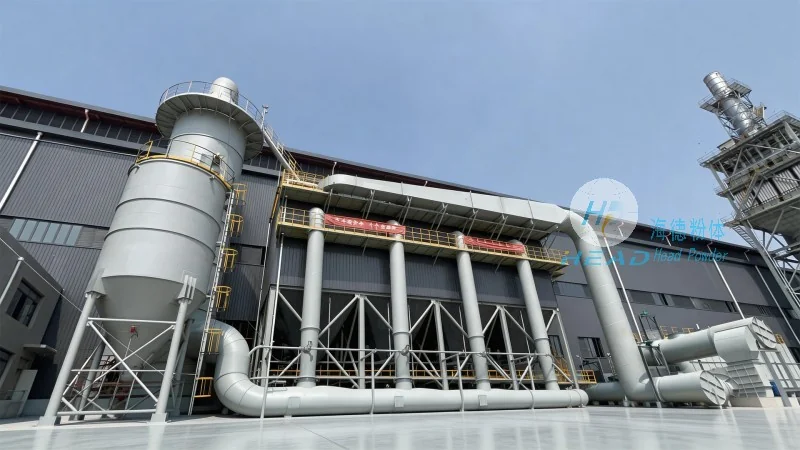
Crystal powder conveying equipment finds extensive applications across various industrial sectors, where the efficient and safe transport of crystalline materials is critical. In the pharmaceutical industry, these systems are used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the powders are transferred without contamination or degradation. The precise control over flow rates and pressure helps maintain the quality of the final drug products, which is paramount in pharmaceutical manufacturing. In the chemical industry, the equipment is utilized for transporting various chemical powders, including catalysts, pigments, and reagents. The ability to handle different bulk densities and particle sizes makes it versatile for diverse chemical processes. The food processing industry also benefits from these systems, particularly in the handling of food-grade powders like sugar, spices, and vitamins. The hygienic design and easy cleaning features of the equipment meet the stringent standards required in food processing facilities. The benefits of using crystal powder conveying equipment extend beyond just efficient transport. These systems reduce labor costs by automating the powder handling process, minimizing the need for manual handling which can be hazardous and inefficient. They also improve product quality by preventing segregation and contamination, which can affect the performance and safety of the final products. Furthermore, the energy efficiency of modern conveying systems helps reduce operational costs, making them a cost-effective solution for long-term use. The reliability of these systems ensures consistent performance, reducing downtime and maintenance costs associated with traditional manual or bulk handling methods. Overall, crystal powder conveying equipment offers significant advantages in terms of efficiency, safety, and product quality, making it an indispensable tool in industries that rely on the precise handling of crystalline powders.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top