Efficient and reliable conveying of purified powders and granules is crucial in various industrial applications, from pharmaceuticals to food processing and chemical manufacturing. The equipment designed for this purpose, often referred to as purified powder and granule conveying systems, plays a vital role in maintaining product integrity and operational efficiency. This article explores the working principles and key features of such equipment, highlighting how they contribute to safe and effective material handling.
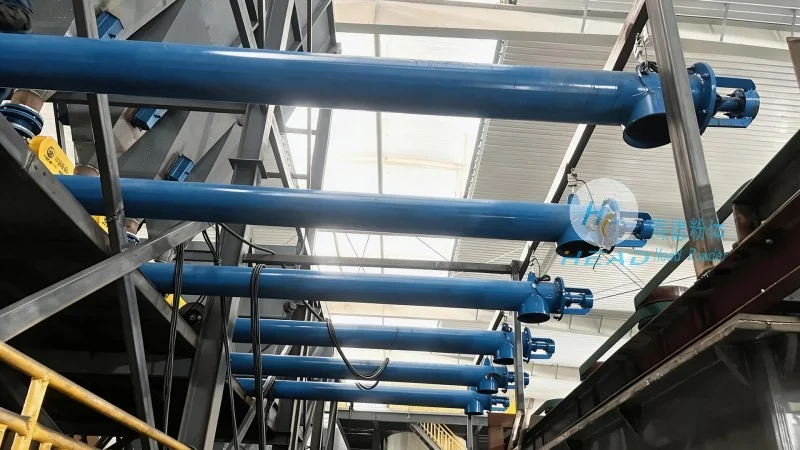
HeadPowder, a leading manufacturer in the field, specializes in the design, development, and production of advanced conveying solutions tailored to the needs of industries dealing with sensitive materials. With a strong foundation in engineering and a commitment to quality, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for businesses seeking reliable equipment for powder and granule handling. Based in Shandong, China, the company leverages local resources and global expertise to deliver innovative solutions that meet stringent industry standards.
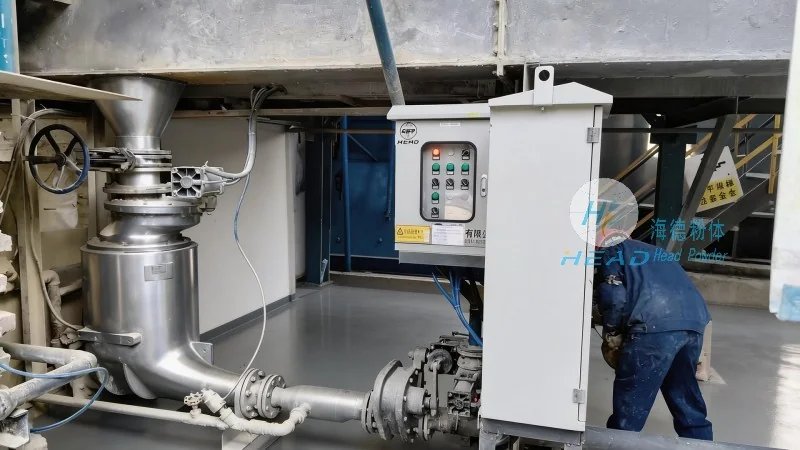
The core working principle of purified powder and granule conveying equipment revolves around the use of specialized mechanisms to transport dry materials without compromising their purity or quality. These systems typically employ a combination of positive displacement and pneumatic conveying technologies, depending on the specific requirements of the application. The process begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. From there, the material is propelled through the system using either air pressure (in pneumatic systems) or mechanical components (in positive displacement systems). The design of the equipment ensures that the material remains in a controlled environment, minimizing exposure to contaminants and maintaining its integrity throughout the conveying process.
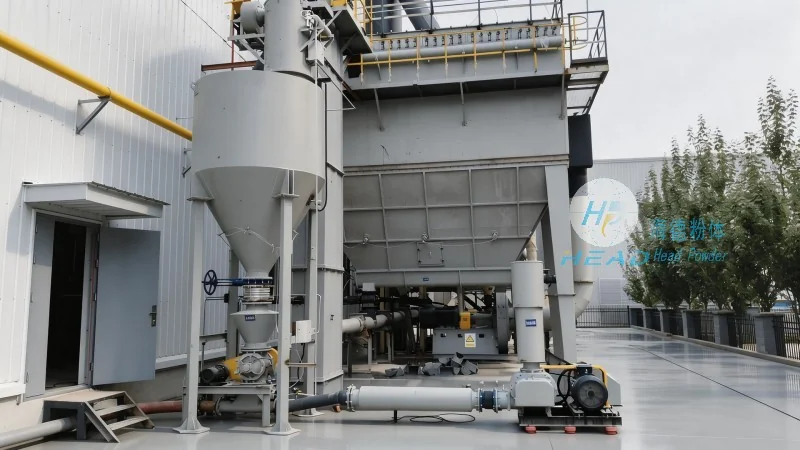
Several critical features distinguish high-quality purified powder and granule conveying equipment. First, the equipment is constructed from materials that are resistant to corrosion and compatible with the conveyed materials, ensuring long-term durability and minimal contamination risk. Second, advanced sealing systems are incorporated to prevent dust leakage and maintain a clean environment, which is essential for industries where product purity is paramount. Third, the design incorporates features that facilitate easy maintenance and cleaning, reducing downtime and operational costs. Fourth, the equipment is equipped with monitoring and control systems that allow for real-time adjustment of conveying parameters, ensuring optimal performance and preventing material blockages or other issues. Finally, the systems are designed to be energy-efficient, reducing operational costs while minimizing environmental impact.
When selecting a purified powder and granule conveying system, several factors must be considered to ensure optimal performance and suitability for the specific application. The first consideration is the type of material being conveyed, as different materials have different flow characteristics and may require specialized equipment. For example, materials with high moisture content or those that are prone to caking may require equipment with additional drying or anti-caking features. The second consideration is the required conveying capacity, as the system must be capable of handling the desired volume of material without compromising speed or efficiency. The third consideration is the distance over which the material needs to be conveyed, as this will affect the choice of conveying technology and system components. Finally, the environmental and regulatory requirements of the industry must be taken into account, as the equipment must comply with relevant standards and guidelines.
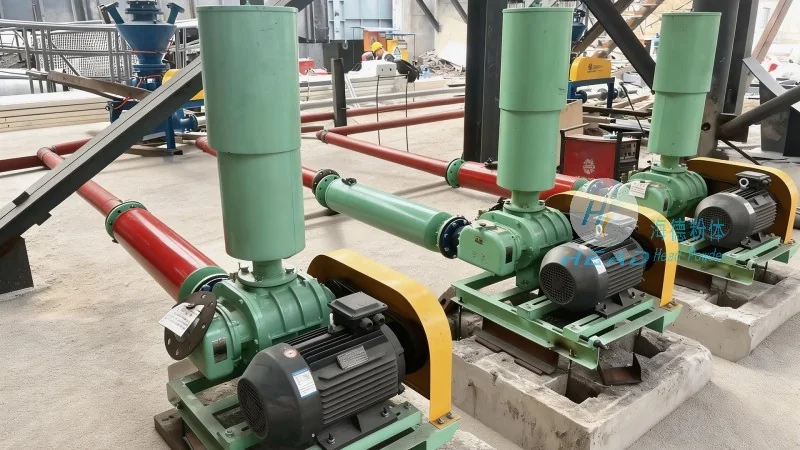
Proper maintenance and operational practices are essential to ensure the longevity and optimal performance of purified powder and granule conveying equipment. Regular inspection of the equipment is necessary to identify and address any potential issues before they become major problems. This includes checking for wear and tear on components, ensuring that seals are intact, and verifying that the conveying system is operating within the recommended parameters. Cleaning the equipment after each use is also important to prevent the buildup of material residues, which can affect performance and lead to contamination. Additionally, training operators on the proper use and maintenance of the equipment is crucial to ensure that they can operate it safely and efficiently. By following these best practices, businesses can maximize the lifespan of their equipment and minimize downtime, ultimately improving their overall operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top