Ammonium nitrate (AN) is a widely used industrial chemical, particularly in the production of fertilizers and explosives. The efficient and safe handling of AN powder is crucial for industrial operations. A specialized system, known as an ammonium nitrate powder conveying line, is designed to transport this fine powder from storage to processing or packaging areas. This article explores the working principle and key features of such a system, highlighting how it ensures optimal performance and safety in industrial applications.
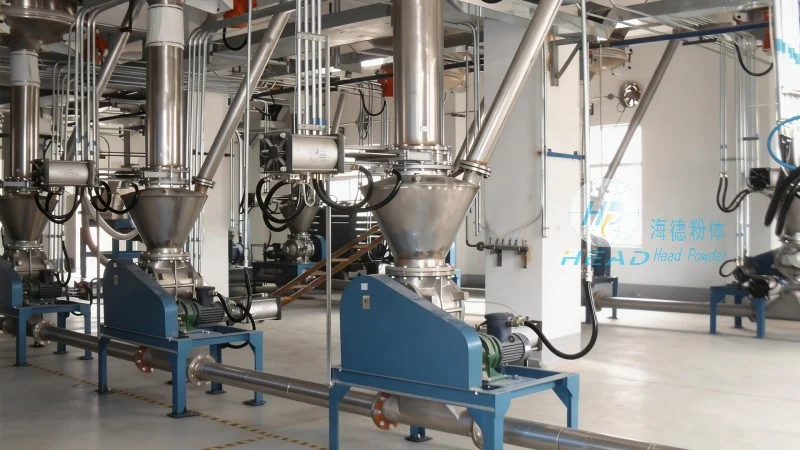
The working principle of an ammonium nitrate powder conveying line typically involves a combination of mechanical and pneumatic components. The process begins with the powder being stored in a silo or hopper. From there, the powder is fed into a feeder, which controls the flow rate to the conveying system. The feeder may be a rotary valve or a screw conveyor, depending on the system design. The powder is then introduced into a pipeline, where it is mixed with compressed air. The air-powder mixture travels through the pipeline under pressure, moving the powder to the destination point. The system may include a series of pipelines, with changes in direction and elevation managed by bends, elbows, and vertical risers. At the destination, the powder is separated from the air using a cyclone or a bag filter. The air is then discharged, while the powder is collected in a receiving hopper or directly to the processing equipment. The entire process is controlled by a programmable logic controller (PLC), which monitors and adjusts the flow rate, pressure, and other parameters to ensure smooth operation. This automated control system enhances efficiency and reduces the risk of human error. The working principle is designed to handle the unique properties of ammonium nitrate, such as its fine particle size and potential for dust explosion, by using appropriate materials and safety features.
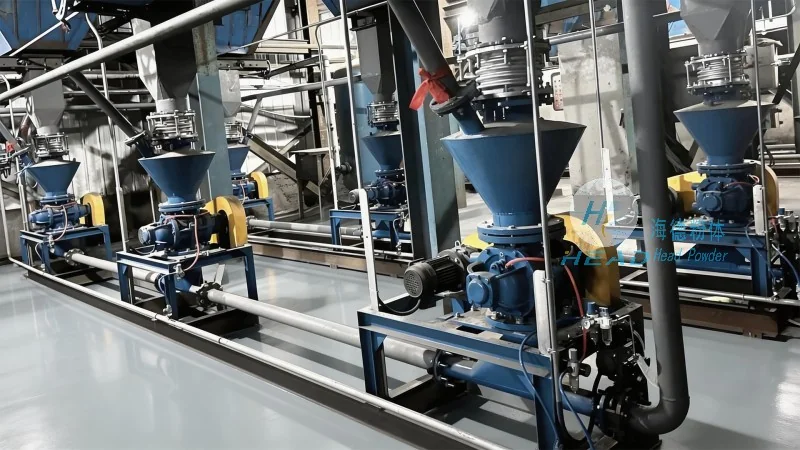
Key features of ammonium nitrate powder conveying lines include advanced safety measures, energy efficiency, durability, and ease of maintenance. Safety is paramount in handling AN, as it is a hazardous material that can cause dust explosions if not managed properly. The system incorporates explosion-proof motors, pressure relief valves, and flame arrestors to prevent and mitigate the risk of explosions. Additionally, the system is equipped with dust collection and ventilation systems to maintain a safe working environment. Energy efficiency is another critical feature, with the system designed to minimize energy consumption while maximizing throughput. This is achieved through optimized air flow rates, efficient motors, and the use of high-performance components. The system is constructed from durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the harsh conditions of AN handling. These materials are resistant to wear and corrosion, ensuring a long service life. The system is also designed for easy maintenance, with features like quick-release fittings, accessible internal components, and modular design. This allows for regular cleaning and maintenance, reducing downtime and extending the system's lifespan. Finally, the system complies with international standards and regulations, such as the European Union's ATEX directive and the U.S. Occupational Safety and Health Administration (OSHA) guidelines. These standards ensure that the system operates safely and meets the requirements for handling hazardous materials.
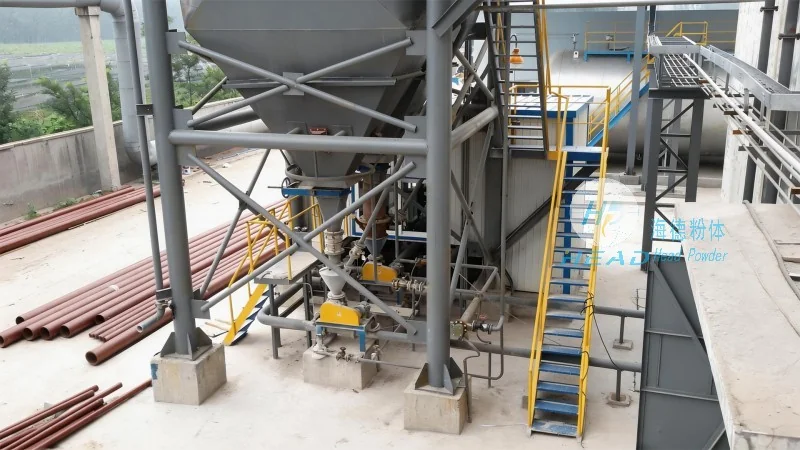
Shandong HeadPowder Engineering Co., Ltd., or HeadPowder, is a prominent manufacturer specializing in engineering solutions for powder handling. HeadPowder has built a reputation for delivering high-quality, reliable equipment tailored to the needs of industrial clients. The company's expertise spans the design, manufacturing, and installation of powder conveying systems, including those for ammonium nitrate. HeadPowder's team of engineers and technicians brings extensive experience in the field, ensuring that each system is optimized for performance and safety. The company's facilities in Shandong, China, are equipped with state-of-the-art technology and equipment, enabling the production of precision-engineered components. HeadPowder's commitment to quality is evident in its adherence to international standards, such as ISO 9001 for quality management systems. The company also prioritizes customer satisfaction, providing comprehensive support from initial consultation to post-installation maintenance. HeadPowder's products are widely used in industries such as fertilizer production, chemical processing, and food processing, where efficient and safe powder handling is essential. The company's dedication to innovation and customer service has established it as a leading provider in the powder handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top