

Working Principle and Characteristics of Dilute Phase Powder Pneumatic Conveying Systems
Dilute phase powder pneumatic conveying systems are advanced technologies used for the efficient transport of particulate materials through a gas stream. This method is widely adopted across various sectors, including pharmaceuticals, food processing, chemical manufacturing, and mining, due to its effectiveness in handling bulk materials. The system operates by suspending powder particles within a high-velocity air or gas flow, which then carries the material from the source to the destination. A thorough understanding of the working principle and key characteristics of such systems is crucial for selecting the appropriate equipment tailored to specific material handling requirements.
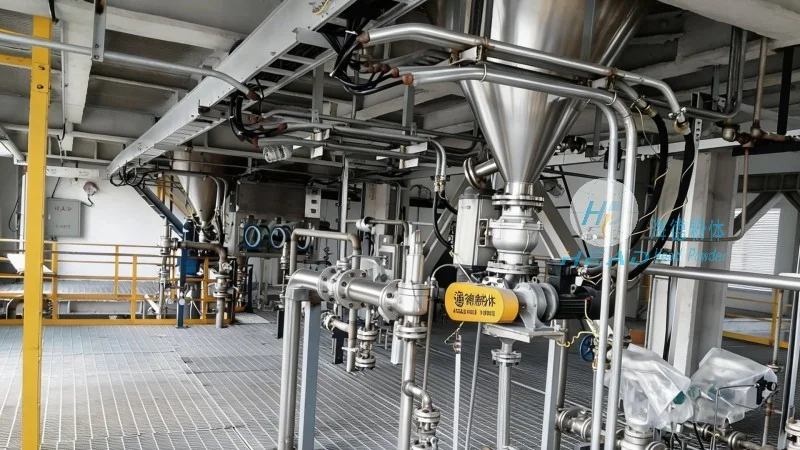
Working Principle of Dilute Phase Pneumatic Conveying Systems
The fundamental operation of dilute phase powder pneumatic conveying involves the creation of a particle suspension within a gas flow. In this process, the material is introduced into a pipeline where it is entrained by a high-velocity air or gas stream. The air velocity is typically maintained at a level that ensures the particles remain suspended, preventing settling or blockages. The system utilizes either pressure or vacuum to facilitate material movement through the pipeline. Pressure systems employ compressed air to push the material forward, while vacuum systems use suction to draw the material into the pipeline. Critical design elements include the type of air nozzles, pipeline diameter, and air velocity, all of which are essential for achieving efficient and reliable material transport. The working principle also encompasses the use of auxiliary equipment such as feeders, cyclones, and filters to control the flow and separate the material from the conveying air, ensuring smooth operation and product integrity.

Key Characteristics of Dilute Phase Powder Pneumatic Conveying Systems
Dilute phase systems are distinguished by several notable features that enhance their suitability for diverse applications. A primary characteristic is the low concentration of powder in the conveying air, typically ranging from 1 to 10 grams per cubic meter. This low concentration minimizes the risk of blockages and ensures consistent flow through the pipeline. Another key characteristic is the high velocity of the air stream, which is necessary to maintain particle suspension and overcome gravitational forces acting on the particles. The systems also offer flexibility in material handling, as they can transport a wide variety of powders, including fine, dry, and abrasive materials. Additionally, dilute phase systems excel in handling long distances and multiple discharge points, making them ideal for complex material handling processes. The design allows for easy integration with existing facilities and can be customized to meet specific operational needs, such as varying material types or flow rates.
Advantages and Applications in Industrial Settings
Dilute phase powder pneumatic conveying systems provide significant advantages over traditional material handling methods. One major benefit is the ability to transport materials in a closed system, which helps maintain product quality and prevent contamination, a critical factor in industries like pharmaceuticals and food processing. The systems also create a hygienic and dust-free environment, reducing the risk of product degradation and ensuring compliance with regulatory standards. Another advantage is the capability to handle materials that are difficult to transport using conventional methods, such as fine powders prone to caking or agglomeration. The systems are energy-efficient, utilizing less energy compared to other bulk material handling solutions, which contributes to cost savings and environmental sustainability. Furthermore, dilute phase systems can operate in both pressure and vacuum modes, providing flexibility in material transport. The ability to handle multiple discharge points and long distances makes them suitable for large-scale operations, such as in mining or chemical plants where material is transported over extensive distances or to multiple processing units.
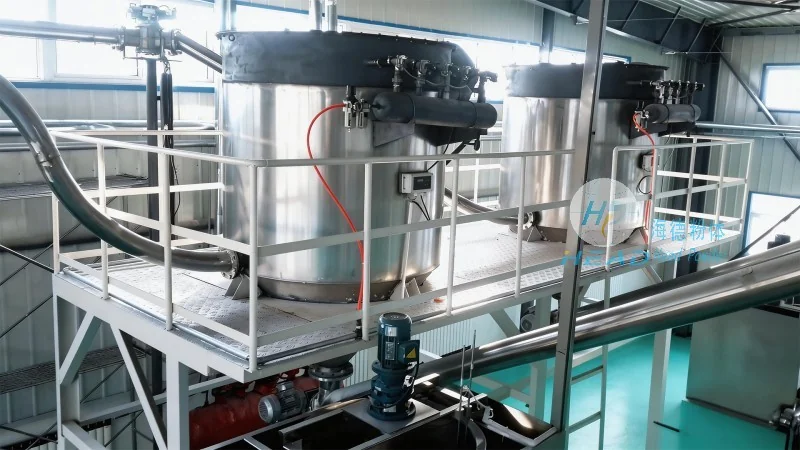
Introduction to Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a prominent provider of specialized powder handling solutions. The company focuses on the design, manufacturing, and installation of dilute phase powder pneumatic conveying systems and complementary equipment. With a commitment to innovation and quality, HeadPowder has established itself as a trusted partner in the industry. The company's products are engineered to meet the unique needs of various industries, ensuring efficient and reliable material transport. HeadPowder's team of experienced engineers and technicians offers comprehensive support, from initial system design and engineering to on-site installation and maintenance. The company's dedication to customer satisfaction and product excellence has earned it a strong reputation as a reliable supplier of advanced powder handling solutions. HeadPowder operates from its headquarters in Shandong, China, where the company leverages its local expertise and resources to deliver high-quality services and products to clients worldwide.