

Working Principle and Features of PFA Powder Pneumatic Conveying System
For industrial applications requiring the efficient and reliable transport of polytetrafluoroethylene (PFA) powder, pneumatic conveying systems offer a robust solution. This article explores the working principle and key characteristics of a PFA powder pneumatic conveying system, highlighting its design, operational mechanics, and advantages in material handling.
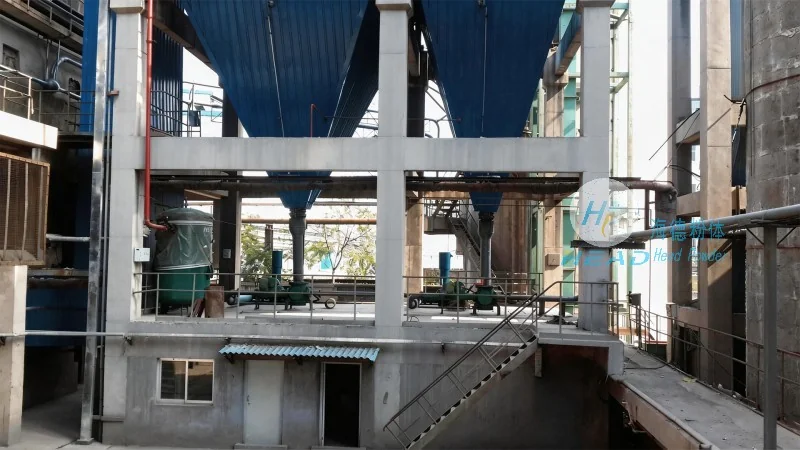
HeadPowder, a leading manufacturer based in Shandong, China, specializes in engineering advanced pneumatic conveying solutions tailored to the unique properties of PFA powder. The system’s design incorporates several critical components that work in tandem to ensure optimal performance and material integrity throughout the conveying process.
Working Principle of the PFA Powder Pneumatic Conveying System
The core mechanism of the PFA powder pneumatic conveying system relies on the principles of pneumatic transport, where air is used as the medium to move dry powder particles. The system typically operates on either positive or negative pressure, depending on the specific application requirements. In a positive pressure system, air is pressurized and forced through the conveying line, carrying the PFA powder from the source to the destination. Conversely, negative pressure systems draw air and powder through a vacuum, pulling material from the source into the system.
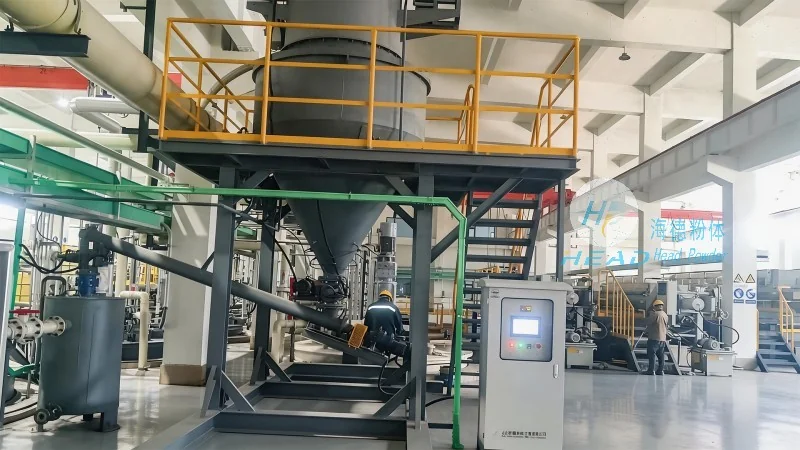
Key components in the system include a material feeder, which accurately meters the PFA powder into the conveying line, a venturi or eductor that accelerates the air-powder mixture, and a receiver or silo where the material is deposited. The material feeder ensures consistent flow rates, preventing overloading or underloading that could affect system efficiency. The venturi or eductor creates the necessary velocity to keep the PFA particles suspended in the air stream, preventing clogging and ensuring smooth transport. The receiver is designed to handle the deposited PFA powder, often with features like a discharge valve or hopper to facilitate downstream processing.
Key Features and Advantages of the PFA Powder Pneumatic Conveying System
Several distinct features make the PFA powder pneumatic conveying system particularly suitable for handling PFA material. Firstly, the system is designed to maintain the purity and integrity of the PFA powder, which is crucial for applications where contamination or degradation could impact product quality. The enclosed conveying line prevents exposure to external contaminants, such as moisture or dust, ensuring the material remains in its original state.
Secondly, the system offers high efficiency in terms of material transport. By using air as the conveying medium, the system can move PFA powder over long distances with minimal energy consumption compared to traditional mechanical conveying methods. This efficiency is further enhanced by the system’s ability to handle varying flow rates and particle sizes, making it adaptable to different production needs.
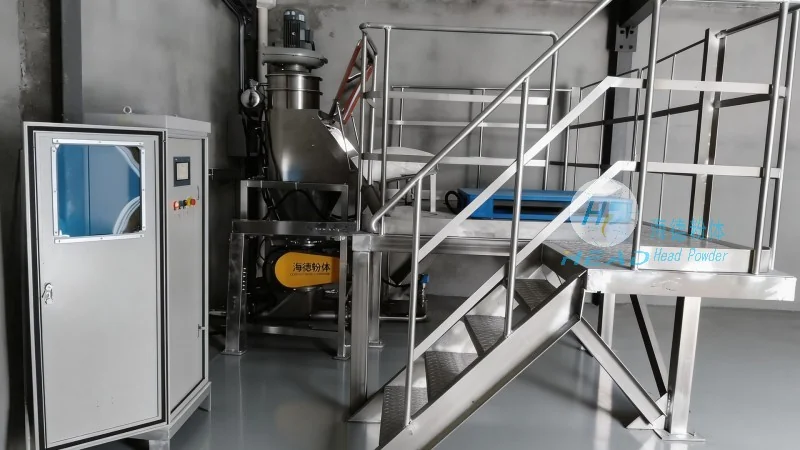
Thirdly, the system provides excellent control over the conveying process. The material feeder allows for precise control of the powder feed rate, while the venturi or eductor can adjust the air velocity to maintain optimal suspension of the PFA particles. This control ensures consistent material delivery to downstream processes, reducing variability and improving overall production quality.
Additionally, the PFA powder pneumatic conveying system is designed for easy maintenance and durability. The components are constructed from materials resistant to the chemical and thermal properties of PFA, ensuring long-term reliability. The system’s modular design allows for easy replacement of parts, reducing downtime and maintenance costs. Furthermore, the system is equipped with safety features, such as pressure relief valves and air filters, to prevent accidents and ensure safe operation.
Conclusion
HeadPowder’s PFA powder pneumatic conveying system combines advanced engineering with robust design to provide an efficient and reliable solution for transporting PFA powder. By leveraging pneumatic transport principles and incorporating key features like precise material control, high efficiency, and durability, the system meets the demanding requirements of industrial applications. Based in Shandong, China, HeadPowder continues to innovate in material handling technology, delivering solutions that enhance productivity and material quality for its clients.