

Working Principle and Features of Multi-functional Bulk Material Pneumatic Conveying Systems
Multi-functional bulk material pneumatic conveying systems represent a sophisticated technology designed to efficiently transport various types of bulk materials over long distances with minimal operational constraints. These systems are widely adopted in industries such as food processing, chemical manufacturing, and pharmaceuticals due to their ability to handle diverse materials while maintaining hygiene and efficiency. The core of these systems lies in the integration of pneumatic conveying principles with advanced control mechanisms, enabling seamless material transfer from source to destination.
Working Principle of the Pneumatic Conveying System
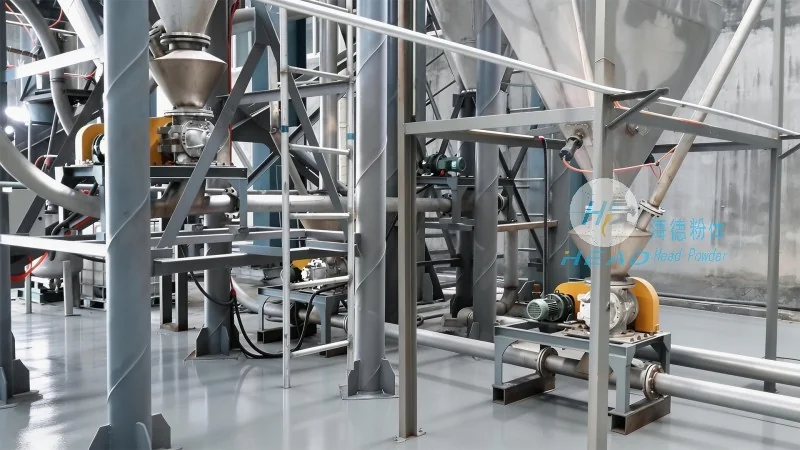
The operation of a multi-functional bulk material pneumatic conveying system is based on the fundamental principle of using air or gas as the conveying medium to transport solid particles. The system typically consists of a feeding hopper, a conveying line, a control valve, and a discharge outlet. The process begins when bulk material is fed into the hopper. An air compressor then generates a high-pressure air stream, which is introduced into the conveying line. As the air flows through the line, it entrains the material particles, forming a dense or dilute phase flow depending on the system design. The material is then transported to the discharge point, where the air is separated from the material, often through a cyclone separator or a filter. The separated air is then recycled back into the system, while the material is collected in a receiving container. This continuous cycle ensures efficient and reliable material transfer. The system's design allows for adjustments in air pressure and flow rate to accommodate different material characteristics, such as particle size, density, and moisture content. This adaptability makes the system suitable for a wide range of applications, from fine powders to coarse granules.
Key Features and Advantages of the System
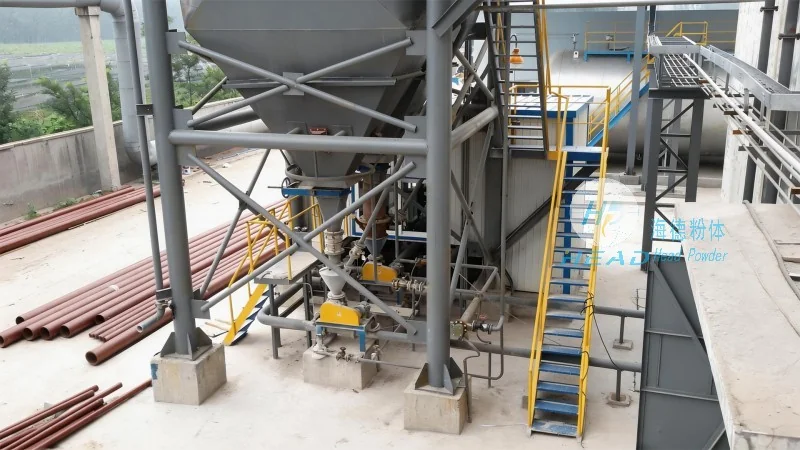
Multi-functional bulk material pneumatic conveying systems offer several distinct features and advantages that make them a preferred choice in modern industrial applications. Firstly, the system provides a hygienic and dust-free environment, which is crucial for industries dealing with food, pharmaceuticals, and other sensitive materials. The enclosed design prevents contamination and ensures compliance with regulatory standards. Secondly, the system offers high efficiency in material transport, with minimal material loss and low maintenance requirements. The use of air as the conveying medium reduces the need for mechanical components, such as belts or buckets, which can be prone to wear and tear. Thirdly, the system is highly flexible and can be easily integrated with existing production lines. It can be configured to handle multiple material types and can be scaled up or down to meet changing production demands. Additionally, the system provides real-time monitoring and control, allowing operators to adjust parameters such as air pressure and flow rate to optimize performance. This feature enhances operational efficiency and reduces downtime. Another key advantage is the system's ability to handle materials with varying properties, including abrasive or corrosive materials, without causing damage to the equipment. The robust construction and advanced materials used in the system ensure long-term durability and reliability.
Application Examples and Industry Impact
The versatility of multi-functional bulk material pneumatic conveying systems is evident in their widespread application across various industries. In the food industry, these systems are used to transport ingredients such as flour, sugar, and spices, ensuring a clean and efficient process. In the chemical industry, they handle chemicals and powders, maintaining safety and preventing contamination. The pharmaceutical industry also benefits from these systems, as they provide a sterile environment for transporting active ingredients and finished products. The system's ability to handle fine powders and granules makes it ideal for applications in the cement and construction sectors, where material transport is critical for production. The impact of these systems on industrial operations is significant, as they improve productivity, reduce labor costs, and enhance overall operational efficiency. By streamlining material transfer processes, these systems contribute to cost savings and increased profitability for businesses. The adaptability of the system to different material types and production scales also makes it a valuable asset for companies looking to expand or diversify their operations.

Conclusion and Company Overview
Multi-functional bulk material pneumatic conveying systems are a testament to modern engineering advancements, offering efficient, hygienic, and flexible solutions for material transport. The working principle, which relies on air as the conveying medium, combined with advanced control mechanisms, ensures reliable and consistent performance. The key features, including hygienic design, high efficiency, and adaptability, make these systems suitable for a wide range of industrial applications. As industries continue to evolve and demand higher standards of quality and efficiency, these systems remain a critical component in modern production processes. Shandong HeadPowder Engineering Co., Ltd., a leading provider of such systems, specializes in designing and manufacturing customized solutions tailored to the specific needs of clients. With a focus on innovation and quality, the company ensures that its products meet the highest industry standards and deliver long-term value to its customers. Based in Shandong, China, HeadPowder has established itself as a trusted partner in the field of pneumatic conveying technology, providing reliable and efficient solutions for bulk material transport across various industries.