

Working Principle and Characteristics of Mineral Particle Material Pneumatic Conveying Systems
For industrial operations dealing with mineral particle materials, efficient material handling is crucial. Pneumatic conveying systems offer a reliable solution to transport bulk materials over short to medium distances. This article explores the working principle and key characteristics of such systems, highlighting their applications and benefits in the mineral processing industry.
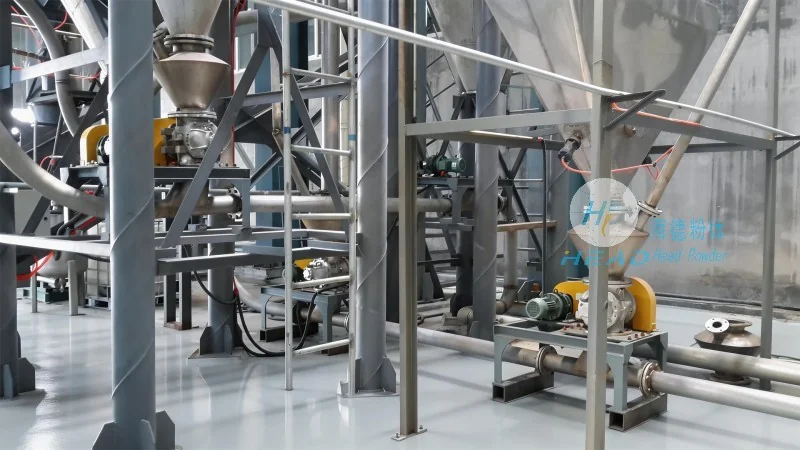
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider in the field, specializes in designing and manufacturing advanced pneumatic conveying solutions. With a strong presence in China, particularly in Shandong, the company leverages years of expertise to deliver customized systems tailored to the unique needs of mineral processing facilities. Their commitment to quality and innovation ensures that clients receive equipment that meets stringent operational requirements and enhances overall productivity.
Working Principle of Mineral Particle Material Pneumatic Conveying Systems
The core of a pneumatic conveying system is the use of air or gas to transport solid particles. The process typically involves a few key components: a material hopper, a conveying line, a fan or blower, and a discharge point. When the system is activated, air is drawn into the hopper, creating a low-pressure zone that draws the mineral particles into the conveying line. The air then carries the particles through the pipeline to the discharge point, where the material is released under controlled conditions. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing safety.
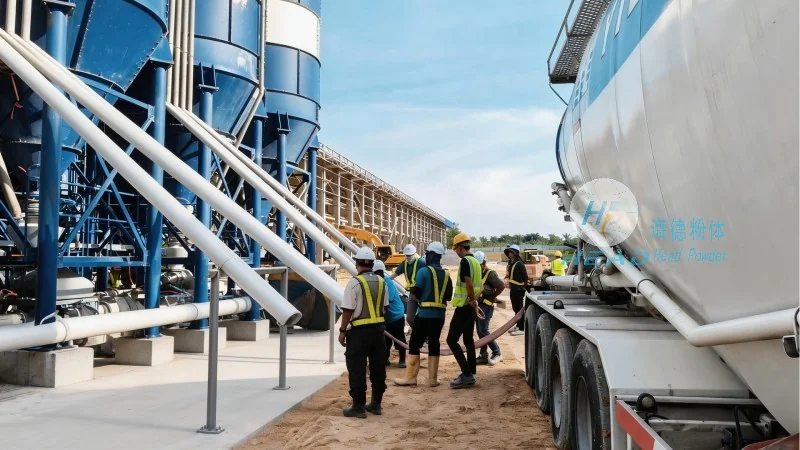
Key Characteristics and Advantages
Several distinct characteristics define pneumatic conveying systems for mineral particles. First, they provide a dust-free environment, which is essential for maintaining air quality and protecting equipment from corrosion. Second, the system can handle a wide range of particle sizes and densities, making it versatile for various mineral types. Third, it offers flexibility in layout, as the conveying line can be installed in different configurations to suit the plant layout. Additionally, pneumatic conveying systems are energy-efficient compared to traditional methods, as they use less power while achieving high material throughput. The ability to transport materials in a closed system also minimizes environmental impact and product contamination.
Applications in the Mineral Processing Industry
Pneumatic conveying systems are widely used in the mineral processing sector for tasks such as transporting raw ores, finished products, and by-products. In mining operations, they are employed to move crushed and screened minerals from storage bins to processing units. In processing plants, they facilitate the transfer of concentrates and tailings, ensuring smooth workflow and reducing downtime. The systems are also suitable for transporting fine powders, which are often sensitive to moisture and contamination, making the closed system design particularly advantageous.
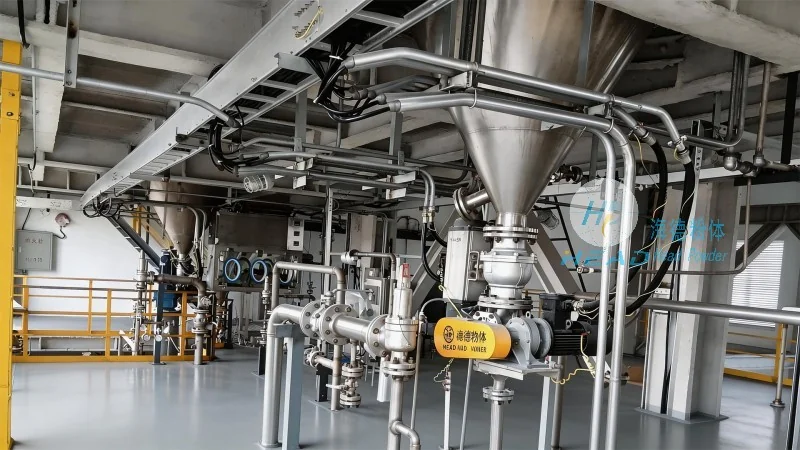
Customization and Integration with Existing Systems
HeadPowder understands that each mineral processing facility has unique operational requirements. Therefore, they offer customized pneumatic conveying solutions that integrate seamlessly with existing infrastructure. The company’s engineers work closely with clients to assess their material characteristics, flow rates, and plant layout to design a system that maximizes efficiency and minimizes operational costs. Whether it's a low-pressure or high-pressure system, or a dilute-phase or dense-phase design, HeadPowder can tailor the solution to meet specific needs. This approach ensures that the system not only meets current demands but also accommodates future expansion and technological advancements.
Conclusion and Contact Information
Pneumatic conveying systems represent a sophisticated and efficient method for handling mineral particle materials. With their ability to provide dust-free, flexible, and energy-efficient transport, they are increasingly becoming the preferred choice in the mineral processing industry. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in delivering these advanced systems, leveraging their expertise and commitment to quality to support clients in achieving their operational goals. For more information or to discuss your specific material handling needs, please contact HeadPowder at their location in Shandong, China.