

Working Principle and Characteristics of Biocatalyst Material Pneumatic Conveying Equipment
Biocatalyst material pneumatic conveying equipment is a specialized system designed for the efficient and safe transportation of biocatalyst materials, which are often sensitive and require precise handling. This equipment plays a crucial role in various industrial applications, particularly in the biochemical and pharmaceutical sectors, where the integrity and quality of the material must be preserved throughout the conveying process.
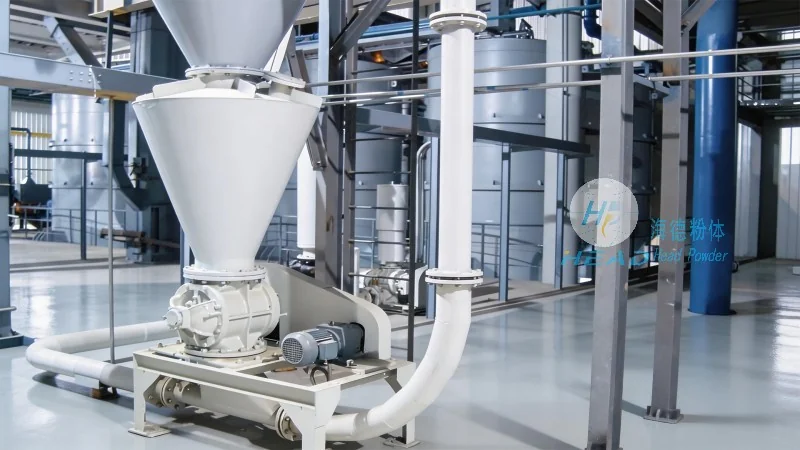
Working Principle of the Equipment
The core working principle of biocatalyst material pneumatic conveying equipment revolves around the use of compressed air to transport the material through a pipeline system. The process typically involves a hopper or feeding device that introduces the biocatalyst material into the system. As the material is fed, a fan or blower generates a flow of air, which creates a negative pressure or positive pressure environment within the pipeline. This airflow then lifts and transports the material particles through the ducts to the destination point, such as a storage tank, reactor, or processing unit. The design of the system ensures that the material is conveyed without direct contact with mechanical components, minimizing the risk of contamination or degradation.
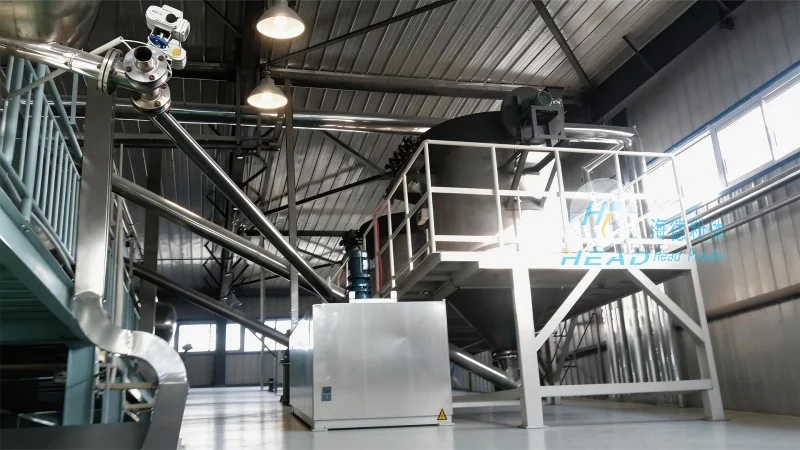
Key Characteristics and Advantages
Several key characteristics define the effectiveness and suitability of biocatalyst material pneumatic conveying equipment for industrial use. Firstly, the equipment is designed to handle sensitive materials, such as enzymes, which are often prone to degradation under high shear or mechanical stress. The pneumatic conveying method provides a gentle and controlled transport environment, reducing the risk of particle damage and maintaining the material's activity. Secondly, the system offers high efficiency in terms of material throughput, with the ability to convey large volumes of material over significant distances with minimal energy consumption compared to traditional mechanical conveyors. Thirdly, the equipment is highly flexible, allowing for easy integration into existing production lines and the ability to adjust the conveying rate based on operational needs. Additionally, the system is equipped with features like dust collection and filtration, ensuring that the material is handled in a clean and safe manner, which is critical for maintaining compliance with industry regulations and quality standards.
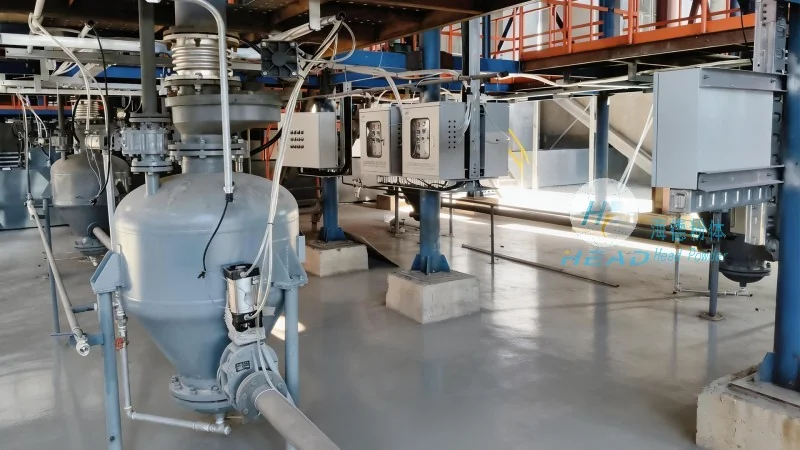
Company Information and Contact Details
For professional solutions in biocatalyst material handling, Shandong HeadPowder Engineering Co., Ltd. provides advanced pneumatic conveying equipment tailored to the specific needs of the biochemical and pharmaceutical industries. With a focus on innovation and quality, the company, commonly known as headpowder, offers systems that combine efficiency, reliability, and safety. HeadPowder's equipment is engineered to meet the stringent requirements of modern production processes, ensuring that biocatalyst materials are transported with the utmost care and precision. The company's headquarters is located in Shandong, China, where it continues to develop and refine its technology to support the evolving needs of the industry.