

Principles and Application Scenarios of Dry Powder Pneumatic Conveying
Dry powder pneumatic conveying is a widely used method for transporting bulk dry materials through a pipeline system using air as the conveying medium. This technology offers several advantages over traditional mechanical conveying methods, such as reduced equipment wear, lower maintenance costs, and the ability to handle materials that are difficult to transport by other means. The core principle involves creating a flow of air within a pipeline, which then lifts and transports the dry powder particles. By controlling the air velocity and pressure, operators can ensure efficient and reliable material transfer. This article explores the fundamental principles of dry powder pneumatic conveying and highlights key application scenarios where this technology excels.
Key Principles of Dry Powder Pneumatic Conveying
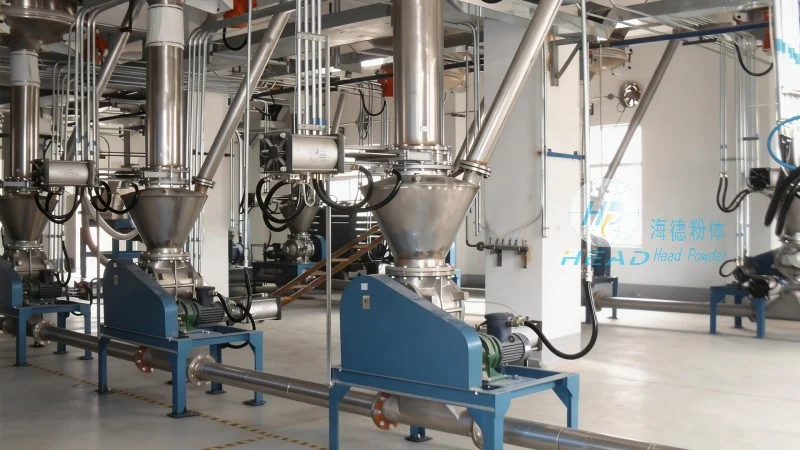
The operation of dry powder pneumatic conveying is based on the interaction between the dry powder particles and the air stream. When air is introduced into the pipeline at a sufficient velocity, it creates a drag force that overcomes the gravitational force acting on the powder particles. This allows the particles to be suspended in the air stream and transported to the destination. The process typically involves several components, including a feeding device, a conveying line, a separation unit, and a discharge mechanism. The feeding device ensures that the dry powder is introduced into the pipeline at a controlled rate, while the conveying line transports the mixture of air and powder. The separation unit, often a cyclone or filter, separates the powder from the air, allowing the air to be recycled or vented, and the powder to be collected for further use. The discharge mechanism then delivers the dry powder to the final storage or processing location.
Advantages of Dry Powder Pneumatic Conveying
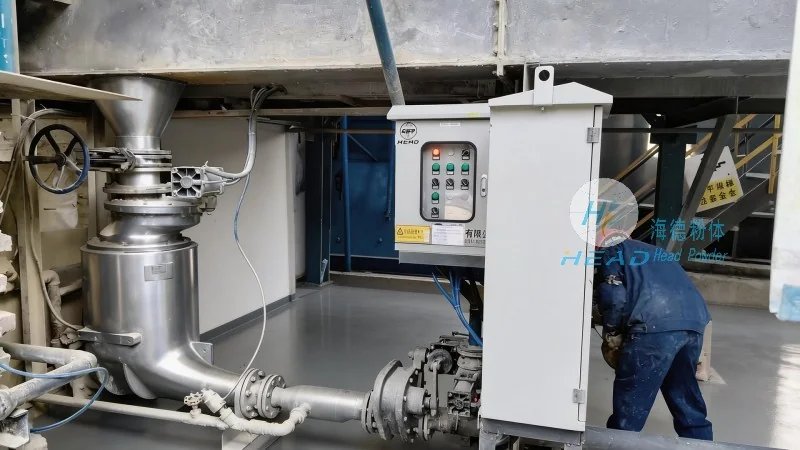
Compared to mechanical conveying systems, dry powder pneumatic conveying offers several benefits. One of the most significant advantages is the reduction in equipment wear and tear, as there are no moving parts in direct contact with the powder. This leads to lower maintenance costs and longer equipment lifespan. Additionally, pneumatic conveying systems can handle a wide range of materials, including fine powders, granules, and even abrasive substances, without causing damage to the material or the equipment. Another key advantage is the ability to transport materials over long distances with minimal loss or degradation. The enclosed pipeline system also helps to prevent dust emissions, improving workplace safety and environmental compliance. Furthermore, the flexibility of pneumatic conveying allows for easy integration with other processing equipment, such as mixers, classifiers, and storage silos.
Common Application Scenarios
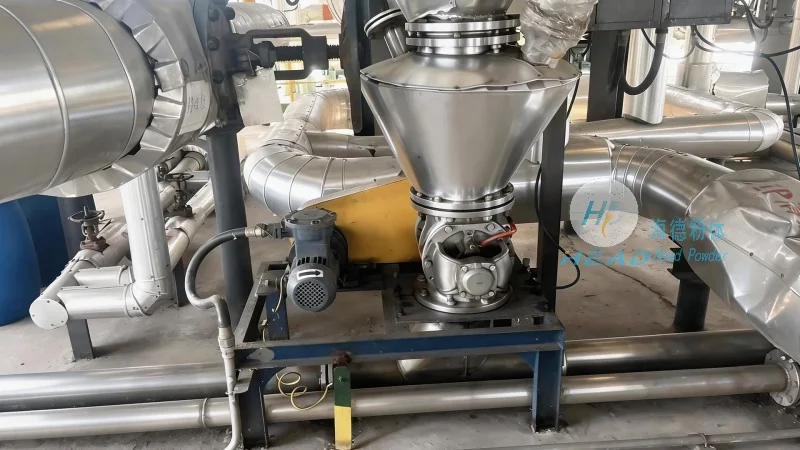
Dry powder pneumatic conveying is widely used in various industries due to its versatility and efficiency. In the pharmaceutical industry, for example, this technology is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. The enclosed system ensures that the materials remain sterile and free from external contaminants, which is critical for pharmaceutical production. In the food and beverage industry, pneumatic conveying is employed to transport dry ingredients like flour, sugar, and spices. The system maintains the quality and freshness of the ingredients while preventing cross-contamination between different products. The chemical industry also relies on dry powder pneumatic conveying for transporting various chemicals, including powders that are hazardous or reactive. The ability to handle these materials safely and efficiently is essential for industrial chemical processes. Additionally, in the mining and mineral processing sector, this technology is used to transport raw materials such as ores and minerals from processing plants to storage facilities or for further processing. The high capacity and reliability of pneumatic conveying make it suitable for large-scale material handling in these applications.
About HeadPowder: Shandong HeadPowder Engineering Co., Ltd.
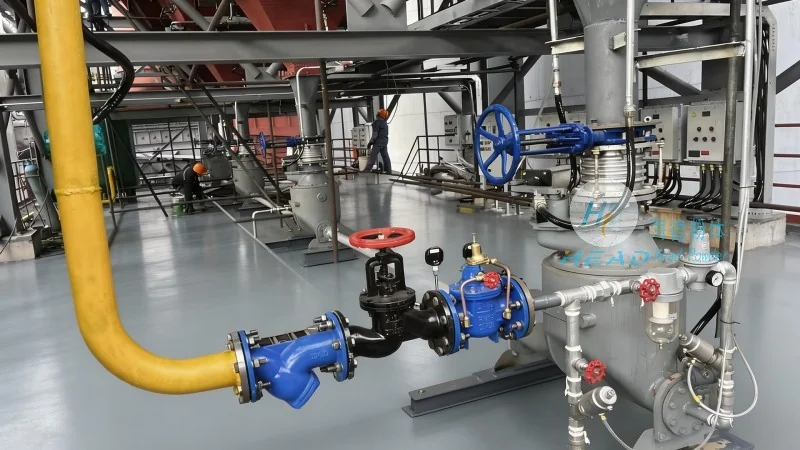
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of dry powder pneumatic conveying solutions. With headquarters in Shandong, China, the company specializes in designing, manufacturing, and installing customized pneumatic conveying systems tailored to the specific needs of its clients. HeadPowder's team of engineers and technicians leverages advanced technology and years of industry experience to develop efficient and reliable conveying systems that meet the highest standards of performance and safety. The company's products are widely used in pharmaceutical, food, chemical, and mining industries, among others. By focusing on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking to optimize their material handling processes. The company's commitment to quality and service ensures that clients receive not only state-of-the-art equipment but also comprehensive support throughout the entire project lifecycle, from initial consultation to installation and maintenance.