

Principles and Working Scene Characteristics of Cocoa Pneumatic Conveying
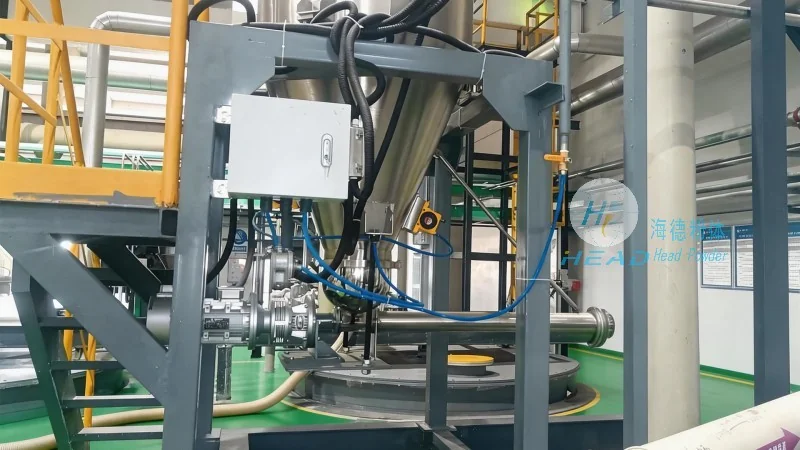
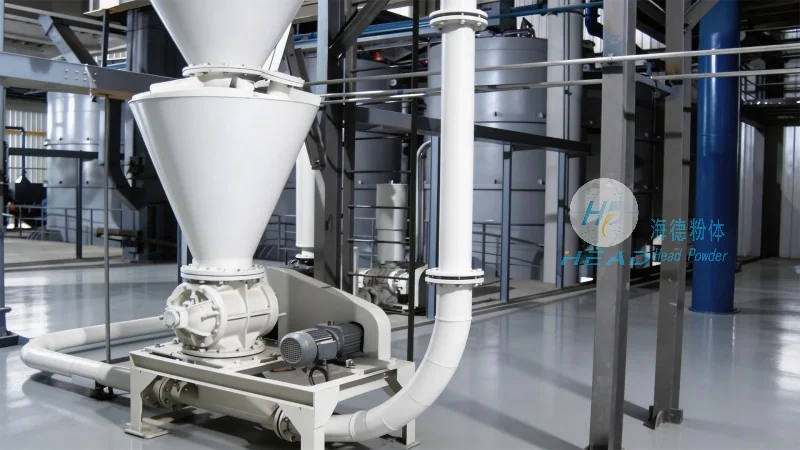
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of efficient pneumatic conveying systems for cocoa processing. The fundamental principle of cocoa pneumatic conveying involves the use of air to transport solid particles, such as cocoa beans or processed cocoa products, through a pipeline network. This method offers significant advantages over traditional mechanical conveying, including reduced contamination risk, lower maintenance requirements, and enhanced process flexibility. The core mechanism relies on creating a pressure differential within the system, typically by using a positive pressure blower or a vacuum pump, to move the material through the pipeline. The air velocity and pressure are carefully controlled to ensure the material is transported without degradation or loss.
Key Principles of Pneumatic Conveying for Cocoa
The pneumatic conveying of cocoa operates on several key principles that ensure effective and reliable material transport. First, the system must maintain a consistent air flow rate and pressure to prevent clogging or uneven distribution of the cocoa particles. The selection of appropriate air velocity is critical; too low a velocity may cause material settling or blockages, while too high a velocity can lead to excessive wear on the pipeline and equipment. HeadPowder engineers employ advanced computational fluid dynamics (CFD) and material flow analysis to optimize these parameters for each specific application. Second, the design of the pipeline system, including the use of bends, expansions, and filters, is crucial for maintaining the integrity of the cocoa product. Specialized filters and cleaning mechanisms are integrated to prevent dust accumulation and maintain product quality. Third, the system must be equipped with proper control and monitoring equipment to adjust air pressure and flow in real-time, ensuring stable operation under varying production conditions.
Working Scene Characteristics: Applications in Cocoa Processing
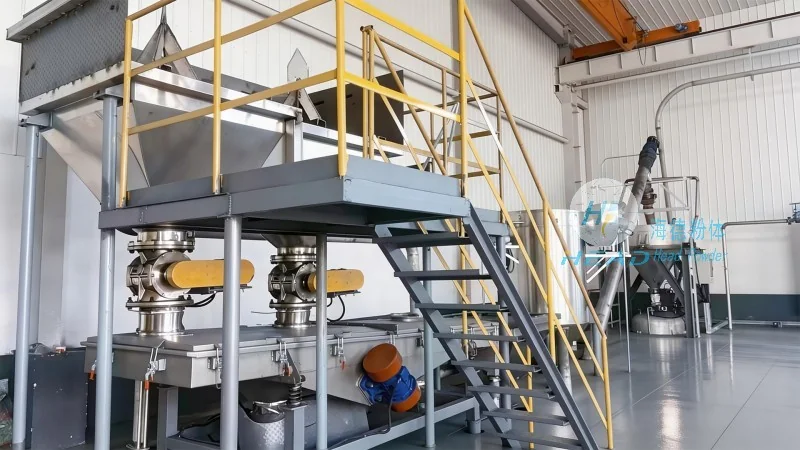
The working scene characteristics of cocoa pneumatic conveying systems are tailored to the specific needs of cocoa processing facilities. In raw cocoa processing, the system is used to transport cocoa beans from storage silos to roasting and grinding equipment. The positive pressure system is preferred in this stage due to its ability to handle high moisture content and prevent contamination from external sources. The pipeline network is designed with large-diameter pipes and gentle bends to accommodate the bulk volume of cocoa beans, minimizing the risk of material degradation. In the post-processing stage, such as cocoa powder or cocoa butter production, the system transitions to a more controlled environment. Here, the air velocity is reduced, and the pipeline diameter is adjusted to prevent the fine particles from being carried too quickly, which could lead to dust formation or equipment wear. The system may also incorporate cyclone separators and bagging stations to handle the final product. Additionally, in facilities that process different types of cocoa products simultaneously, the system is designed with multiple lines and isolation valves to prevent cross-contamination, ensuring each product maintains its unique characteristics.
HeadPowder's Expertise in Cocoa Pneumatic Conveying Solutions
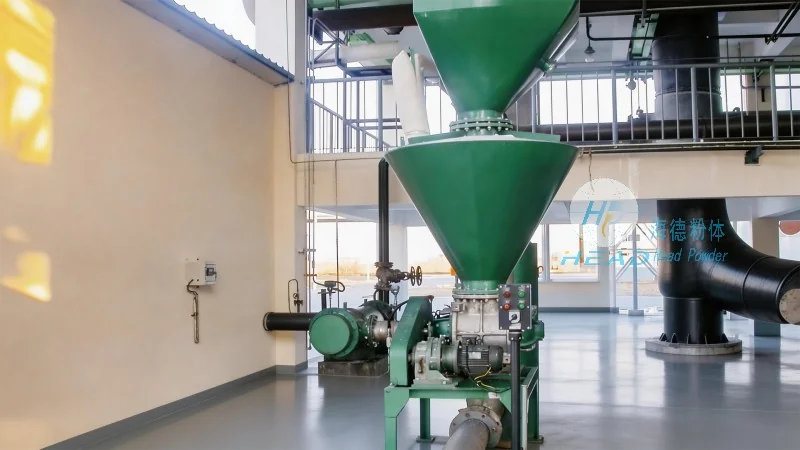
Shandong HeadPowder Engineering Co., Ltd. leverages decades of experience in the food processing industry to provide customized pneumatic conveying solutions for cocoa applications. The company's team of engineers works closely with clients to understand their specific production requirements, including capacity, material characteristics, and environmental regulations. By integrating advanced technology and robust design principles, HeadPowder ensures that each system is optimized for efficiency, reliability, and compliance. The company's solutions are built with high-quality materials, such as stainless steel and food-grade plastics, to meet stringent hygiene standards. Regular maintenance and support services are also provided to ensure the longevity and performance of the equipment. With a focus on customer satisfaction and product quality, HeadPowder has become a trusted partner for cocoa processing facilities worldwide.