

Principles and Application Scenarios of Dust-Free Automatic Pneumatic Conveying Systems
HeadPowder, a leading provider of industrial conveying solutions, specializes in dust-free automatic pneumatic conveying systems. These systems are engineered to transport bulk materials efficiently while maintaining stringent cleanliness standards, making them ideal for industries where contamination control is paramount.
Principles of Dust-Free Automatic Pneumatic Conveying Systems
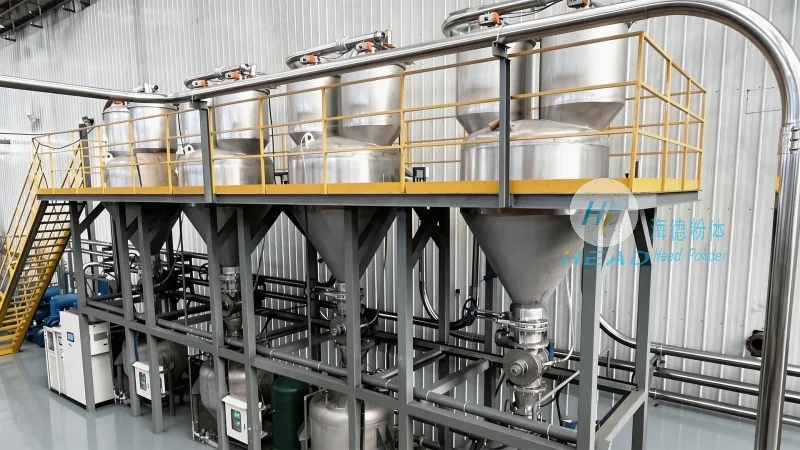
The core principle of pneumatic conveying involves using compressed air or gas to move materials through a pipeline. In a dust-free design, this process is enhanced with specialized components such as high-efficiency filters, sealed hoppers, and positive pressure or negative pressure systems to prevent dust leakage. The system typically comprises a material hopper, a conveying line, and a discharge unit, all integrated to ensure a continuous and clean material flow. The use of sealed containers and air-tight connections minimizes the risk of dust emission, aligning with industry standards for cleanroom environments.
Key Components and Their Functions
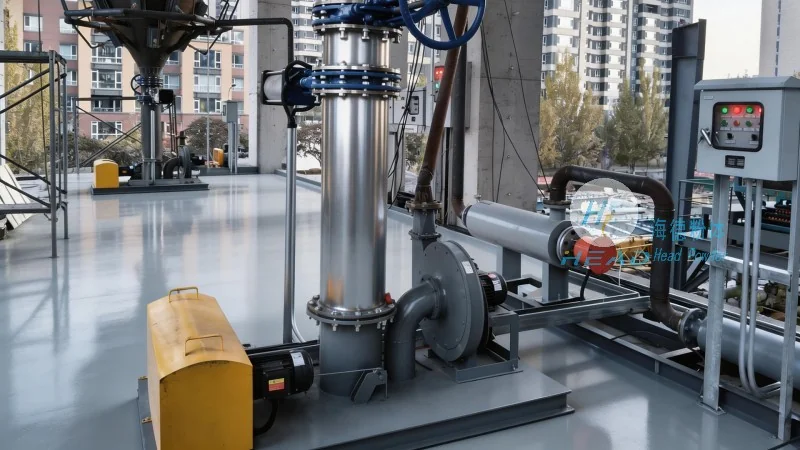
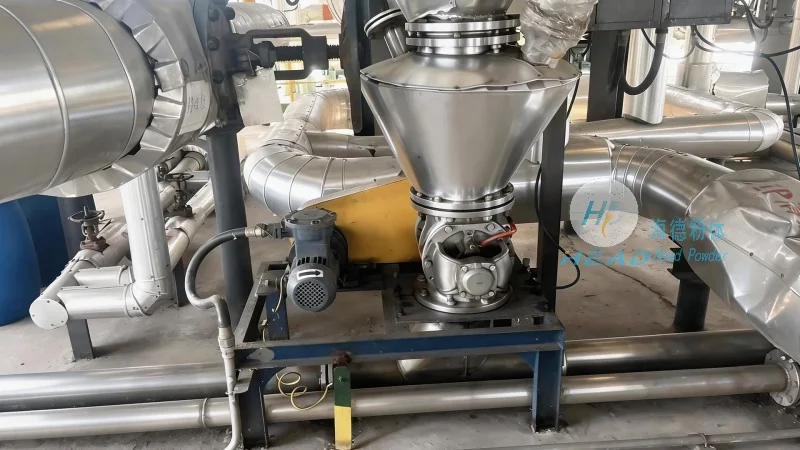
Several critical components contribute to the effective operation of a dust-free pneumatic conveying system. The material hopper is designed to store the bulk material and feed it into the conveying line under controlled conditions. A rotary valve or feeder ensures a consistent flow rate, preventing blockages or overfilling. The conveying line, often made of stainless steel or other corrosion-resistant materials, is equipped with pressure regulators and filters to maintain air quality and system pressure. At the discharge end, a cyclone separator or filter system captures any residual particles, ensuring that the material is delivered in a clean state. The control panel allows operators to monitor and adjust system parameters, such as air pressure and flow rate, to optimize performance and maintain dust-free conditions.
Application Scenarios and Industry Use Cases
Dust-free automatic pneumatic conveying systems are widely adopted across various industries due to their ability to handle sensitive materials without contamination. In the pharmaceutical industry, these systems are essential for transporting raw materials and finished products in sterile environments, where even trace dust can compromise product quality and safety. The food and beverage sector also relies on such systems to maintain hygiene standards, as they can handle powders and granules without cross-contamination. Additionally, in the chemical and petrochemical industries, these systems are used to transport hazardous or reactive materials safely, reducing the risk of exposure and environmental contamination. Each application scenario is tailored to meet specific industry requirements, ensuring that the system operates efficiently while adhering to regulatory standards.
Advantages of Implementing Dust-Free Pneumatic Conveying
Adopting a dust-free automatic pneumatic conveying system offers numerous benefits for industrial operations. Firstly, it significantly reduces operational costs by minimizing material loss and the need for frequent cleaning. The sealed design also lowers maintenance requirements, as there are fewer components exposed to dust and debris. Additionally, these systems enhance workplace safety by eliminating the need for manual handling of powders, which can cause respiratory issues or other health hazards. From an environmental perspective, the reduced dust emissions contribute to a cleaner working environment and compliance with environmental regulations. The efficiency of pneumatic conveying, with its ability to transport materials over long distances without the need for mechanical components, further improves overall productivity and operational flexibility.
Customization and Integration with Existing Facilities
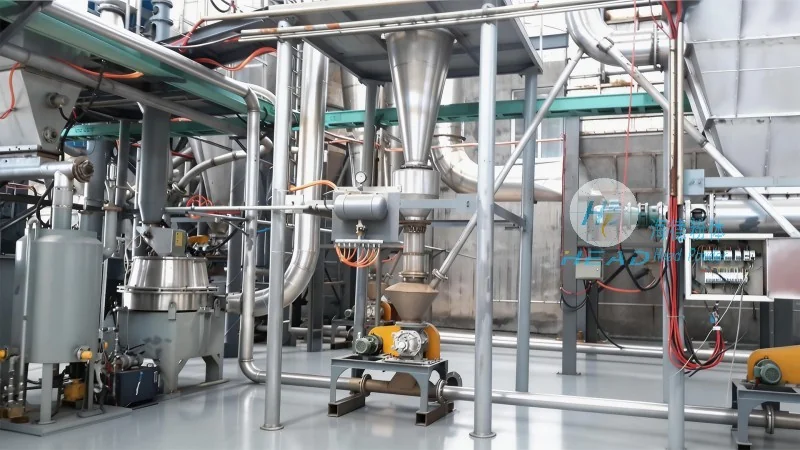
HeadPowder understands that each industrial facility has unique requirements, and therefore, offers customized solutions for dust-free pneumatic conveying systems. The company works closely with clients to assess their material handling needs, facility layout, and operational constraints to design a system that fits seamlessly into existing infrastructure. Customization may include adjusting the conveying line length, modifying the hopper size, or integrating additional filtration systems to meet specific industry standards. The ability to integrate with existing equipment, such as silos or storage tanks, ensures minimal disruption to current operations during installation. This approach not only enhances the system's performance but also maximizes the return on investment by leveraging existing assets. HeadPowder's expertise in engineering and manufacturing ensures that each customized system is built to withstand the demands of industrial environments, providing long-term reliability and efficiency.
Maintenance and Longevity of the System
Proper maintenance is crucial for the longevity and optimal performance of a dust-free pneumatic conveying system. Regular inspections of components such as filters, seals, and valves are essential to identify and address potential issues before they escalate. The use of high-quality materials, including stainless steel and advanced filtration media, contributes to the system's durability and resistance to corrosion. HeadPowder provides comprehensive maintenance services, including scheduled inspections, component replacements, and troubleshooting support, to ensure that the system operates at peak efficiency. By adhering to a regular maintenance schedule, industrial facilities can extend the lifespan of their conveying systems, reduce downtime, and maintain consistent material quality. The company's commitment to quality and customer support ensures that clients receive timely assistance and guidance throughout the system's lifecycle, enhancing overall operational reliability.
Conclusion: The Role of Dust-Free Pneumatic Conveying in Modern Manufacturing
In conclusion, dust-free automatic pneumatic conveying systems represent a sophisticated solution for efficient and clean material handling in various industries. By leveraging the principles of pneumatic transport and incorporating advanced sealing and filtration technologies, these systems address the critical need for contamination control while maintaining high operational efficiency. The applications span multiple sectors, from pharmaceuticals to food processing, where maintaining product purity and safety is non-negotiable. The advantages of reduced costs, enhanced safety, and environmental compliance make these systems a valuable investment for industrial facilities seeking to optimize their material handling processes. As industries continue to evolve and place greater emphasis on quality and sustainability, the role of dust-free pneumatic conveying systems will only become more prominent in modern manufacturing. HeadPowder remains at the forefront of this technology, providing tailored solutions that meet the diverse needs of its clients and contribute to the advancement of industrial efficiency and cleanliness standards.