

Principles and Working Scene Characteristics of Peanut Powder Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced powder handling solutions tailored for industries dealing with peanut powders. This article explores the fundamental principles behind peanut powder conveying equipment and highlights key working scene characteristics that define its application in various industrial settings.
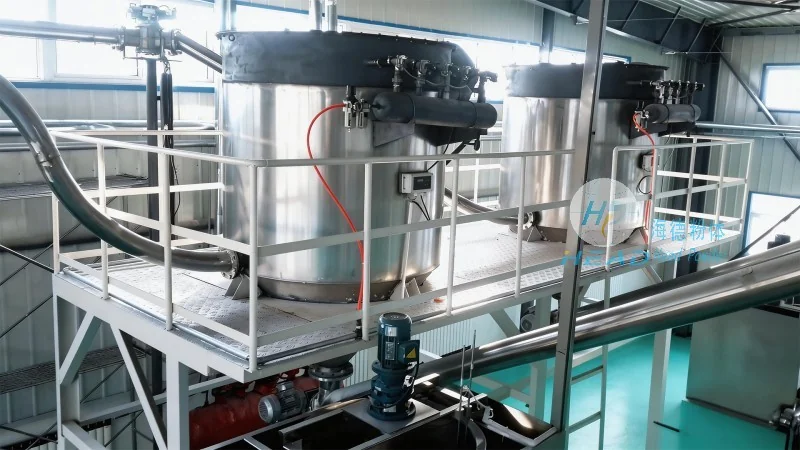
The Working Principle of Peanut Powder Conveying Equipment
Peanut powder conveying equipment operates on the principle of utilizing air or mechanical forces to transport fine powder materials like peanut flour or peanut meal. The core mechanism involves a combination of air flow dynamics and material handling components designed to ensure efficient and reliable movement of the powder. Key components include the hopper, which collects the peanut powder, the conveyor system (such as pneumatic or mechanical conveyors), and the control unit that regulates the flow. The equipment is engineered to handle the unique properties of peanut powder, such as its fine particle size and potential for static accumulation, ensuring stable and consistent conveying performance.
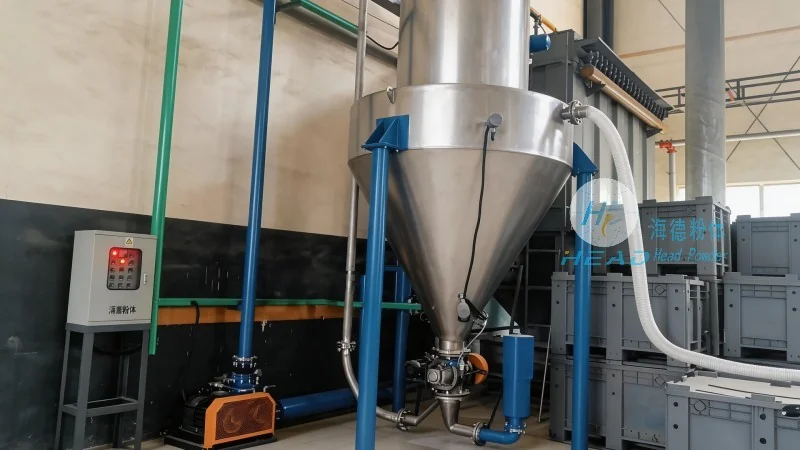
Key Working Scene Characteristics of Peanut Powder Conveying Equipment
The application of peanut powder conveying equipment is defined by several critical characteristics that address the specific demands of peanut processing industries. Firstly, the equipment is designed for high efficiency in material transfer, minimizing downtime and maximizing production throughput. Secondly, it ensures hygienic handling, which is essential for food-grade applications, as peanut powders are often used in food manufacturing. The equipment’s modular design allows for easy integration into existing production lines, adapting to different processing scales from small-scale batch operations to large-scale continuous production. Additionally, the system’s ability to handle varying powder densities and moisture content makes it versatile for diverse peanut processing scenarios, from raw material transport to finished product packaging.
Application Scenarios and Operational Advantages
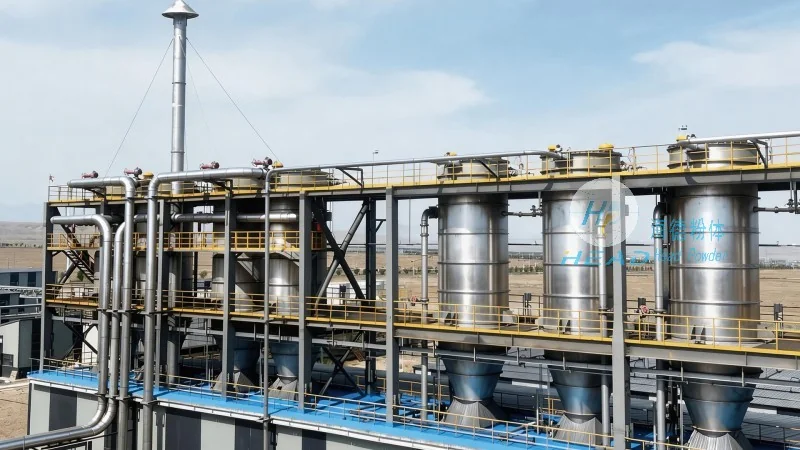
Peanut powder conveying equipment is widely used in scenarios ranging from raw peanut processing facilities to food processing plants. In raw material handling, the equipment efficiently transports ground peanuts from storage silos to processing lines, ensuring a continuous supply of powder for further production steps like roasting or flavoring. During the production of peanut-based food products, the conveying system maintains consistent material flow to mixers and extruders, preventing material buildup and ensuring uniform product quality. The equipment’s ability to handle fine powders without clogging or segregation is particularly valuable in maintaining product integrity. Furthermore, the system’s energy efficiency and low maintenance requirements contribute to long-term operational cost savings, making it a reliable choice for industrial peanut processing operations.
Conclusion
HeadPowder’s peanut powder conveying equipment exemplifies advanced engineering tailored to the unique challenges of handling peanut powders. By integrating principles of efficient material transport with robust design, the equipment ensures reliable performance across diverse working scenes. With a focus on hygiene, adaptability, and operational efficiency, this technology supports the seamless operation of peanut processing industries, from raw material handling to final product distribution. As a trusted manufacturer based in Shandong, China, HeadPowder continues to provide innovative solutions that meet the evolving needs of the peanut processing sector.