

Principle and Application Scenarios of Positive Pressure Dilute Phase Powder Conveying Systems
Positive pressure dilute phase powder conveying systems represent a sophisticated technology designed to transport bulk powders efficiently over long distances with minimal pressure loss. This method is particularly effective for handling materials that are prone to caking or require gentle handling, such as cement, flour, and various industrial powders. The core principle involves using compressed air to create a dilute suspension of the powder in the conveying line, ensuring smooth and continuous material movement.
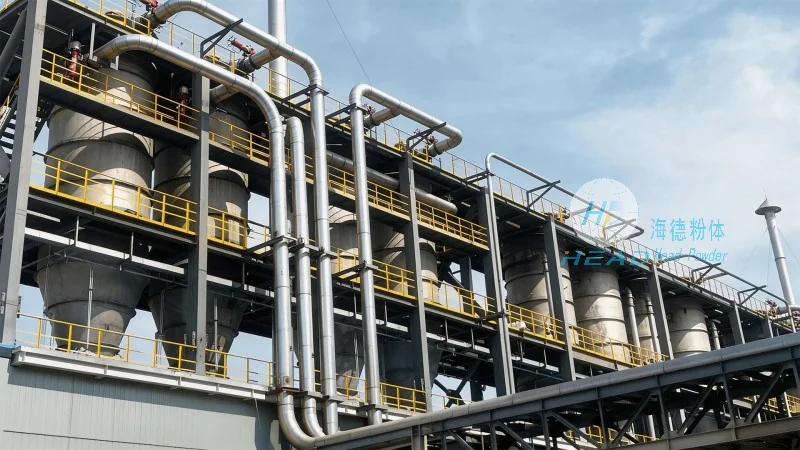
About HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of bulk material handling solutions, specializes in the design, manufacturing, and supply of advanced powder conveying equipment. With a strong presence in Shandong, China, the company leverages over 20 years of industry expertise to deliver reliable and efficient systems tailored to diverse industrial needs. The company's commitment to quality and innovation has positioned it as a trusted partner for businesses seeking to optimize their powder handling processes.
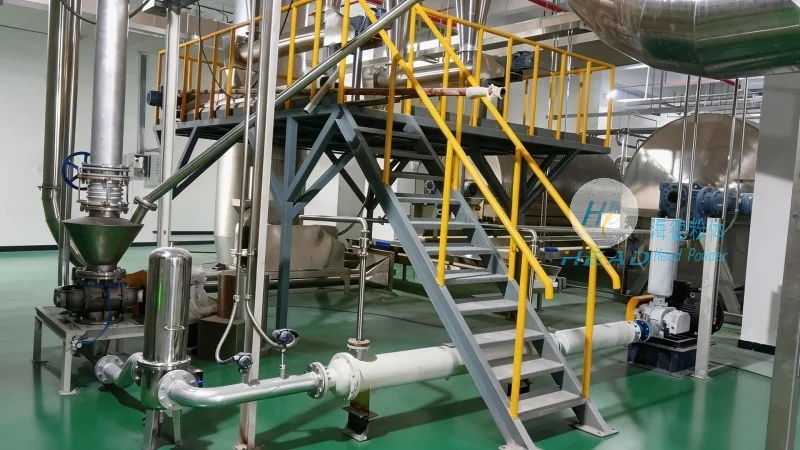
The Working Principle of Positive Pressure Dilute Phase Conveying
The positive pressure system operates by injecting compressed air into the material at the inlet of the conveying line. This air is then mixed with the powder to form a dilute suspension, which is propelled through the pipeline by the pressure differential. The key components include the air compressor, the material feeder, the conveying line, and the discharge equipment. The air pressure is typically maintained at a level sufficient to overcome the frictional losses in the pipeline and any elevation changes, ensuring the material is transported without clogging or degradation. This method is particularly advantageous for long-distance transport, as it minimizes the need for intermediate storage or transfer points, thus enhancing operational efficiency. The system's design allows for precise control of air and material flow rates, enabling operators to adjust the conveying speed according to the specific requirements of the material being handled. This flexibility is crucial for optimizing energy consumption and reducing operational costs.
Key Application Scenarios and Advantages
Positive pressure dilute phase conveying is widely used in various industrial sectors, including cement production, food processing, chemical manufacturing, and pharmaceuticals. Its advantages include high transport capacity, low material degradation, and the ability to handle a wide range of powder types. The system is also suitable for applications requiring gentle handling, such as sensitive pharmaceutical powders or food-grade materials, where caking or agglomeration must be avoided. Additionally, the positive pressure design ensures that the material is continuously in motion, reducing the risk of material buildup and associated maintenance issues. The flexibility of the system allows for easy integration into existing production lines, making it a cost-effective solution for businesses looking to upgrade their material handling capabilities. For example, in cement plants, this technology is used to transport raw materials and finished products over long distances, improving the overall production flow and reducing labor costs. In food processing facilities, it ensures that powders like flour or sugar are handled hygienically and efficiently, maintaining product quality and safety standards.
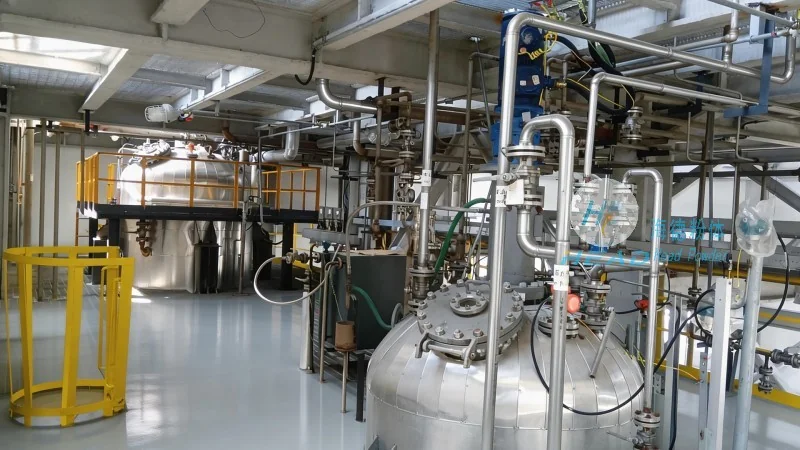
Customized Solutions for Diverse Industrial Needs
HeadPowder Engineering Co., Ltd. offers customized positive pressure dilute phase powder conveying systems tailored to the specific requirements of each client. The company's engineering team works closely with clients to understand their operational challenges and design solutions that maximize efficiency and minimize downtime. Whether it's for short or long-distance transport, high or low capacity requirements, HeadPowder provides comprehensive support from system design and installation to maintenance and after-sales service. The company's commitment to quality control ensures that all equipment meets international standards, providing clients with reliable and durable solutions that enhance their production processes. HeadPowder's expertise in material handling allows them to address unique challenges, such as handling abrasive powders or dealing with space constraints in existing facilities, by providing tailored solutions that meet both functional and regulatory requirements.