

Principle and Working Scene Characteristics of Catalyst Powder Conveying Machines
Catalyst powder conveying machines are critical equipment in industrial processes, particularly in sectors where catalysts are used for chemical reactions. These machines are designed to handle the transportation of catalyst powders efficiently and safely, ensuring that the material reaches its intended destination without degradation or loss. The technology behind these machines involves a combination of mechanical and pneumatic systems, tailored to meet the specific requirements of catalyst handling in various industrial applications.
The Working Principle of Catalyst Powder Conveying Machines
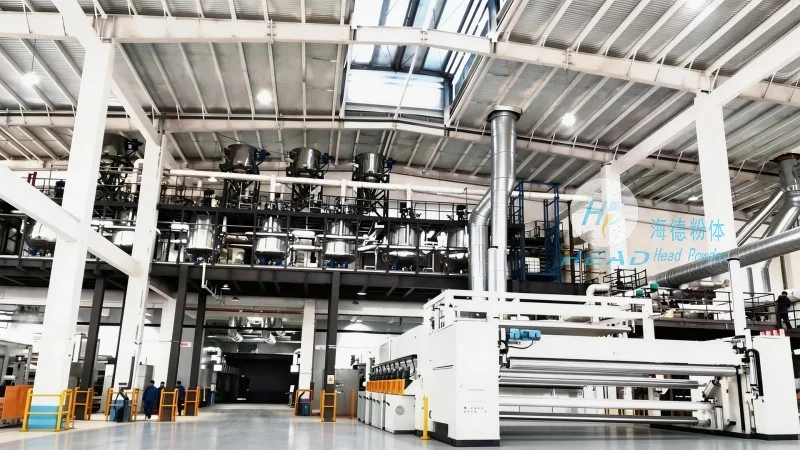
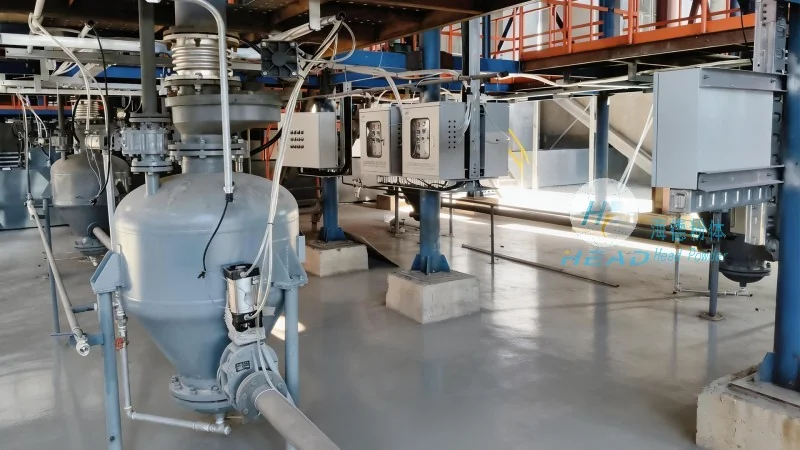
The core principle of catalyst powder conveying machines is the transfer of bulk powder materials through a system that combines air flow and mechanical components. The process typically begins with the loading of the catalyst powder into a hopper or feeder. From there, the powder is drawn into a pipeline by a fan or blower, which creates a pressure differential that propels the material forward. The design of the conveying system, including the type of ductwork, the size of the air nozzle, and the speed of the fan, is crucial for maintaining the flow rate and preventing clogging or particle degradation. In many systems, a rotary valve or a star feeder is used to control the flow of powder from the hopper into the pipeline, ensuring a consistent and controlled feed. The air flow is carefully regulated to maintain the powder in a suspended state, minimizing particle agglomeration and ensuring smooth transport. This principle is essential for maintaining the quality and effectiveness of the catalyst during transportation, as any degradation could impact the performance of the downstream processes.
Key Working Scene Characteristics of Catalyst Powder Conveying Machines
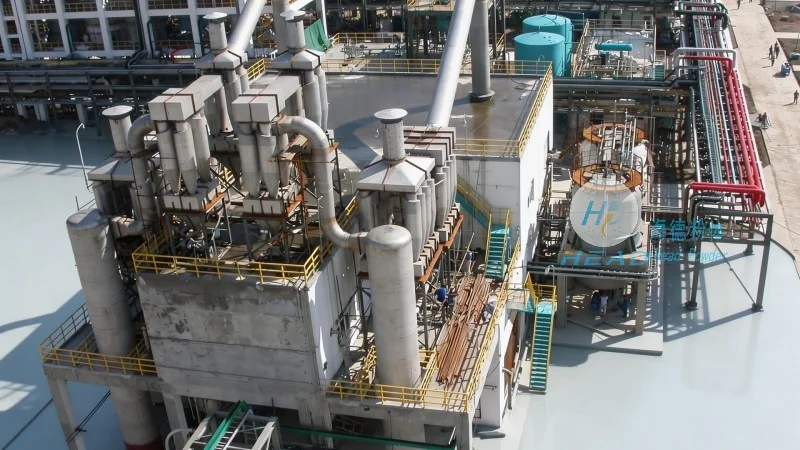
The working scene characteristics of catalyst powder conveying machines are tailored to the specific demands of industrial environments where catalysts are utilized. These characteristics include high efficiency in material handling, ensuring that large volumes of catalyst powder can be transported over significant distances with minimal energy consumption. The machines are designed for durability and reliability, as they operate in harsh industrial conditions where regular maintenance and downtime are costly. Another important characteristic is the ability to handle a wide range of particle sizes and densities, making them versatile for different types of catalysts. The systems are also equipped with safety features to prevent dust explosions, such as explosion-proof fans and proper grounding of the equipment. Additionally, the conveying machines are designed to minimize product contamination, which is critical in pharmaceutical and chemical industries where catalyst purity is paramount. The working scene also includes the integration of these machines with other process equipment, such as reactors and storage tanks, to form a seamless material flow system. This integration ensures that the catalyst is delivered to the reaction site in a timely and controlled manner, optimizing the overall production efficiency.
Application Scenarios and Operational Advantages
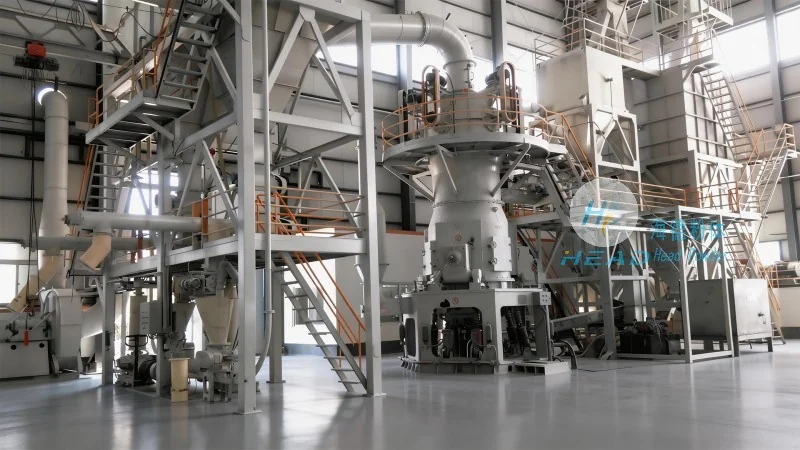
Catalyst powder conveying machines are widely used in various industrial applications, including chemical manufacturing, petrochemical processing, and pharmaceutical production. In chemical manufacturing, these machines are essential for transporting catalysts to reactors where they facilitate chemical reactions, such as in the production of plastics, fertilizers, and synthetic materials. The efficiency of the conveying system directly impacts the production rate and cost-effectiveness of the process. In petrochemical plants, catalysts are used in refining processes to improve the quality of fuels and other products. The conveying machines ensure that the catalysts are delivered to the reactors under controlled conditions, maintaining the optimal reaction environment. In pharmaceutical industries, the handling of catalyst powders requires strict adherence to hygiene and contamination control, which the design of these machines addresses through features like sealed systems and easy cleaning mechanisms. The operational advantages of catalyst powder conveying machines include reduced labor costs due to automated material handling, improved safety through enclosed systems, and enhanced product quality by minimizing exposure to air and moisture. These advantages make the machines a preferred choice for industries that require consistent and reliable transportation of catalyst powders.