

Principle and Working Scene Characteristics of Graphite Powder Conveying System Equipment
HeadPowder, a professional manufacturer based in Shandong, China, specializes in providing advanced solutions for graphite powder handling and transportation. The company's core product, the graphite powder conveying system, is designed to meet the demanding requirements of various industrial applications. This article explores the fundamental principles behind these systems and highlights the key characteristics of their operational environments.
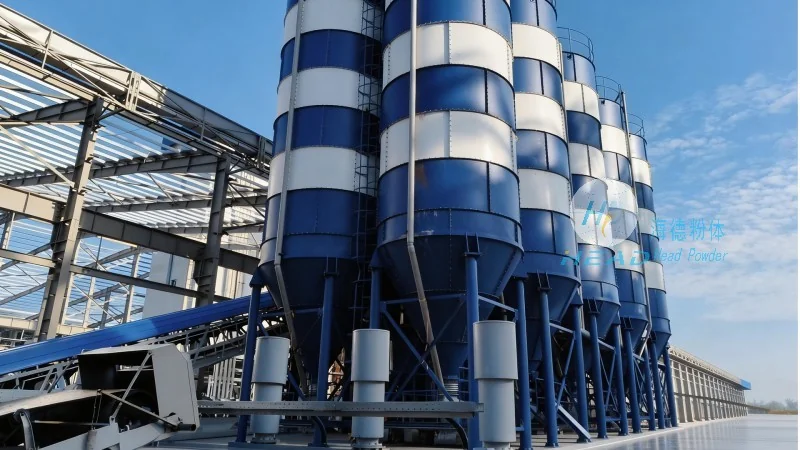
About HeadPowder: Leading Graphite Powder Conveying Solutions
HeadPowder, operating from Shandong, China, is dedicated to delivering high-quality equipment for the efficient handling of graphite powders. As a reputable entity in the field, the company leverages years of expertise to develop systems that ensure safe, reliable, and efficient material transport. The graphite powder conveying systems offered by HeadPowder are engineered to address the unique challenges associated with handling fine, abrasive, and potentially hazardous powders like graphite.

Principle of Graphite Powder Conveying Systems
The graphite powder conveying system operates on the principle of pneumatic or mechanical transport, depending on the specific requirements of the application. In pneumatic systems, compressed air is used to create a flow that carries the graphite powder through a network of pipes. This method is particularly effective for long-distance transport and can handle large volumes of material with minimal maintenance. Mechanical systems, on the other hand, utilize screw conveyors, belt conveyors, or bucket elevators to move the powder. These systems are often preferred in environments where air quality must be strictly controlled or where the material is sensitive to air exposure. The choice between pneumatic and mechanical transport is typically determined by factors such as the material's properties, the distance to be covered, and the desired level of control over the conveying process.
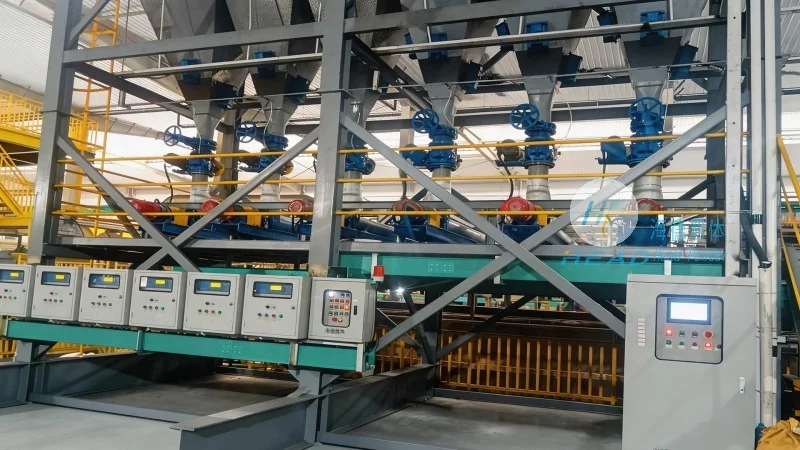
Working Scene Characteristics of Graphite Powder Conveying Systems
The operational environment of a graphite powder conveying system is characterized by several key factors that influence its design and performance. Firstly, the system must be capable of handling the fine, dry nature of graphite powder, which can be prone to dust generation and clogging. To mitigate these issues, the equipment is often equipped with features such as dust collection systems, anti-static measures, and self-cleaning mechanisms. Secondly, the system operates in industrial settings where space constraints and integration with existing production lines are critical. The compact design of many conveying systems allows for seamless integration into existing workflows, reducing downtime and increasing overall productivity. Thirdly, the system must meet safety standards to handle potentially hazardous materials. This includes features like explosion-proof components, proper ventilation, and regular maintenance protocols to ensure safe operation. Additionally, the system's performance is evaluated based on factors like conveying capacity, material flow control, and energy efficiency, all of which are tailored to the specific needs of the application.
Applications and Industry Integration
Graphite powder conveying systems are widely used in various industries, including battery manufacturing, lubricant production, and refractory materials processing. In battery manufacturing, for example, the system ensures that graphite powder is delivered to production lines with precision, maintaining consistent quality and reducing waste. In lubricant production, the system helps in the efficient mixing of graphite with other components, enhancing the final product's performance. The adaptability of these systems allows them to be customized for different production scales, from small-scale laboratory applications to large-scale industrial operations. This flexibility makes them a valuable asset for companies looking to optimize their material handling processes and improve overall operational efficiency.
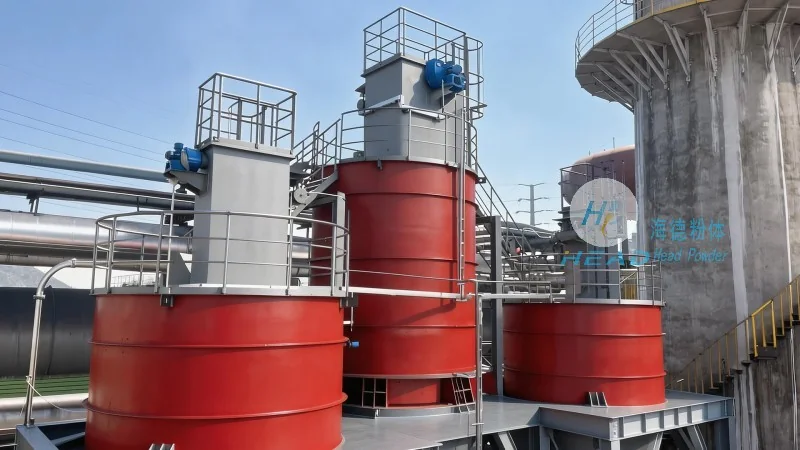
Advantages and Future Trends
The graphite powder conveying systems offered by HeadPowder provide several advantages over traditional handling methods. These include improved safety through reduced manual handling, increased efficiency through automated control, and enhanced product quality through consistent material flow. As technology advances, there is a growing emphasis on integrating smart features into these systems, such as real-time monitoring, predictive maintenance, and data analytics. These advancements help in optimizing performance, reducing downtime, and ensuring compliance with industry regulations. The future of graphite powder conveying systems lies in their continued evolution to meet the increasing demands of modern industrial applications, with a focus on sustainability, efficiency, and reliability.