

Principle and Working Scene Characteristics of Calcined Ash Powder Conveying System Equipment
Calcined ash, a byproduct of industrial processes such as coal combustion, requires efficient handling and transportation. The calcined ash powder conveying system equipment from Shandong HeadPowder Engineering Co., Ltd. addresses these needs through advanced engineering solutions designed to ensure reliable and safe material transport. This article explores the underlying principles of the system and highlights key characteristics of its operational scenarios.
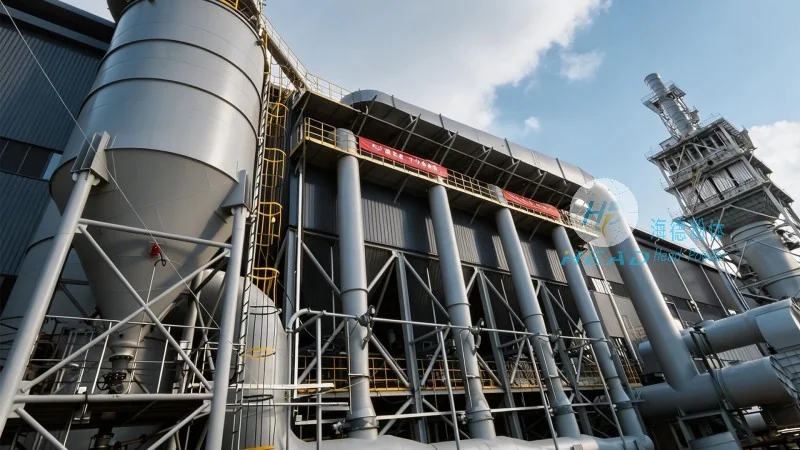
System Principle: How the Calcined Ash Powder Conveying System Works
The calcined ash powder conveying system operates on the principle of pneumatic or mechanical transport, depending on the specific application requirements. For most industrial settings, a combination of positive pressure air flow and specialized conveying components is employed. The system typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line with appropriate ductwork, and a receiver for the discharged material. The core mechanism involves the introduction of compressed air into the conveying line, which creates a flow that lifts and transports the calcined ash particles. This method is particularly effective for handling fine powders and minimizes dust generation compared to traditional methods like bucket elevators or belt conveyors.
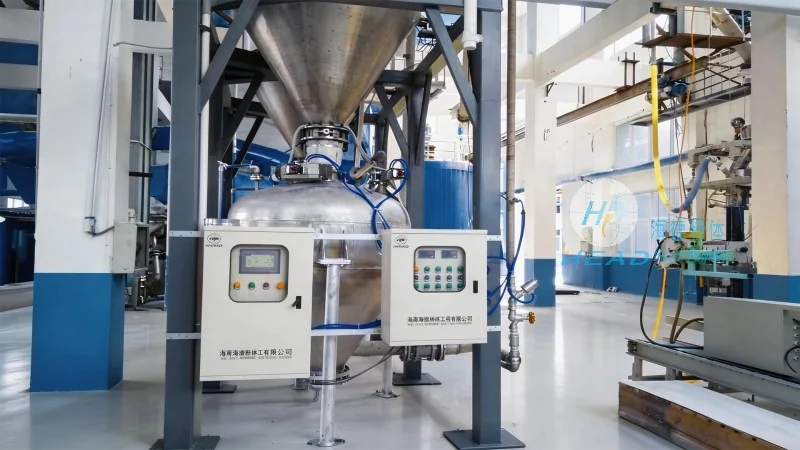
Key Components and Their Functions
Each component of the calcined ash powder conveying system plays a critical role in ensuring efficient operation. The hopper, often equipped with a level indicator, stores the calcined ash and provides a consistent feed to the feeder. The feeder, which may be a rotary valve or a screw feeder, regulates the material flow rate to match the conveying capacity of the system. The conveying line, constructed from materials resistant to corrosion and abrasion (such as stainless steel or special alloys), is designed to withstand the harsh conditions of calcined ash particles. The receiver, typically a large storage tank or a discharge hopper, collects the transported material and prepares it for subsequent processing or disposal. Additionally, the system may include dust collection and filtration equipment to comply with environmental regulations and maintain workplace safety.
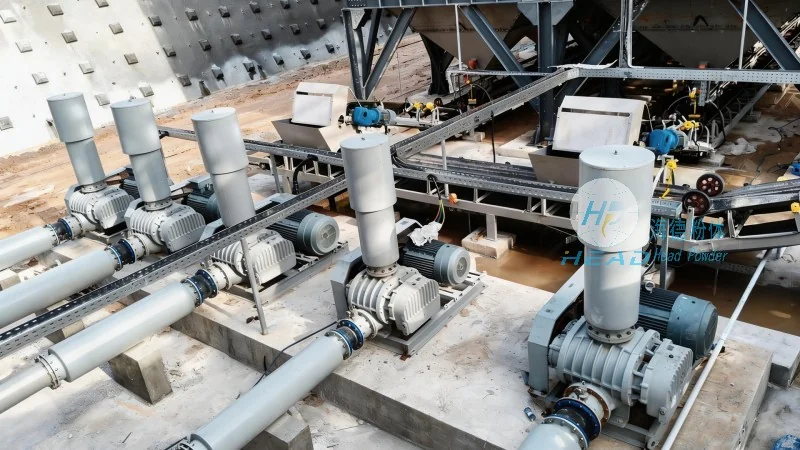
Working Scene Characteristics: Applications and Operational Environments
The calcined ash powder conveying system is widely used in various industrial sectors, including power plants, cement factories, and waste management facilities. In power plants, the system is essential for transporting calcined ash from the boiler to storage or disposal sites, ensuring that the ash is handled without causing environmental contamination. In cement factories, the system aids in the transport of calcined ash as a raw material or as a supplementary fuel, contributing to the overall efficiency of the production process. The operational environment for these systems is often characterized by high temperatures, abrasive particles, and the need for continuous operation, which requires robust and reliable equipment design.
Advantages in Different Operational Scenarios
The calcined ash powder conveying system offers several advantages in diverse operational scenarios. One of the primary benefits is its ability to handle fine powders without clogging or blockages, which is crucial for maintaining consistent production rates. The system also reduces labor costs by automating the material transport process, minimizing the need for manual handling. Furthermore, the enclosed design of the conveying line helps to control dust emissions, improving workplace safety and compliance with environmental standards. In industrial settings where space is limited, the compact design of the system allows for flexible installation, adapting to various facility layouts. The system's low maintenance requirements and long service life also contribute to its cost-effectiveness over time.
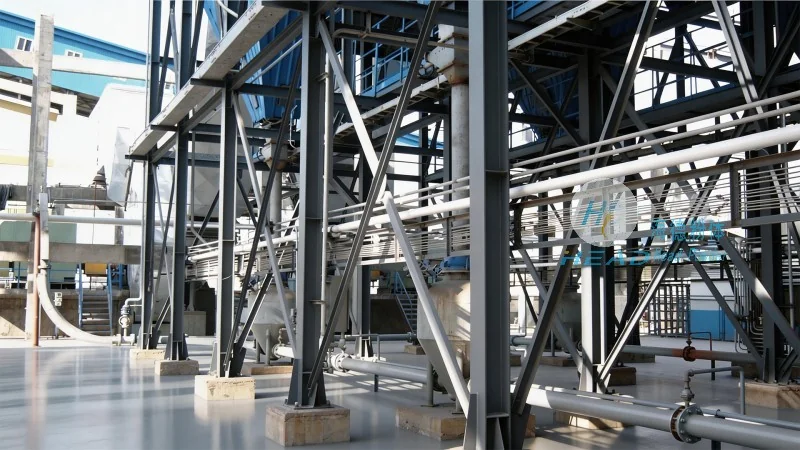
Conclusion: The Role of Shandong HeadPowder Engineering Co., Ltd. in Providing Effective Solutions
Shandong HeadPowder Engineering Co., Ltd., with its expertise in powder handling technology, provides calcined ash powder conveying systems that meet the specific needs of industrial clients. The company's commitment to quality and innovation ensures that its equipment operates reliably in demanding environments. By understanding the unique characteristics of calcined ash and the operational requirements of different industries, HeadPowder engineers design systems that optimize material transport efficiency while maintaining safety and environmental compliance. The calcined ash powder conveying system, as a key component of industrial material handling, plays a vital role in modern manufacturing and waste management processes, and companies like HeadPowder continue to advance the technology to meet evolving industry demands.