

Principle and Working Scene Characteristics of Ore Powder Material Handling System Equipment
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in the design, development, and supply of advanced ore powder material handling systems. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable ore powder transportation. This article explores the fundamental principles behind these systems and highlights the key characteristics of their operational environments.
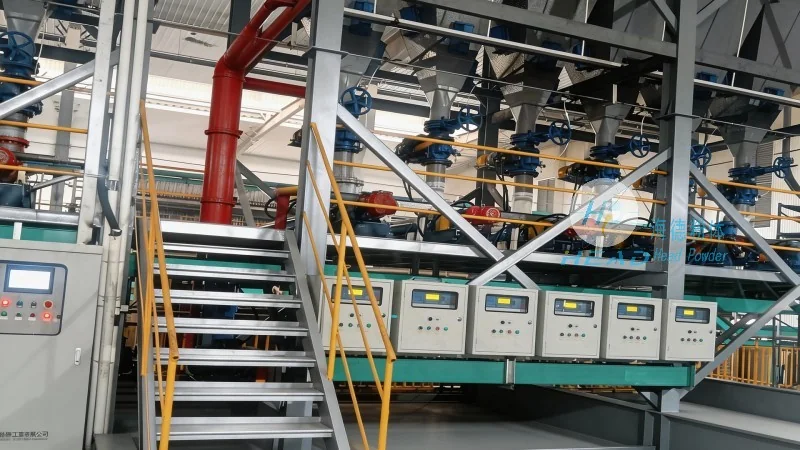
Company Overview and Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is dedicated to providing high-quality ore powder handling equipment. The company leverages years of industry experience to deliver systems that meet the diverse needs of mining, chemical, and other industrial sectors. HeadPowder's commitment to innovation and customer satisfaction has positioned it as a key player in the material handling equipment market, with a focus on ore powder applications.
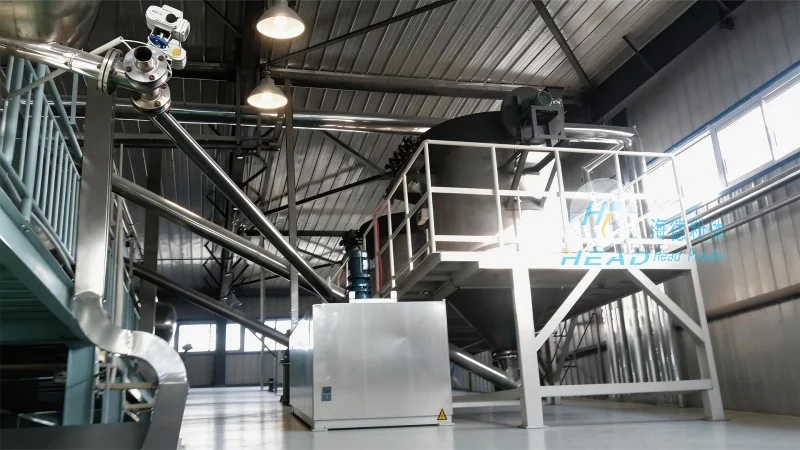
The Core Principle of Ore Powder Material Handling Systems
Ore powder material handling systems are engineered to transport fine ore powders efficiently and safely. The fundamental principle involves the use of specialized equipment such as conveyors, pneumatic transport systems, and storage solutions to move ore powder from one location to another. These systems are designed to handle the unique challenges posed by ore powders, including their fine particle size, dust generation, and potential for caking or bridging. The core technology often includes components like screw conveyors, bucket elevators, and pneumatic ducts, each tailored to the specific characteristics of the ore powder being handled.
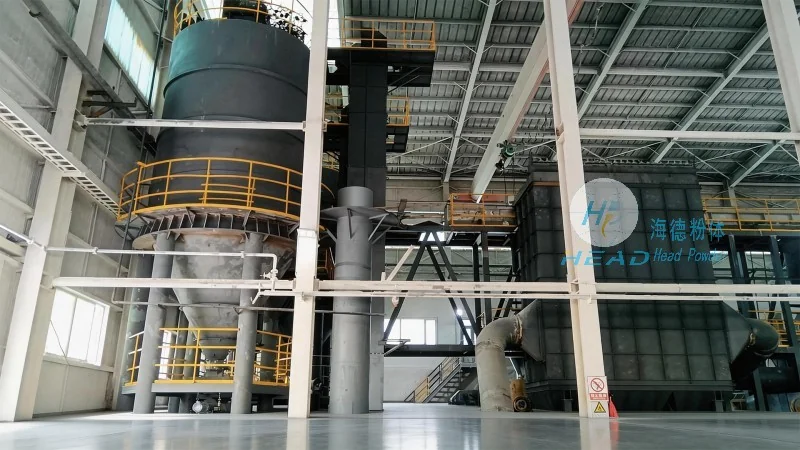
Key Working Scene Characteristics
The operational environments of ore powder material handling systems are characterized by several critical factors that influence system design and performance. First, the systems must be capable of handling high volumes of ore powder while maintaining low energy consumption and minimal maintenance requirements. Second, the equipment must be designed to prevent dust emissions and ensure compliance with environmental regulations, which is crucial in industrial settings. Third, the systems need to be adaptable to varying ore powder compositions and flow rates, allowing for flexibility in different production scenarios. Additionally, the working scenes often involve integration with other industrial processes, such as crushing, grinding, and blending, requiring seamless coordination between different equipment units.
Advantages in Real-World Applications
HeadPowder's ore powder material handling systems offer several advantages in real-world applications. The systems are designed to enhance productivity by ensuring a continuous and reliable flow of ore powder, which is essential for maintaining production efficiency in mining and processing plants. The use of advanced materials and engineering techniques minimizes downtime and reduces maintenance costs, contributing to overall operational savings. Furthermore, the systems are built to withstand harsh industrial conditions, including high temperatures, corrosive environments, and heavy usage, ensuring long-term durability and reliability. The integration of automation and control systems allows for precise monitoring and adjustment of the material flow, optimizing performance and reducing human error.
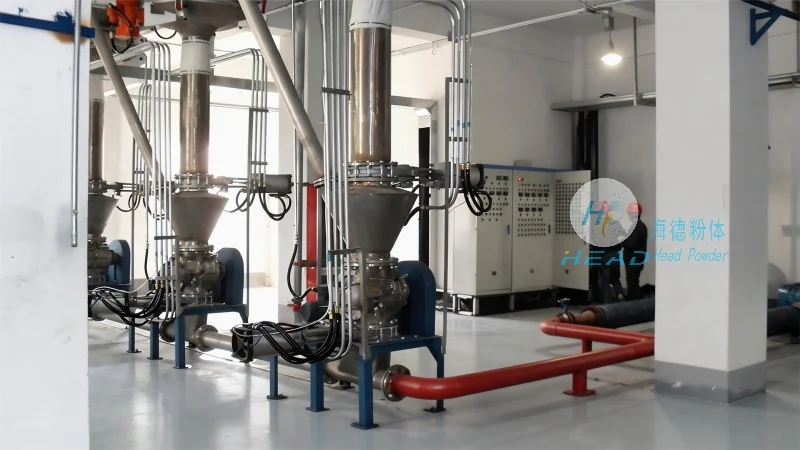
Conclusion
HeadPowder's ore powder material handling systems exemplify the principles of efficient and reliable material transportation. By understanding the core principles and working scene characteristics, industries can leverage these systems to improve their operational efficiency and meet their production goals. With a strong foundation in engineering and a commitment to quality, HeadPowder continues to provide innovative solutions for ore powder handling, supporting the growth and success of its clients in the industrial sector.