

Principles and Application Scenarios of Multi-functional Powder Pneumatic Conveying Systems
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems for diverse powder applications. This article explores the fundamental principles behind multi-functional powder pneumatic conveying systems and highlights key operational scenarios where these systems excel in material transport and processing.
Understanding the Core Principles of Multi-functional Powder Pneumatic Conveying
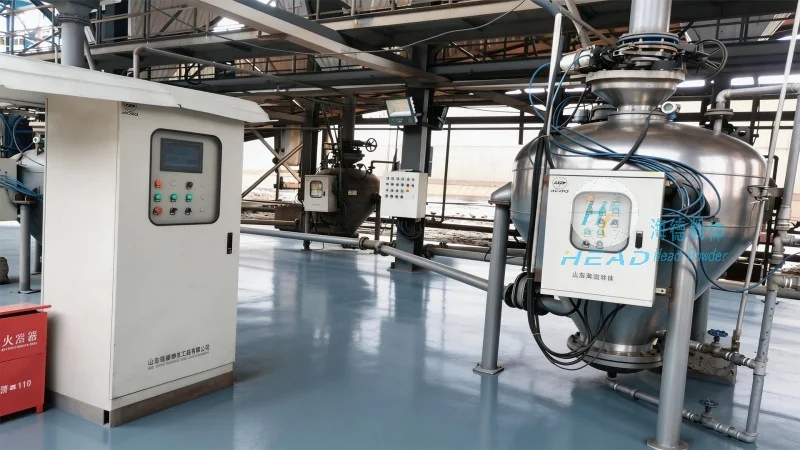
At the heart of a multi-functional powder pneumatic conveying system lies the integration of several core technologies that enable efficient and versatile material transport. The system typically operates on the principle of using compressed air or other gases to create a flow that propels powders through a network of pipes and components. This method, known as pneumatic conveying, offers significant advantages over traditional mechanical conveying methods, such as reduced equipment wear, lower maintenance requirements, and the ability to handle a wide range of powder characteristics.
Key components of a multi-functional system include the air compressor, which generates the necessary pressure to move the material; the feed hopper, which stores and dispenses the powder; and the conveying line, which transports the material from the source to the destination. The system may also incorporate features like cyclone separators, filters, and control valves to ensure optimal performance and material quality. By combining these elements, the system can adapt to various operational needs, making it suitable for both small-scale and large-scale industrial applications.
Key Application Scenarios for Multi-functional Powder Pneumatic Conveying Systems
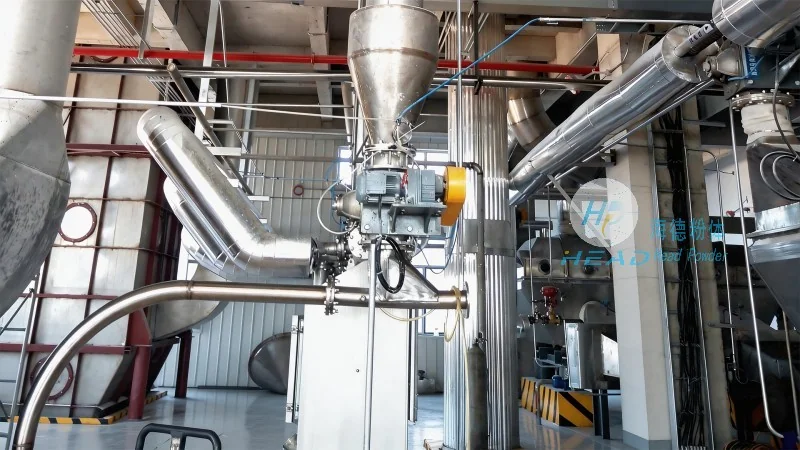
Multi-functional powder pneumatic conveying systems are widely used across various industries due to their adaptability and efficiency. One common application is in the pharmaceutical industry, where systems are employed to transport active pharmaceutical ingredients (APIs) and other powders with strict purity and contamination control requirements. The enclosed nature of the system prevents cross-contamination and ensures that the material remains in a controlled environment throughout the transport process.
In the food and beverage sector, these systems are utilized for handling ingredients like flour, sugar, and spices. The ability to maintain product integrity and prevent moisture absorption is crucial, and the pneumatic conveying method achieves this by minimizing direct contact with air and reducing the risk of contamination. Additionally, the system can be integrated with dust collection and filtration systems to meet regulatory standards for food safety.
Another significant application is in the chemical industry, where systems transport various powders, including chemicals, pigments, and catalysts. The robust design of the multi-functional system allows it to handle abrasive and corrosive materials, ensuring long-term durability and reliability. The system's ability to operate under different pressure and flow conditions makes it suitable for processes that require precise material control, such as in chemical synthesis and production lines.
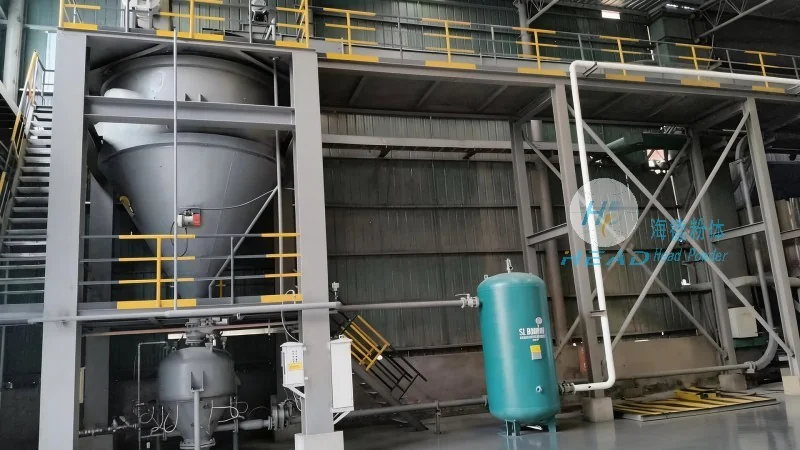
In the agricultural sector, multi-functional powder pneumatic conveying systems are used to transport bulk materials like fertilizers, seeds, and animal feed. The system's flexibility allows it to handle different particle sizes and moisture content, making it ideal for agricultural processing and storage. By efficiently moving these materials from storage silos to processing facilities or distribution points, the system enhances operational efficiency and reduces labor costs.
Advantages and Considerations for Implementing Multi-functional Powder Pneumatic Conveying Systems
Implementing a multi-functional powder pneumatic conveying system offers numerous benefits for industrial operations. The primary advantage is the reduction in material handling costs, as the system eliminates the need for manual or mechanical loading and unloading processes. This not only saves time but also minimizes the risk of material spillage and workplace accidents. Additionally, the enclosed system design improves workplace safety by containing dust and preventing exposure to hazardous materials.
Another key advantage is the improved material quality control. By maintaining a controlled environment and minimizing material contact with external elements, the system ensures that the powder remains in its original state, free from contamination or degradation. This is particularly important for products that require high purity, such as pharmaceuticals and food ingredients. The system's ability to handle fine powders without clogging or agglomeration further enhances product quality.
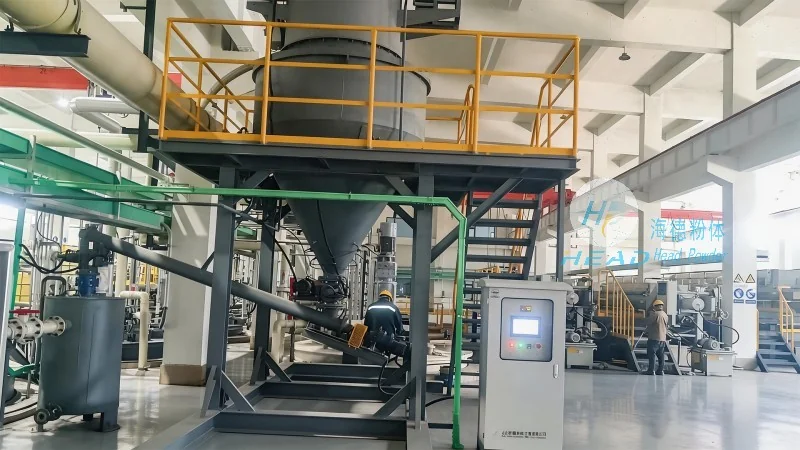
However, there are also considerations to keep in mind when implementing such systems. The initial investment cost can be higher compared to traditional conveying methods, and the system requires regular maintenance to ensure optimal performance. Additionally, the system's efficiency depends on proper design and operation, as improper setup can lead to increased energy consumption and reduced material flow rates. Proper training of operators and regular system checks are essential to maximize the benefits of the multi-functional powder pneumatic conveying system.
Conclusion
Multi-functional powder pneumatic conveying systems represent a sophisticated solution for efficient and reliable material transport in various industrial applications. By leveraging advanced pneumatic technology and integrated components, these systems offer versatility, durability, and enhanced material quality control. As industries continue to demand more efficient and sustainable material handling solutions, the adoption of such systems is expected to grow, particularly in sectors where product purity and operational efficiency are critical. HeadPowder, with its expertise in engineering and implementation, remains at the forefront of providing tailored solutions that meet the unique needs of its clients.