

Principle and Working Scene Characteristics of Sodium Nitrate Material Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, specializes in providing advanced material handling solutions. One of their core offerings is the pneumatic conveying system designed specifically for sodium nitrate, a critical chemical widely used in agriculture, food preservation, and industrial applications. This system combines efficiency, reliability, and safety, making it an ideal choice for various industrial environments.
Principle of the Pneumatic Conveying System
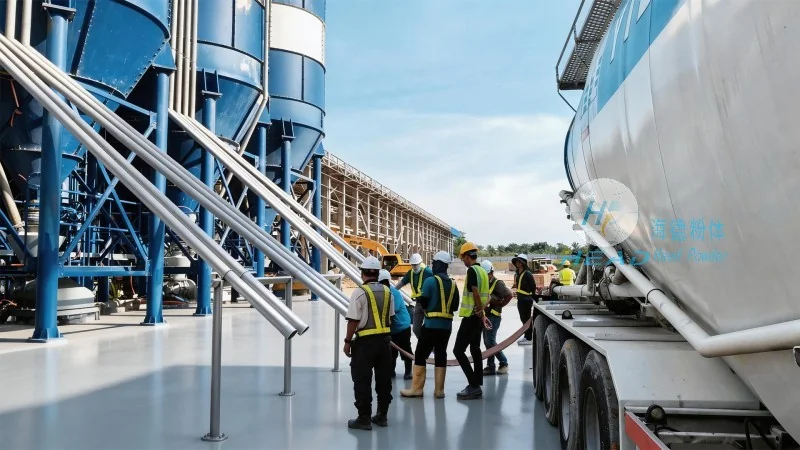
The pneumatic conveying system for sodium nitrate operates on the fundamental principle of using air or gas to transport bulk materials through a pipeline. The system typically consists of a hopper, a rotary valve, a conveying line, and a receiver. The process begins when the sodium nitrate is fed into the hopper. The rotary valve then controls the material flow into the conveying line. Compressed air is introduced into the line, creating a flow that propels the material forward. The air velocity is carefully controlled to ensure the material is transported without degradation or blockage. The system can be either positive pressure (where air pushes the material) or negative pressure (where air pulls the material), depending on the specific application and material characteristics. The design ensures that the sodium nitrate is handled gently, preserving its quality and preventing dust generation or contamination.
Working Scene Characteristics
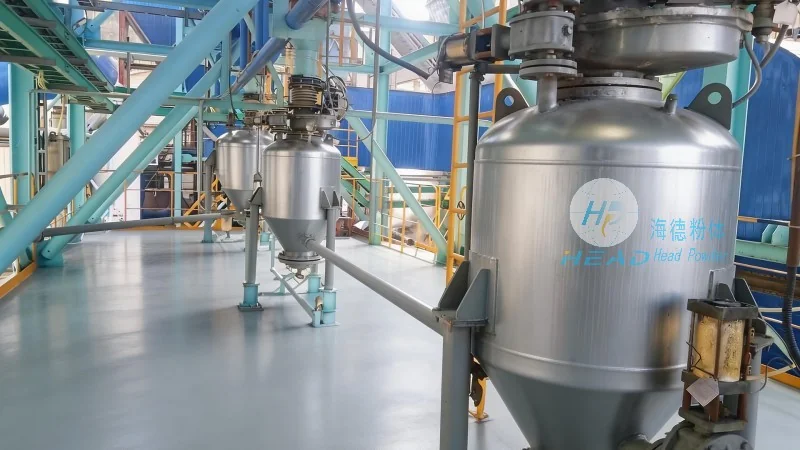
The working scene characteristics of the sodium nitrate pneumatic conveying system are tailored to meet the demands of diverse industrial settings. These systems are commonly used in fertilizer production facilities, where sodium nitrate is a key ingredient in nitrogen-based fertilizers. The system's ability to handle large volumes of material efficiently supports high production rates. In food processing plants, the system ensures the safe and hygienic transfer of sodium nitrate, which is used as a preservative. The design also accommodates environments where dust control is essential, such as in chemical processing plants. The system's flexibility allows it to be integrated into existing production lines, minimizing downtime and operational disruptions. Additionally, the system's compact design makes it suitable for facilities with limited space, while its durability ensures long-term performance even under harsh conditions.
Key Features and Advantages
HeadPowder's pneumatic conveying system for sodium nitrate offers several key features that enhance its performance and reliability. The system is equipped with advanced control systems that allow for precise regulation of air pressure and material flow, ensuring consistent operation. The use of high-quality materials in the construction of the conveying line and components ensures resistance to corrosion and wear, which is crucial for handling sodium nitrate, a chemical that can be abrasive. The system's design minimizes the risk of material buildup and blockages, reducing maintenance requirements and improving overall efficiency. Additionally, the system is designed with safety in mind, incorporating features such as dust suppression and explosion-proof components, which are essential in industrial environments where sodium nitrate is used. The system's energy efficiency is another significant advantage, as it reduces operational costs while maintaining high performance.
Application Examples
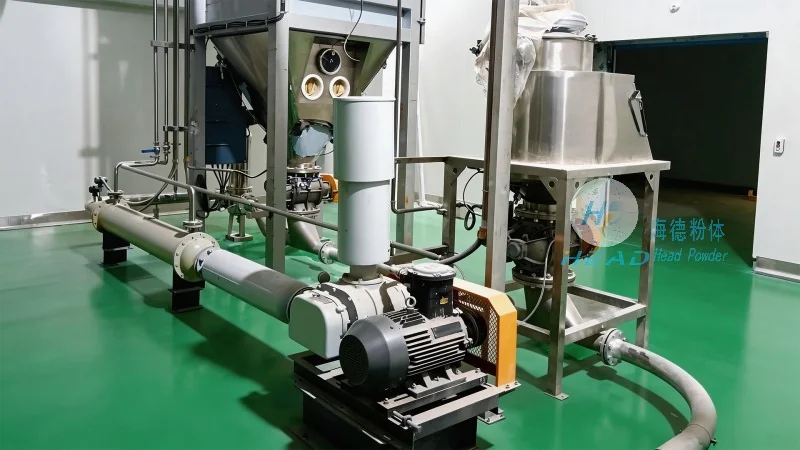
The pneumatic conveying system for sodium nitrate is applied in various scenarios across different industries. In the agricultural sector, it is used to transport sodium nitrate from storage silos to mixing and packaging lines in fertilizer manufacturing plants. The system's ability to handle large quantities of material quickly and accurately supports the high throughput required in modern fertilizer production. In the food industry, the system is used to transfer sodium nitrate from bulk storage to processing equipment in food processing facilities. The system's hygienic design ensures that the material remains free from contamination, meeting strict food safety standards. In industrial chemical plants, the system is used to convey sodium nitrate between different processing stages, such as from a drying unit to a packaging line. The system's flexibility allows it to be adapted to different production processes, making it a versatile solution for various applications.