

Principle and Working Scene Characteristics of Paddy Husk Ash Material Pneumatic Conveying System
Pneumatic conveying systems are essential for transporting bulk materials like paddy husk ash efficiently and safely. These systems utilize air as the conveying medium, enabling the movement of materials through pipelines without the need for mechanical components like belts or buckets. The core principle involves creating a flow of air that suspends the material particles, allowing them to be transported over long distances with minimal friction and energy consumption.
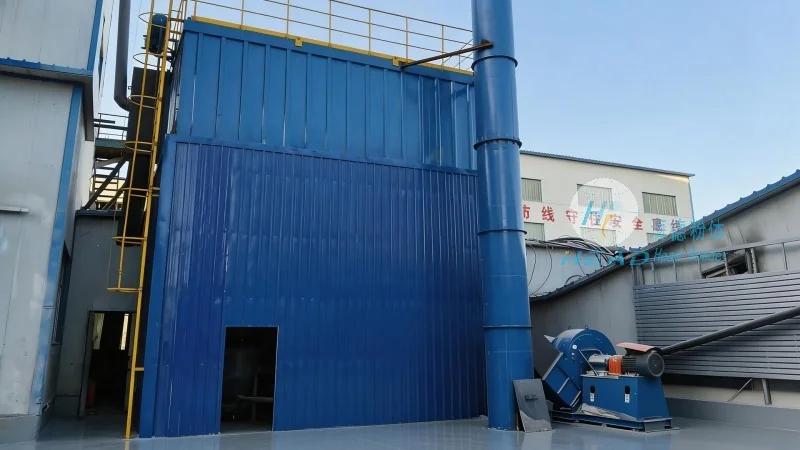
Working Principle of Paddy Husk Ash Pneumatic Conveying
The operation of a paddy husk ash pneumatic conveying system is based on the interaction between air and the material particles. When compressed air is introduced into the system, it creates a pressure differential that lifts and transports the ash particles. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The air velocity and pressure are carefully regulated to ensure the material remains suspended and does not settle or clog the pipeline. This method is particularly effective for fine or dusty materials like paddy husk ash, as it prevents dust dispersion and maintains a clean working environment.
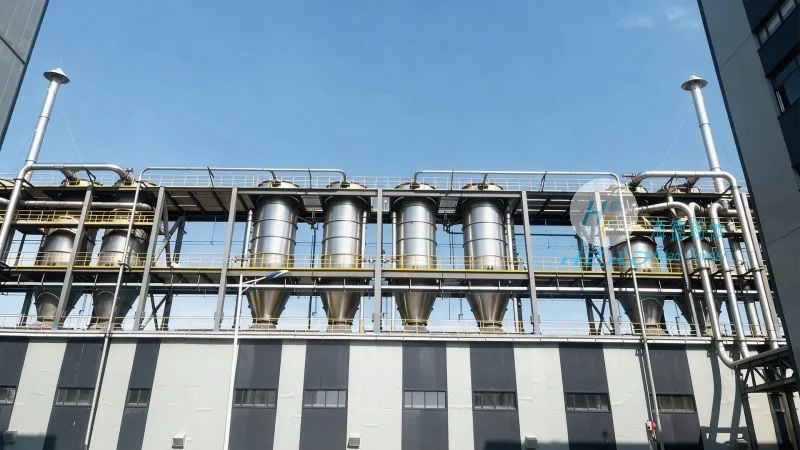
Key Features and Advantages in Working Scenarios
In industrial applications, the working scene characteristics of paddy husk ash pneumatic conveying systems are tailored to specific operational needs. For example, in biomass power plants or waste-to-energy facilities, these systems are used to transport ash from boilers to storage or treatment areas. The systems are designed to handle varying ash compositions, including different moisture levels and particle sizes, ensuring consistent performance. Key advantages include high efficiency in material transport, reduced labor costs due to automated operation, and minimal environmental impact compared to traditional methods like truck or conveyor belt transport. Additionally, the enclosed system prevents dust pollution, which is crucial for maintaining air quality in industrial zones.
System Design and Customization by HeadPowder
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique requirements of paddy husk ash processing. The company’s engineers work closely with clients to assess site conditions, material properties, and operational goals, ensuring the system is optimized for maximum efficiency and reliability. Customization options include adjustable air pressure and flow rates, variable speed feeders, and different pipeline configurations to accommodate various plant layouts. The systems are constructed with durable materials such as stainless steel and high-grade plastics to withstand the corrosive and abrasive nature of paddy husk ash, ensuring long-term durability and low maintenance costs.
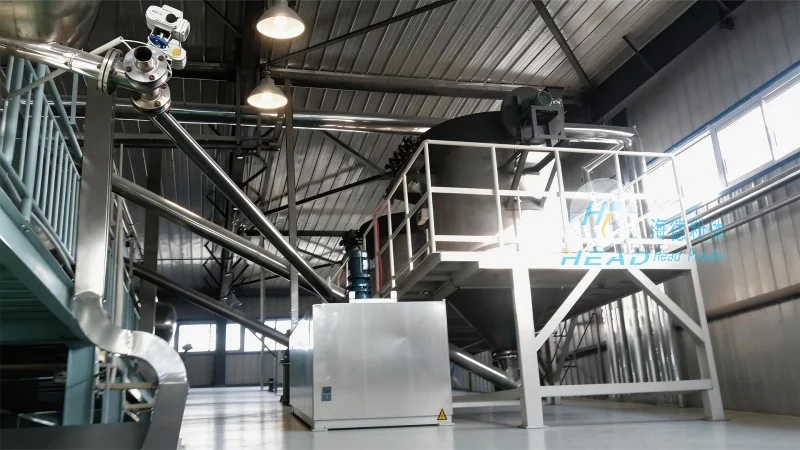
Application Examples and Operational Efficiency
Real-world applications of paddy husk ash pneumatic conveying systems demonstrate their effectiveness in various industrial settings. In a typical biomass power plant, the system transports ash from the boiler to a storage silo, covering distances of up to several hundred meters. The system operates continuously, with minimal downtime for maintenance, and can handle large volumes of ash, reducing the need for manual handling. The enclosed design also prevents ash from contaminating the surrounding environment, aligning with environmental regulations. The operational efficiency of these systems is further enhanced by advanced control systems that monitor air pressure, flow rates, and material levels, allowing for real-time adjustments to optimize performance. This results in lower energy consumption and higher throughput, making the system a cost-effective solution for ash management.