

Operation Process and Working Principle of Corn Grit Pneumatic Conveying System
The corn grit pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized equipment designed for the efficient and safe transportation of corn grit. This system is widely used in the food processing industry, particularly in corn milling and related applications. The system's design ensures optimal performance in handling the unique characteristics of corn grit, such as its granular size and moisture content, while maintaining high conveying efficiency and minimal product loss.
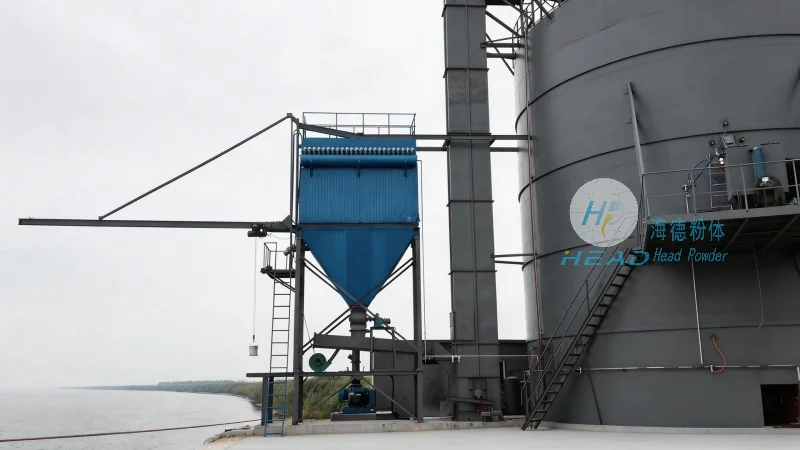
Key Components of the Pneumatic Conveying System
The corn grit pneumatic conveying system consists of several core components that work in tandem to achieve effective material transport. These components include the hopper for material storage, the air compressor or blower to generate the necessary air pressure, the conveying pipeline, and the control system for regulating the flow. Each component is carefully engineered to ensure durability and reliability under continuous operation. The hopper is designed with a sloped bottom to facilitate smooth material discharge, while the air compressor provides a consistent air flow that propels the corn grit through the pipeline. The conveying pipeline is typically made of corrosion-resistant materials to withstand the abrasive nature of corn grit and to prevent contamination. The control system allows operators to adjust the conveying speed and pressure, ensuring precise control over the material flow.
Operation Process of the Corn Grit Pneumatic Conveying System
The operation process of the corn grit pneumatic conveying system begins with the loading of corn grit into the hopper. The material is then fed into the conveying pipeline through the air flow generated by the compressor. As the air flows through the pipeline, it carries the corn grit particles, creating a dense phase or dilute phase conveying system depending on the system design. The system can operate in either positive or negative pressure modes, with positive pressure being more common for corn grit applications due to its ability to handle longer distances and more complex layouts. The control system monitors the pressure and flow rates, adjusting the air compressor speed to maintain optimal conveying conditions. The corn grit is then discharged at the receiving end, where it is collected in a storage bin or processing unit. Throughout the process, the system ensures minimal product degradation and loss, maintaining the quality of the corn grit for subsequent processing steps.
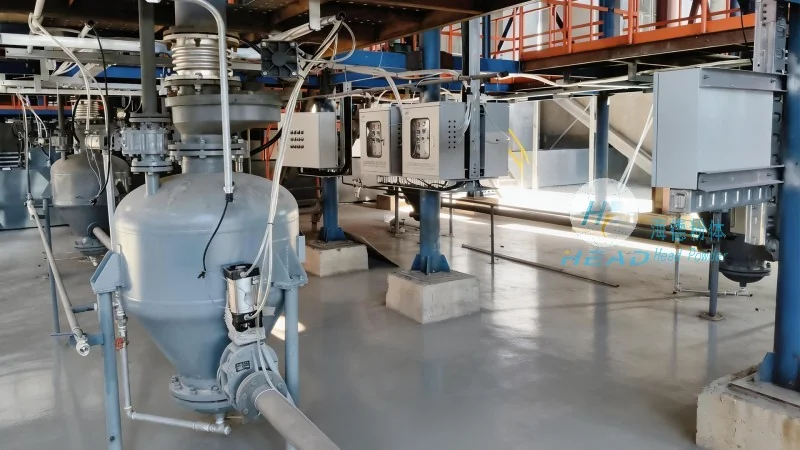
Working Principle of the Pneumatic Conveying System
The working principle of the corn grit pneumatic conveying system is based on the use of air as the conveying medium. The system utilizes the kinetic energy of the air to transport the corn grit particles. In the positive pressure mode, the air compressor pressurizes the air, which then flows through the pipeline, carrying the corn grit. The air velocity is maintained at a level that prevents the particles from settling or clogging the pipeline. The system's design ensures that the air flow is sufficient to overcome the gravitational force and frictional resistance of the corn grit, allowing for efficient transport. The control system plays a crucial role in maintaining the air pressure and flow rate, ensuring that the conveying process is smooth and consistent. The system's efficiency is further enhanced by the use of appropriate pipeline diameters and bends, which minimize pressure losses and ensure uniform material distribution.
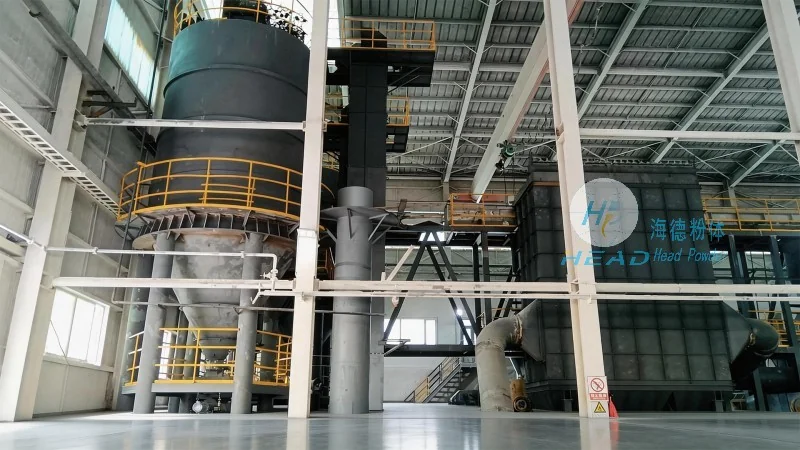
Advantages of the Corn Grit Pneumatic Conveying System
Compared to traditional mechanical conveying systems, the corn grit pneumatic conveying system offers several advantages. One of the key benefits is the ability to transport corn grit over long distances without the need for multiple transfer points. This reduces the risk of product contamination and loss, as the material is conveyed in a closed system. The system also provides better control over the material flow, allowing for precise adjustment of the conveying speed and pressure. This is particularly important in food processing applications, where maintaining product quality is critical. Additionally, the system is more hygienic and easier to clean, as the conveying pipeline is made of smooth, corrosion-resistant materials that can be easily sanitized. The system's compact design also saves space in the processing facility, making it suitable for both new and existing installations.
Application and Maintenance Considerations
The corn grit pneumatic conveying system is widely used in various applications within the food processing industry, including corn milling, corn flour production, and corn syrup processing. The system's ability to handle different particle sizes and moisture contents makes it versatile for a range of corn grit products. Regular maintenance is essential to ensure the system's optimal performance and longevity. This includes checking the air compressor for proper operation, inspecting the conveying pipeline for any signs of wear or damage, and cleaning the hopper and control system to prevent clogging. The system's control panel should be checked regularly to ensure that all settings are correct and that the system is operating within safe parameters. Proper maintenance not only extends the life of the equipment but also ensures consistent product quality and minimal downtime.