

Operation Process and Working Principle of Glucose Powder Conveying System
Glucose powder conveying systems are critical components in various industrial applications, particularly in the pharmaceutical, food, and chemical sectors. These systems are designed to efficiently transport glucose powder from storage to processing units, ensuring consistent flow and minimal product degradation. The operation of such systems involves a series of integrated processes that work in tandem to achieve optimal performance. This article provides a detailed overview of the operation process and working principles of glucose powder conveying systems, highlighting key components and their functions.

Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling solutions, specializes in the design, development, and implementation of advanced conveying systems. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for businesses requiring reliable and efficient powder transport solutions. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality products and services tailored to the specific needs of its clients.
Key Components and Working Principles
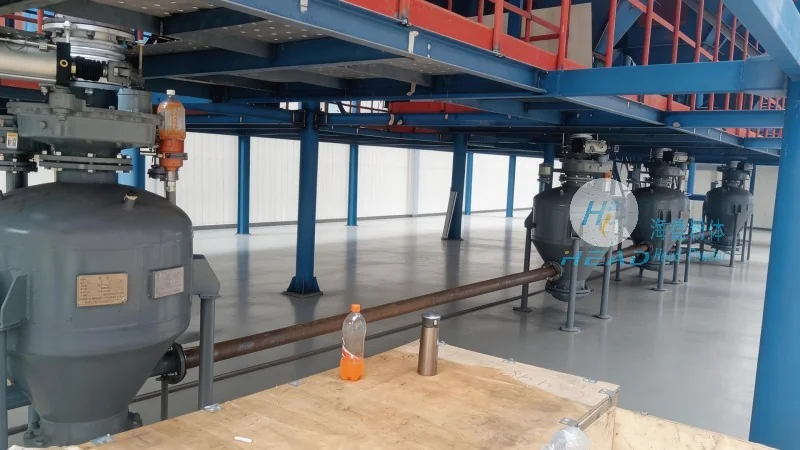
The glucose powder conveying system typically consists of several key components, each playing a vital role in the overall operation. The primary components include a hopper for powder storage, a feeder mechanism to control the flow rate, a conveyor system (such as a screw conveyor or pneumatic conveyor) to transport the powder, and a control panel to monitor and adjust the system parameters. The working principle revolves around the controlled movement of glucose powder from the storage hopper to the processing equipment through these interconnected components.
Operation Process: Step-by-Step Overview
The operation of a glucose powder conveying system begins with the loading of glucose powder into the storage hopper. The hopper is designed to maintain the powder in a stable condition, preventing caking or agglomeration. Once the hopper is filled, the feeder mechanism, often a rotary valve or a vibratory feeder, starts to regulate the flow of powder. This controlled release ensures a consistent feed rate to the conveyor system. The conveyor system then transports the powder to the processing unit, such as a mixer or a reactor, where it is used in the production process. The control panel continuously monitors parameters like flow rate, pressure, and temperature, allowing operators to make real-time adjustments to maintain optimal performance.
Advantages and Applications
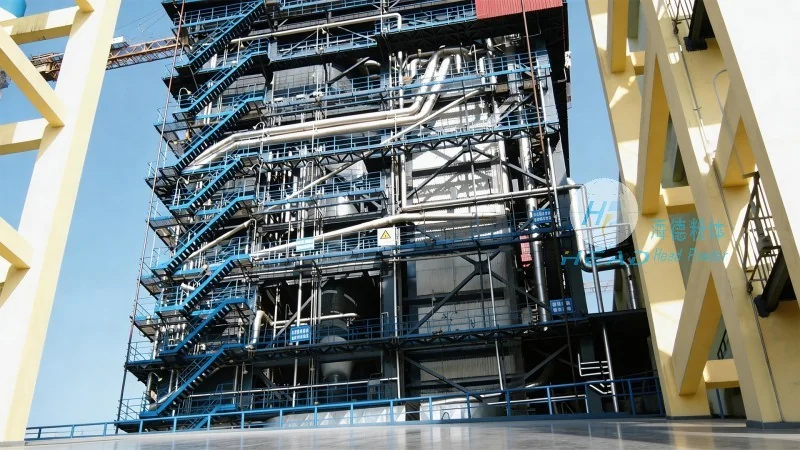
Glucose powder conveying systems offer several advantages, including high efficiency, minimal product loss, and reduced labor costs. They are widely used in the pharmaceutical industry for the transport of active pharmaceutical ingredients (APIs), in the food industry for the handling of glucose as a sweetener or nutrient, and in the chemical industry for the processing of glucose-based products. The systems are designed to handle various powder characteristics, such as particle size, moisture content, and flowability, ensuring compatibility with different production requirements.
Maintenance and Troubleshooting
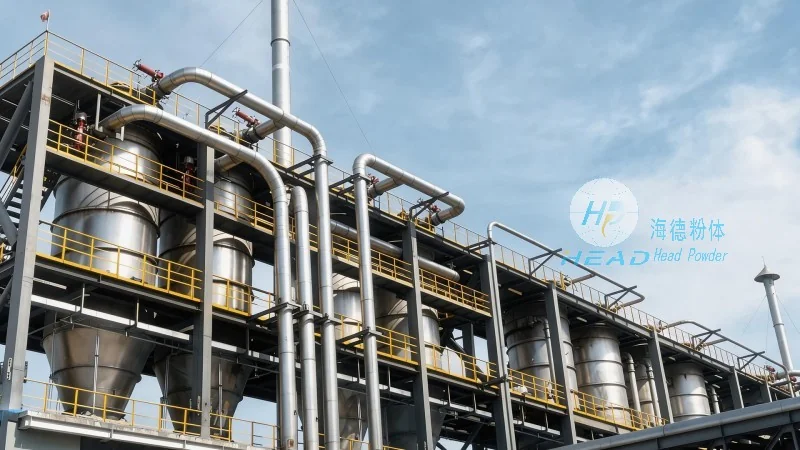
To ensure the long-term reliability of glucose powder conveying systems, regular maintenance is essential. This includes cleaning the hopper and conveyor components to prevent powder buildup, inspecting the feeder mechanism for wear and tear, and checking the control panel for proper functionality. Common issues that may arise include clogging of the conveyor, uneven flow rates, or malfunctions in the control system. Proper troubleshooting procedures, as outlined by HeadPowder, help in identifying and resolving these issues quickly, minimizing downtime and maintaining production efficiency.
Conclusion
In conclusion, glucose powder conveying systems are sophisticated and reliable solutions for the efficient transport of glucose powder in industrial settings. The operation process, which involves careful control of flow rates and system parameters, ensures consistent performance and product quality. With its expertise in powder handling technology, Shandong HeadPowder Engineering Co., Ltd. provides high-quality systems that meet the diverse needs of its clients, contributing to enhanced productivity and operational efficiency in various industries.