

Operation Process and Working Principle of PUR Powder Pneumatic Conveying Machine
HeadPowder, a leading manufacturer headquartered in Shandong, China, specializes in the design, production, and supply of advanced pneumatic conveying systems, including the PUR powder pneumatic conveying machine. This equipment is engineered to efficiently transport dry powders and granules over long distances with minimal product degradation and high reliability, making it a preferred choice in various industrial sectors.
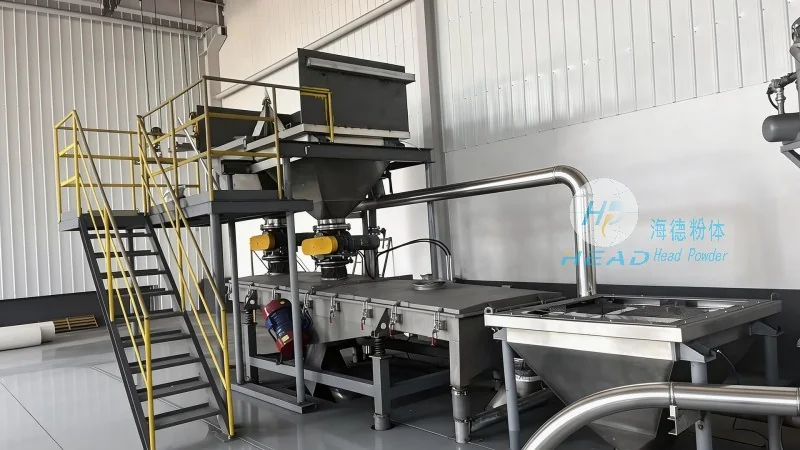
Overview of the PUR Powder Pneumatic Conveying Machine
The PUR powder pneumatic conveying machine is a sophisticated system that utilizes air or gas as the medium to transport bulk materials. It integrates positive and negative pressure conveying technologies, offering flexibility in application and ensuring efficient material transfer. The machine is widely used in industries such as food, pharmaceuticals, chemicals, and plastics due to its ability to handle sensitive powders without contamination or loss of quality, maintaining product integrity throughout the process.
Key Components and Their Functions
The PUR powder pneumatic conveying machine comprises several critical components that work in unison to achieve effective material transport. These include the hopper (material storage and feeding unit), the airlock or rotary valve (controls material flow into the conveying line), the conveying pipe (carries the material-air mixture), the filter and separator (separates material from air), and the blower or vacuum pump (provides necessary air pressure or suction). Each component is designed to optimize performance and ensure smooth, continuous operation, reducing downtime and maintenance requirements.
Working Principle of the Pneumatic Conveying Process
The operation of the PUR powder pneumatic conveying machine begins with material loading into the hopper. The airlock or rotary valve then regulates the discharge of material into the conveying pipe. Simultaneously, the blower generates a flow of air that either pushes the material forward (in positive pressure systems) or pulls it through the pipe (in negative pressure systems). As the material and air mixture travels through the pipe, the filter and separator capture the material particles, allowing the clean air to be discharged or recycled. The separated material is collected in the receiving hopper or container. This process ensures efficient material transport with minimal energy consumption and low operational costs, while maintaining product quality and safety.
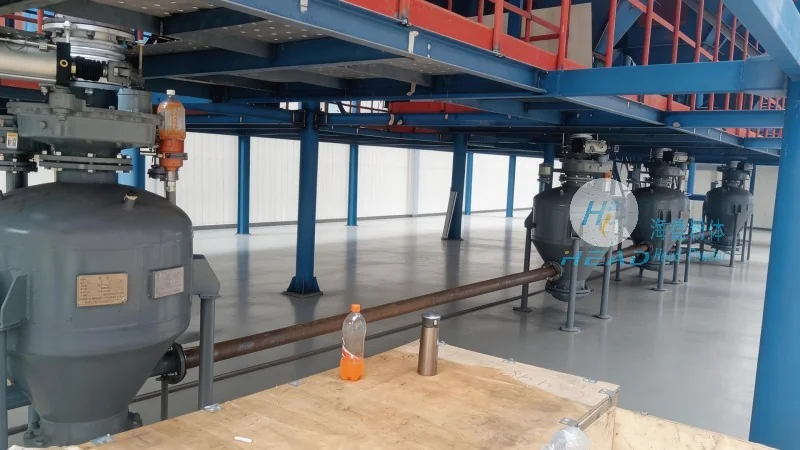
Operation Process Step-by-Step
1. **Material Loading**: Bulk powder or granules are fed into the hopper from a storage silo or container. The hopper features a sloped bottom to facilitate smooth material flow and prevent clogging.
2. **Airlock Operation**: The airlock or rotary valve opens to allow a controlled amount of material to enter the conveying pipe. This mechanism prevents material backflow into the hopper and ensures a consistent feed rate, maintaining system stability.
3. **Air Supply**: The blower or vacuum pump starts and generates the required air pressure or suction. The air flow rate is adjusted based on the material's characteristics (e.g., particle size, density) and the desired conveying distance, optimizing performance.
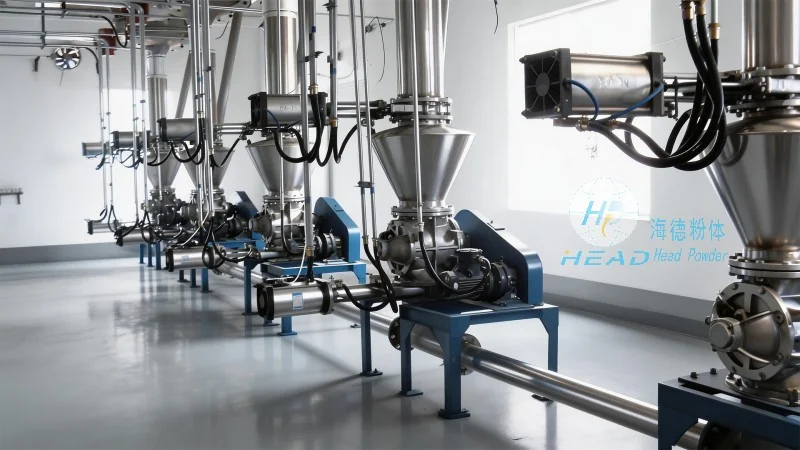
4. **Conveying**: The material is carried by the air flow through the conveying pipe. The air velocity is maintained above the material's terminal velocity to prevent particle settling and ensure continuous transport, avoiding blockages or system inefficiencies.
5. **Separation and Collection**: At the receiving end, the filter and separator separate the material from the air. The material is collected in the receiving hopper, while the air is either filtered and recycled back into the system or discharged to the atmosphere, depending on the application and environmental requirements.
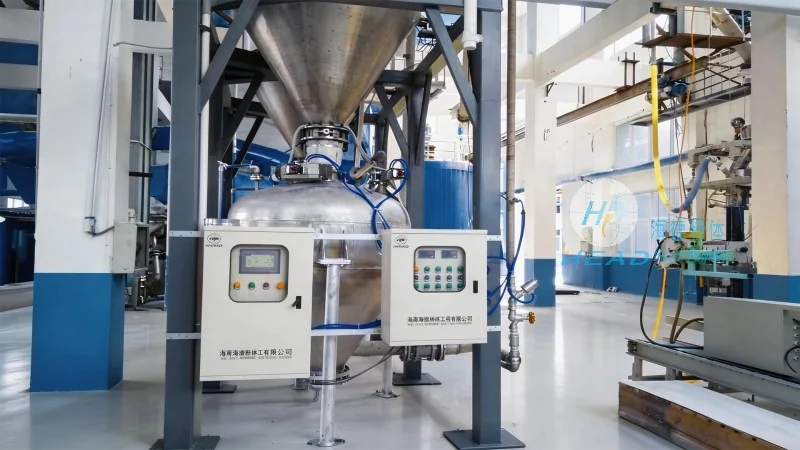
Advantages of the PUR Powder Pneumatic Conveying Machine
The PUR powder pneumatic conveying machine offers several advantages over traditional mechanical conveying methods. These include: (1) **Non-Contact Transport**: The material is conveyed without physical contact with the equipment, reducing wear and tear and preventing contamination, which is critical for industries handling food, pharmaceuticals, or sensitive chemicals. (2) **Versatility**: It can handle a wide range of powder properties, including fine, abrasive, hygroscopic, or heat-sensitive materials, making it suitable for diverse applications. (3) **Low Maintenance**: The system has fewer moving parts compared to mechanical conveyors, resulting in lower maintenance costs and longer service life, reducing operational downtime. (4) **Energy Efficiency**: Advanced designs optimize air usage, reducing energy consumption and operational costs, which is beneficial for large-scale industrial operations. (5) **Scalability**: The machine can be customized to handle different material volumes and conveying distances, making it adaptable to various production scales, from small-scale laboratory use to large industrial manufacturing.
Applications and Industries
The PUR powder pneumatic conveying machine is widely applied in industries that require the safe and efficient transport of dry powders. Some common applications include: (1) **Food and Beverage Industry**: Transporting ingredients such as flour, sugar, cocoa powder, and spices without compromising their quality or freshness, ensuring compliance with food safety regulations. (2) **Pharmaceutical Industry**: Handling active pharmaceutical ingredients (APIs) and excipients with strict contamination control measures, maintaining product purity and efficacy. (3) **Chemical Industry**: Conveying chemicals, pigments, and additives in manufacturing processes, ensuring consistent material flow and preventing cross-contamination. (4) **Plastics Industry**: Transporting resin powders and additives for plastic extrusion and molding, supporting high-speed production lines and maintaining material quality. (5) **Mining and Minerals Industry**: Moving bulk minerals and ores from storage to processing facilities, improving operational efficiency and reducing manual handling risks.
Conclusion
HeadPowder's PUR powder pneumatic conveying machine is a reliable and efficient solution for bulk material transport. By leveraging advanced pneumatic technology, this equipment ensures minimal product degradation, high transfer efficiency, and low operational costs. With its robust design and versatile applications, it meets the demands of modern industrial processes, providing businesses with a competitive edge in material handling. Based in Shandong, China, HeadPowder continues to innovate and provide high-quality pneumatic conveying systems that enhance productivity and operational safety, supporting the growth and success of industries worldwide.