

What is a High-Alumina Ash Powder Conveyor? And What Are Its Design Principles?
High-alumina ash powder conveyors are specialized equipment designed for the efficient and reliable transportation of high-alumina ash powders in industrial settings. These conveyors are engineered to handle the unique challenges associated with transporting such powders, including their abrasive nature, potential for dust generation, and the need for precise control over material flow. The design of these systems is crucial for ensuring optimal performance, safety, and longevity in various industrial applications.
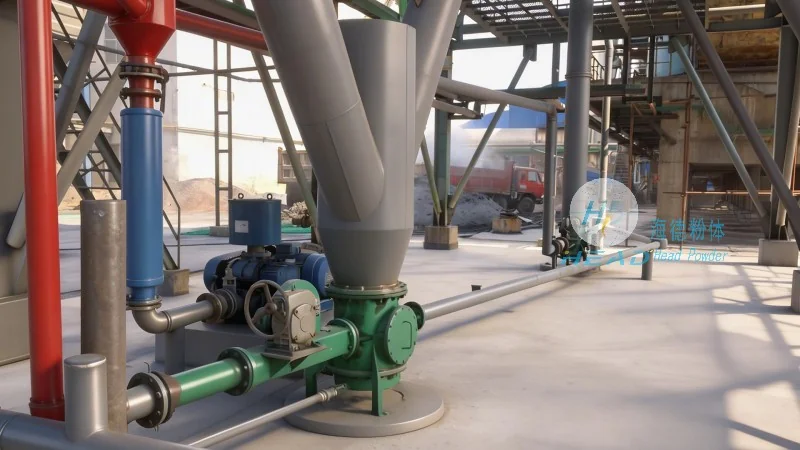
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-quality industrial conveyor systems. With a strong commitment to innovation and customer satisfaction, HeadPowder specializes in designing and producing equipment tailored to the specific needs of industries dealing with abrasive and high-density powders. The company is headquartered in Shandong, China, and has established a reputation for delivering reliable, efficient, and durable conveyor solutions that meet international standards.
Key Features of High-Alumina Ash Powder Conveyors
High-alumina ash powder conveyors from HeadPowder are equipped with several key features that enhance their performance and usability. These include robust construction materials, such as high-strength alloys and corrosion-resistant coatings, which are essential for withstanding the abrasive properties of high-alumina ash. The conveyors also feature advanced control systems that allow for precise regulation of material flow rates, ensuring consistent and reliable operation. Additionally, the design incorporates dust suppression mechanisms and sealing technologies to minimize environmental impact and maintain a safe working environment. The equipment is further optimized for low maintenance requirements, reducing downtime and operational costs for users.
Design Principles and Operational Mechanisms
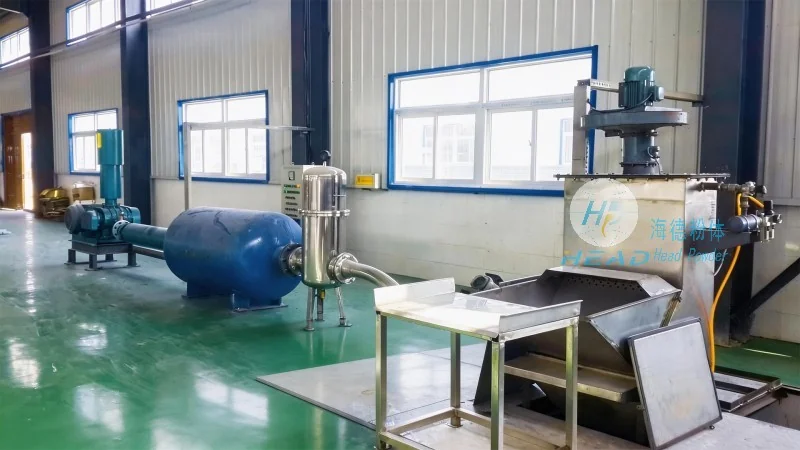
The design principles of high-alumina ash powder conveyors are centered on maximizing efficiency, safety, and durability. The core operational mechanism involves the use of a conveyor belt or screw mechanism to transport the ash powder from the source to the destination. The conveyor system is typically equipped with a hopper or feeding mechanism that ensures a consistent feed of material, preventing blockages and ensuring smooth operation. The design also incorporates features such as adjustable speed controls and material level sensors, which allow operators to monitor and adjust the system in real-time. The use of high-quality bearings and seals further enhances the longevity of the equipment, reducing the need for frequent repairs and replacements.
Benefits and Applications
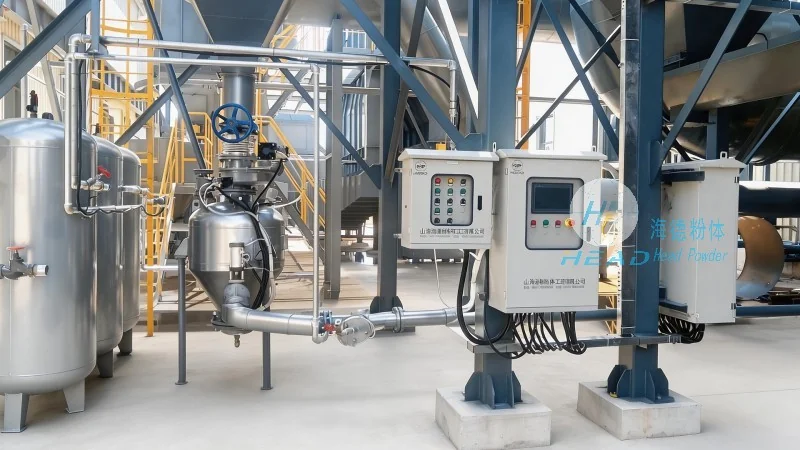
High-alumina ash powder conveyors offer numerous benefits to industries that handle high-alumina ash, including improved material handling efficiency, reduced labor costs, and enhanced safety. These conveyors are commonly used in power plants, cement factories, and other industrial facilities where high-alumina ash is a byproduct of combustion processes. The equipment is designed to handle large volumes of material while maintaining low energy consumption, making it an economical choice for long-term operation. The robust construction and advanced control systems also ensure that the conveyors can operate in harsh environments, such as high-temperature or dusty conditions, without compromising performance.
Conclusion
High-alumina ash powder conveyors are essential equipment for industries dealing with high-alumina ash, providing efficient and reliable transportation solutions. The design principles and operational mechanisms of these systems are carefully engineered to meet the specific demands of the material being transported. With their robust construction, advanced control systems, and low maintenance requirements, these conveyors offer significant advantages over traditional transportation methods. Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted provider of high-quality conveyor systems, delivering solutions that enhance operational efficiency and safety for its clients.