

What is an Organic Salt Powder Conveying Machine? What Are Its Design Principles?
Organic salt powder conveying machines are specialized equipment designed to handle and transport organic salt powders efficiently. These machines are crucial in industries where organic salts are processed, such as chemical manufacturing, food processing, and pharmaceuticals. Understanding the design principles behind these machines is essential for optimizing material handling processes and ensuring operational efficiency.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the development and production of high-quality organic salt powder conveying systems. With a strong commitment to innovation and precision engineering, HeadPowder provides reliable solutions tailored to the unique requirements of organic salt handling applications.
Understanding Organic Salt Powder Conveying Machines
An organic salt powder conveying machine is a mechanical system engineered to transport organic salt powders from one location to another within a processing facility. These machines are designed to handle materials with specific properties, including moisture content, particle size distribution, and flow characteristics. The primary goal is to ensure safe, efficient, and consistent material transfer while minimizing product degradation and operational risks.
Key Design Principles of Organic Salt Powder Conveying Machines
The design of an organic salt powder conveying machine involves several critical principles aimed at optimizing performance and reliability. One of the fundamental principles is the use of appropriate material handling components that are resistant to corrosion and wear, as organic salts can be chemically aggressive. For instance, materials like stainless steel or specialized alloys are commonly used for the construction of conveyor components to withstand the corrosive nature of organic salts.
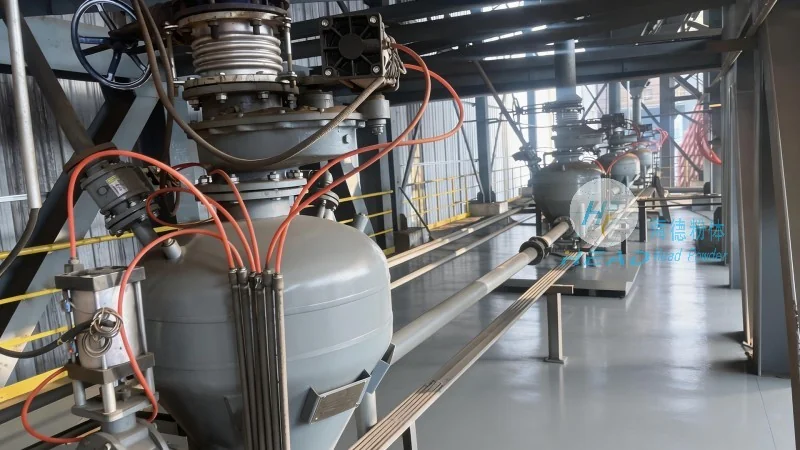
Another crucial design principle is the implementation of airtight and sealed systems to prevent dust emissions and maintain material purity. Organic salt powders are often fine and can create airborne particles, which pose health and safety risks. Therefore, conveying machines are equipped with dust collection systems and sealed housing to contain the material and ensure a clean working environment.
Efficient material flow is also a key design consideration. The machine's design includes features such as hopper design, feed mechanisms, and conveyor belts or screws that are optimized to handle the specific flow characteristics of organic salts. Properly designed hoppers with appropriate angles and feeders help prevent material bridging and ensure a consistent flow rate. The conveyor system, whether it's a screw conveyor, pneumatic conveyor, or belt conveyor, is selected based on the material's bulk density, flowability, and the required conveying distance.
Technical Features and Advantages
Organic salt powder conveying machines from HeadPowder incorporate advanced technical features that enhance their performance and durability. These features include:
- Corrosion-Resistant Construction: Built with high-quality stainless steel or corrosion-resistant alloys to withstand the chemical properties of organic salts, ensuring long-term reliability.
- Sealed and Dust-Proof Design: Equipped with sealed housing and integrated dust collection systems to maintain a clean environment and prevent product contamination.
- Adjustable Flow Control: Advanced control systems allow for precise adjustment of the conveying speed and flow rate, enabling optimal material handling for different processing stages.
- Low Maintenance: Simplified mechanical designs and high-quality components reduce maintenance requirements, minimizing downtime and operational costs.
These technical features contribute to the overall efficiency and safety of organic salt powder conveying operations, making them suitable for various industrial applications.
Applications in Industrial Settings
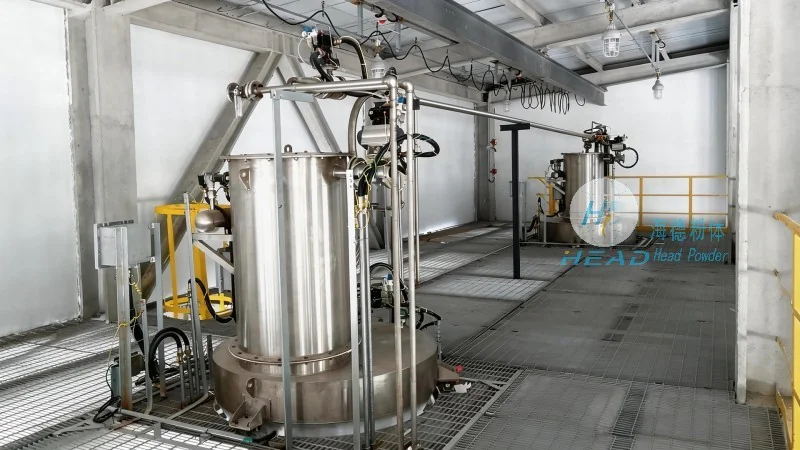
Organic salt powder conveying machines are widely used in several industrial sectors. In the chemical industry, they are employed to transport organic salts used in the production of fertilizers, pharmaceuticals, and other chemical products. In food processing, these machines help handle organic salt powders used as flavor enhancers or preservatives. The pharmaceutical industry also utilizes them for the transport of organic salts used in drug formulations.
In addition to these sectors, organic salt powder conveying machines are essential in manufacturing plants where organic salts are used as raw materials or intermediates. Their ability to handle fine powders with precision ensures that the material is transferred without loss or contamination, maintaining product quality and consistency.
Conclusion
Organic salt powder conveying machines are vital equipment in industries dealing with organic salts, offering efficient and reliable material handling solutions. The design principles, including corrosion resistance, sealed systems, and optimized flow control, ensure that these machines meet the demanding requirements of industrial applications. HeadPowder, with its expertise and commitment to quality, provides top-tier organic salt powder conveying machines that enhance operational efficiency and product safety. By understanding and implementing these design principles, industries can achieve improved productivity and reduced operational risks in their organic salt processing operations.