

What is a Calcined Sand Powder Pneumatic Conveying Equipment? What Are Its Design Principles?
Calcined sand powder pneumatic conveying equipment is a specialized system designed to transport calcined sand powder efficiently and reliably. This equipment is crucial in various industrial applications where the handling of fine powders like calcined sand is required. The system utilizes air as the conveying medium to move the powder from one location to another, offering advantages such as reduced dust generation, improved safety, and enhanced process control. Understanding the components and design principles of this equipment is essential for optimizing material handling processes in industries like construction, foundries, and chemical manufacturing.
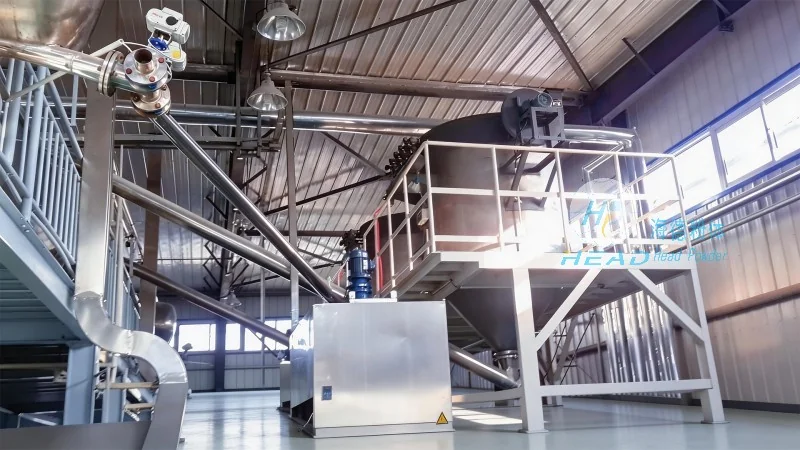
Key Components of the Pneumatic Conveying System
The calcined sand powder pneumatic conveying equipment typically consists of several key components that work together to ensure smooth operation. These components include the hopper, which stores the calcined sand powder; the feeder, which controls the flow of powder into the system; the conveying line, which transports the powder using air pressure; the receiver, which collects the powder at the destination; and the air compressor or blower, which generates the necessary air pressure. Each component plays a vital role in the overall functionality of the system, and proper selection and maintenance are critical for optimal performance.
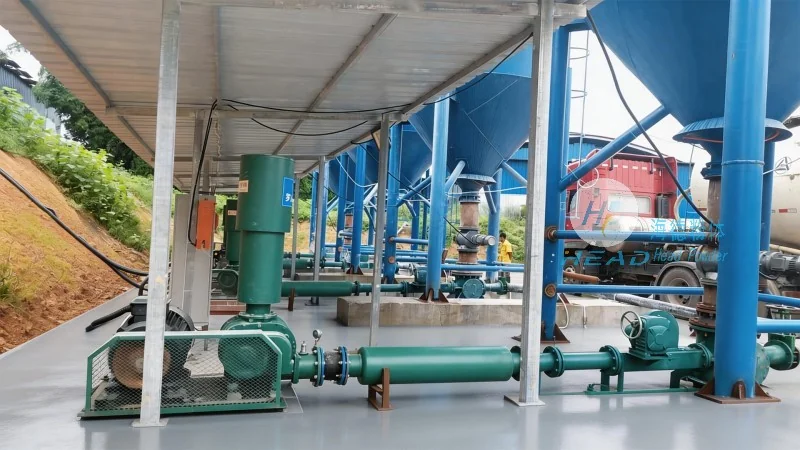
Design Principles and Operational Mechanisms
The design principles of calcined sand powder pneumatic conveying equipment are centered around the efficient use of air to move fine powders. The system operates on the principle of pneumatic transport, where the powder is suspended in a stream of air and carried through the conveying line. The design considers factors such as the particle size, density, and moisture content of the calcined sand, as these properties affect the conveying velocity and pressure requirements. The equipment is engineered to handle the specific characteristics of calcined sand, ensuring that the powder is transported without clogging or degradation. The design also incorporates features like pulse-jet or rotary valves to control the flow and prevent blockages, maintaining consistent performance over time.
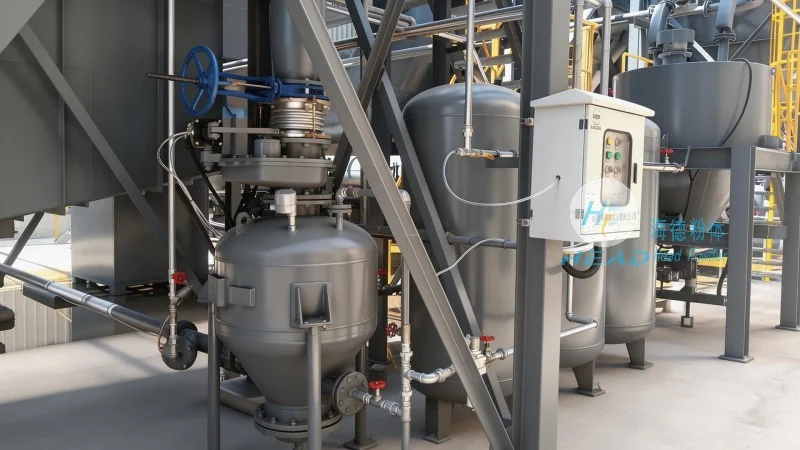
Advantages of Using Pneumatic Conveying for Calcined Sand
Employing pneumatic conveying equipment for calcined sand offers several advantages over traditional methods like belt conveyors or bucket elevators. One of the primary benefits is the reduction in dust exposure, which enhances workplace safety and compliance with environmental regulations. The system also minimizes product contamination, as the enclosed design prevents the powder from coming into contact with external contaminants. Additionally, pneumatic conveying allows for flexible routing of the conveying line, enabling the equipment to be installed in various layouts without the need for complex infrastructure modifications. The system's ability to handle fine powders with high efficiency and low maintenance requirements makes it a preferred choice for industries dealing with calcined sand.
Applications and Industries
The calcined sand powder pneumatic conveying equipment is widely used in various industries that require the handling of calcined sand. In the construction industry, it is used for transporting sand used in concrete production, ensuring consistent quality and reducing material waste. In foundries, the equipment is essential for moving calcined sand used in sand casting processes, improving the efficiency of the casting operations. The chemical industry also utilizes this equipment for handling calcined sand in processes such as filtration and drying. The versatility of the system makes it suitable for a range of applications where fine powder transport is critical.
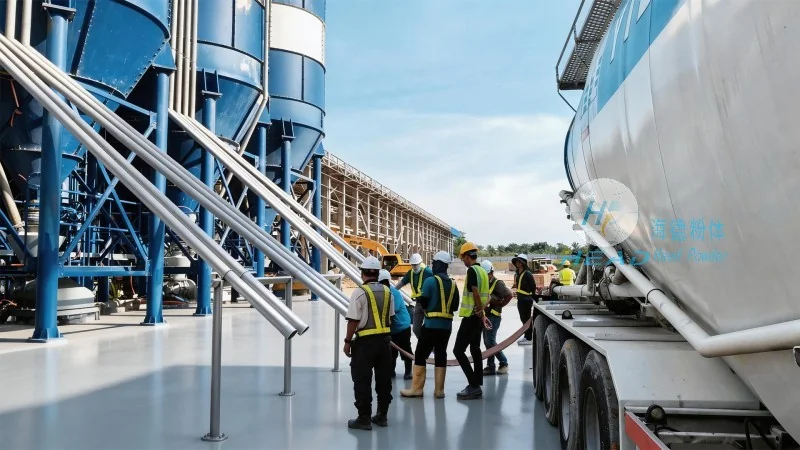
Customization and Integration with Existing Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying equipment, offers customized solutions tailored to the specific needs of clients. The company, based in China, provides equipment that can be integrated seamlessly with existing industrial systems, ensuring minimal disruption to current operations. The customization options include varying the conveying line length, adjusting the air pressure and flow rates, and incorporating additional features such as dust collection systems or material drying units. This flexibility allows clients to optimize the equipment for their unique processes, enhancing overall productivity and efficiency. The company's expertise in designing and manufacturing calcined sand powder pneumatic conveying equipment ensures that clients receive high-quality, reliable systems that meet their operational requirements.