

What is a High-Pressure Bin Pump Powder Pneumatic Conveying System? And What Are Its Design Principl
High-pressure bin pump powder pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transport of bulk powders across industrial settings. These systems are integral to modern material handling operations, offering a flexible and low-maintenance approach to moving materials like chemicals, pharmaceuticals, food ingredients, and mining ores. The core of such a system is the high-pressure bin pump, which acts as the driving force behind the pneumatic conveying process, enabling powders to be moved through a network of pipes under controlled pressure. This technology has become increasingly popular due to its ability to handle a wide variety of powder characteristics, including abrasive, corrosive, or sensitive materials, while maintaining product integrity and operational efficiency.
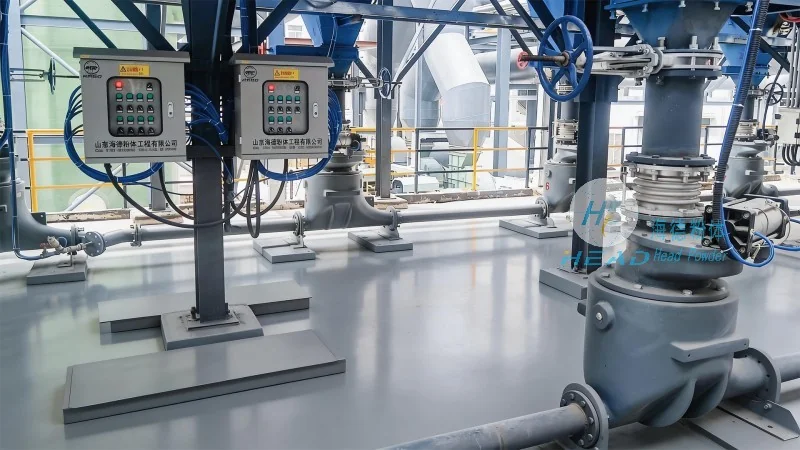
Key Components and the Fundamental Working Principle
The design of a high-pressure bin pump powder pneumatic conveying system comprises several essential components that work in unison to facilitate material transport. The primary components include a storage bin or hopper for holding the bulk powder, a high-pressure pump that generates the necessary pressure to move the material, a pipeline system for conveying the powder, and a control system for regulating flow and pressure. The working principle is rooted in pneumatic conveying, where the powder is suspended in a stream of air or gas and propelled through the pipeline. The high-pressure pump creates a pressure differential that forces the powder from the storage bin to the discharge point. This process is typically continuous, allowing for consistent and controlled material transfer. The pump may be a positive displacement type, such as a rotary lobe or piston pump, or a centrifugal pump, depending on the specific requirements of the powder being handled.
Advantages Over Traditional Conveying Methods
Compared to conventional methods like belt conveyors or screw conveyors, high-pressure bin pump systems offer several distinct advantages. One of the most significant benefits is the ability to handle abrasive and corrosive powders without causing wear or damage to the equipment. The enclosed pipeline system also helps in maintaining product purity and preventing contamination, which is critical in industries like pharmaceuticals and food processing. Additionally, these systems are highly flexible, allowing for changes in the conveying route or capacity without major modifications. They also require less floor space compared to other bulk handling solutions, making them suitable for installations with limited space. The low maintenance requirements and energy efficiency further enhance their appeal, as they can operate with minimal downtime and lower operational costs. Furthermore, the system's ability to handle variations in powder feed, such as changes in moisture content or bulk density, ensures consistent performance and reduces the risk of blockages or system failures.
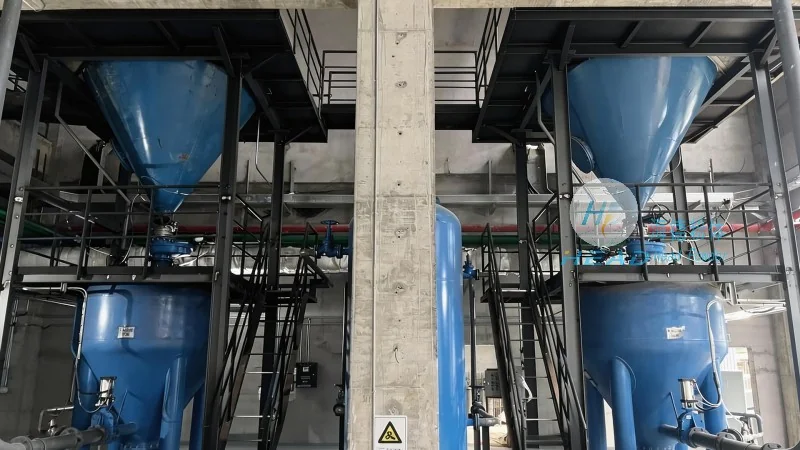
Design Principles and Engineering Considerations
The design of a high-pressure bin pump powder pneumatic conveying system involves careful consideration of several engineering principles to ensure safety, efficiency, and reliability. The selection of the appropriate pump type depends on the specific characteristics of the powder, such as particle size, density, and flowability. For example, some powders may require a positive displacement pump to maintain a consistent flow rate, while others may be better suited for a centrifugal pump for handling larger volumes. The pipeline design is also critical, as it must be able to withstand the high pressures generated by the pump and prevent leaks or blockages. The use of appropriate materials for the pipeline, such as stainless steel or special alloys, is essential to prevent corrosion and ensure long-term durability. The control system plays a vital role in regulating the pressure and flow rate, ensuring that the system operates within safe limits and prevents overpressure or underflow conditions. Additionally, the system must be designed to handle variations in powder feed, such as changes in moisture content or bulk density, to maintain consistent performance. Safety features, including pressure relief valves and emergency shut-off mechanisms, are also incorporated to protect the system and personnel from potential hazards.
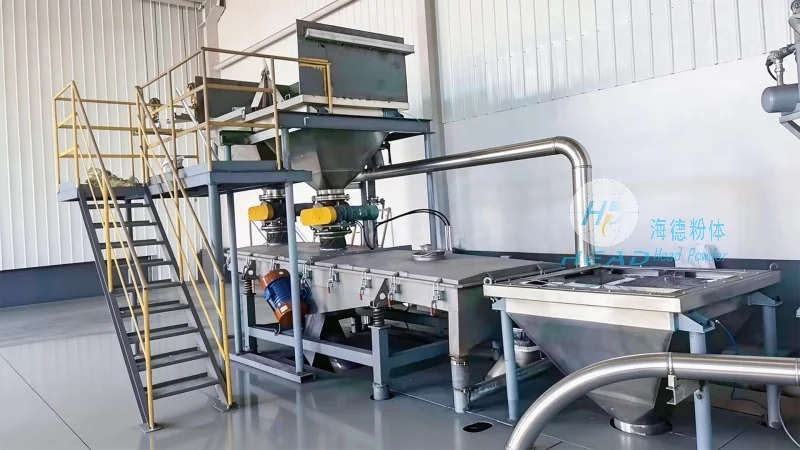
Applications and Industries
High-pressure bin pump powder pneumatic conveying systems are used in a wide range of applications across various industries. In the chemical industry, they are used to transport raw materials and finished products, such as powders for pharmaceuticals, fertilizers, and plastics. The food processing industry utilizes these systems for handling ingredients like flour, sugar, and spices, ensuring that the products remain fresh and uncontaminated. The mining industry also benefits from these systems for transporting ore and other bulk materials from the mine to processing facilities. Additionally, in the pharmaceutical and biotech sectors, the enclosed and sterile design of the system is essential for maintaining product purity and meeting regulatory requirements. The versatility of these systems makes them suitable for any application where bulk powder handling is required, providing a reliable and efficient solution for material transport. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, specialize in designing and manufacturing such systems, offering customized solutions tailored to the specific needs of their clients.
Conclusion
High-pressure bin pump powder pneumatic conveying systems represent a cutting-edge technology in bulk material handling, offering a reliable and efficient solution for transporting a wide range of powders. By understanding the key components, working principles, and design considerations, industries can leverage these systems to improve operational efficiency, reduce costs, and maintain product quality. As the demand for advanced material handling solutions continues to grow, high-pressure bin pump systems remain a popular choice due to their flexibility, durability, and ability to handle challenging materials. With companies like Shandong HeadPowder Engineering Co., Ltd. providing expertise and customized solutions, businesses can ensure that their material transport needs are met with the highest standards of performance and reliability.