For industrial applications that require efficient and reliable handling of bulk materials within silos, the design and operation of silo bulk material conveyors play a crucial role. These systems are engineered to ensure seamless material flow from storage silos to processing or packaging areas, minimizing downtime and optimizing operational efficiency. Understanding the working principle and key features of such conveyors is essential for selecting the right equipment for specific industrial needs.
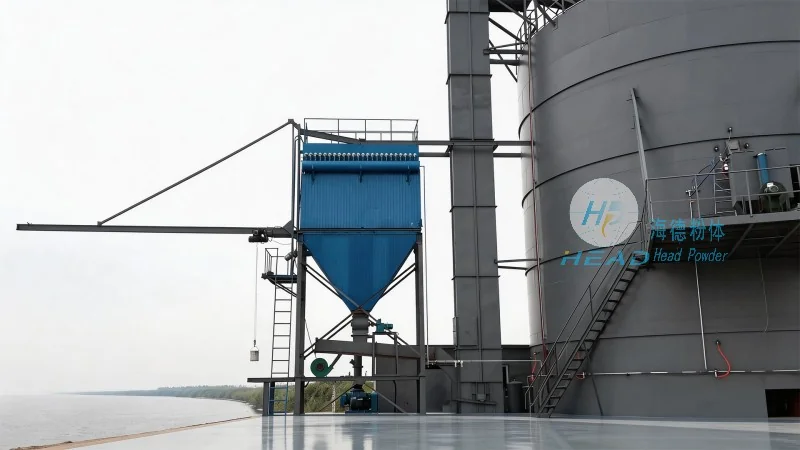
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, manufacturing, and supply of advanced bulk material handling solutions. With a focus on precision engineering and robust construction, their conveyors are tailored to meet the demands of various industries, including food processing, chemical manufacturing, and pharmaceutical production. The company’s headquarters is located in Shandong, China, where state-of-the-art facilities ensure the production of high-quality equipment that adheres to international standards.
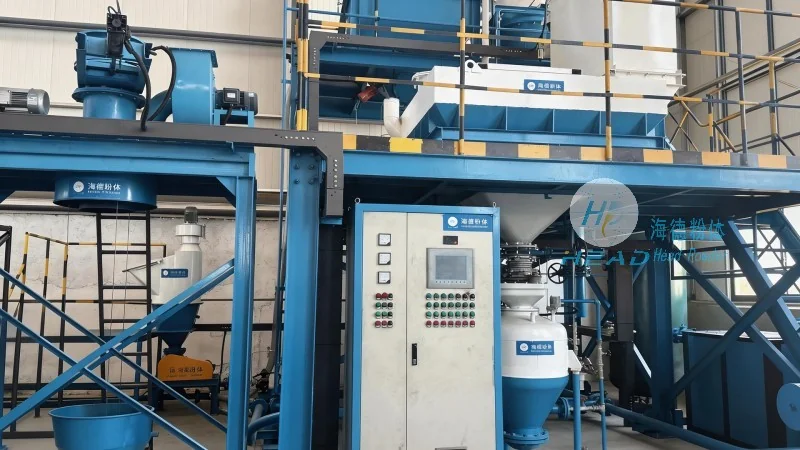
The core working principle of a silo bulk material conveyor involves the use of mechanical components to transport powders or granules from a silo to a discharge point. Typically, these systems consist of a hopper or feeder that draws material from the silo, a conveyor mechanism (such as a screw, belt, or pneumatic system), and a control system that regulates the flow rate. The process begins when the silo’s material is drawn into the feeder, where it is then conveyed to the desired location. The conveyor’s speed and direction are controlled by a programmable logic controller (PLC) or similar system, allowing for precise adjustment based on operational requirements. This mechanism ensures that material is transported consistently, preventing blockages and maintaining a steady flow rate. The design of the conveyor, including the type of screw or belt used, is tailored to the characteristics of the material being handled—such as particle size, moisture content, and flowability—to optimize performance.
Shandong HeadPowder Engineering Co., Ltd.’s silo bulk material conveyors are distinguished by several key features that enhance their functionality and reliability. One of the primary features is the robust construction, which includes high-quality materials such as stainless steel or corrosion-resistant alloys, ensuring durability and resistance to wear and tear. This is particularly important for handling abrasive or corrosive materials, as it prevents equipment failure and extends the lifespan of the system. Another critical feature is the variable speed control, which allows operators to adjust the conveyor speed based on the material’s flow characteristics. This flexibility ensures that the system can handle a wide range of materials, from free-flowing powders to cohesive granules, without compromising performance. Additionally, the conveyors are equipped with advanced monitoring systems, including sensors that detect blockages or overloads, providing real-time feedback to the control system. This feature enhances safety and operational efficiency by preventing accidents and reducing downtime. The compact design of the conveyors also contributes to their effectiveness, as they can be easily integrated into existing silo structures without requiring significant modifications to the facility. This makes them a cost-effective solution for industries looking to upgrade their material handling processes.
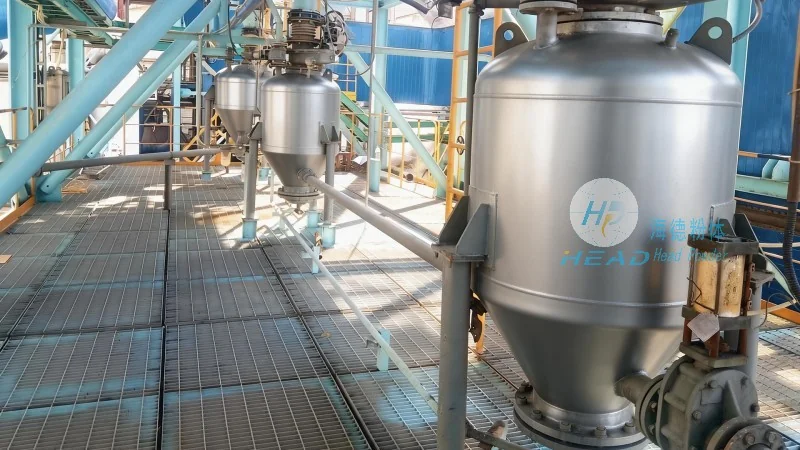
The implementation of silo bulk material conveyors offers numerous benefits for industrial operations. Firstly, they improve material flow efficiency by reducing the time required to transfer bulk materials from storage to processing areas. This leads to increased productivity and reduced labor costs, as manual handling is minimized. Secondly, the consistent flow rate provided by these conveyors ensures that downstream processes, such as mixing or packaging, operate smoothly without interruptions. This stability is crucial for maintaining product quality and meeting production targets. Thirdly, the automated control systems reduce the risk of human error, enhancing safety in the workplace. The ability to monitor and adjust the conveyor in real-time also allows for better inventory management, as operators can track the material levels in the silo and adjust the discharge rate accordingly. Furthermore, the durability and reliability of the equipment reduce maintenance costs over time, as fewer breakdowns occur and repairs are minimized. Overall, the use of silo bulk material conveyors contributes to a more efficient, cost-effective, and safe industrial operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan City, Shandong Province, China

telephone
WeChatconsult
top