

[W]Working Principle and Features of Coal and Coke Powder Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for coal and coke powders. These systems are engineered to efficiently transport bulk powders over long distances with minimal maintenance and operational costs.
Working Principle of Coal and Coke Powder Pneumatic Conveying Systems
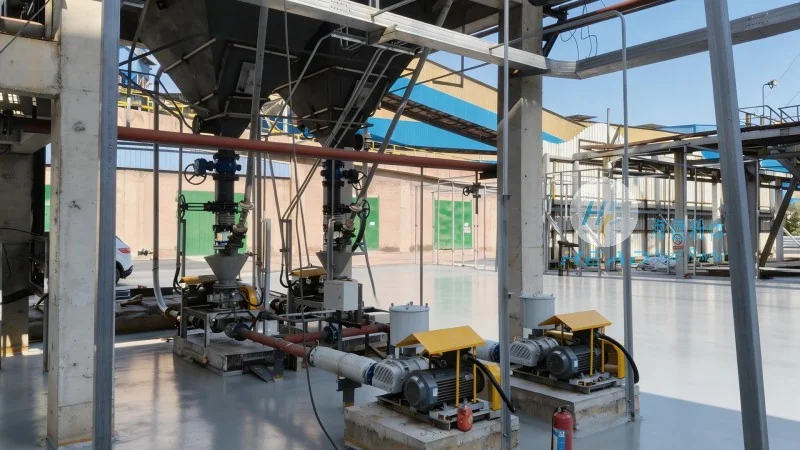
The working principle of a coal and coke powder pneumatic conveying system involves the use of a pressurized air stream to move particulate materials through a pipeline network. The system typically consists of a material feed hopper, a positive displacement blower or a rotary lobe pump that generates the necessary air pressure, and a series of pipelines that guide the material from the source to the destination. As the material is introduced into the system, it is entrained by the high-velocity air stream, which carries it through the pipeline. The air and material mixture is then separated at the discharge point, with the air being recirculated back to the blower and the material being discharged into the receiving container. This process ensures a continuous and controlled flow of material, minimizing downtime and maximizing throughput.
Key Features and Advantages of HeadPowder's Systems
HeadPowder's coal and coke powder pneumatic conveying systems are distinguished by several key features that enhance performance and reliability. One of the primary advantages is the high efficiency in material transport, as the systems can move large volumes of powder over significant distances with minimal energy consumption. The use of positive displacement blowers or rotary lobe pumps ensures consistent air pressure, which is critical for maintaining the flow of abrasive materials like coal and coke. Additionally, the systems are designed with wear-resistant components, such as lined pipelines and hardened pump parts, to withstand the corrosive and abrasive nature of the powders, reducing the need for frequent replacements and maintenance.
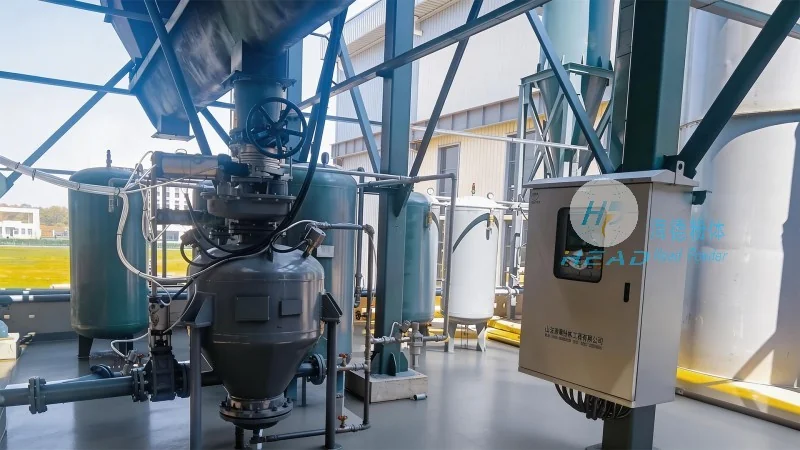
Another notable feature is the reduced dust generation compared to traditional mechanical conveying methods. The enclosed pipeline system prevents dust from escaping into the environment, improving workplace safety and compliance with environmental regulations. This is particularly important in industries where dust control is a regulatory requirement. The systems also offer flexibility in layout, allowing for integration into existing industrial facilities or new plant designs without major structural modifications. This adaptability makes them suitable for a wide range of applications, from small-scale operations to large-scale industrial plants.
Customization and Engineering Expertise
HeadPowder's engineering team provides tailored solutions to meet the specific needs of each client. By working closely with clients, the company can design systems that address unique challenges such as material variability, distance constraints, and environmental regulations. The company's expertise in material handling and process engineering allows for the development of customized solutions that optimize performance and cost-effectiveness. For example, the system can be configured to handle different particle sizes, moisture contents, or bulk densities, ensuring that the material is transported safely and efficiently. This level of customization ensures that the system meets the exact requirements of the client's operation, leading to improved productivity and reduced operational costs.
Reliability and Maintenance
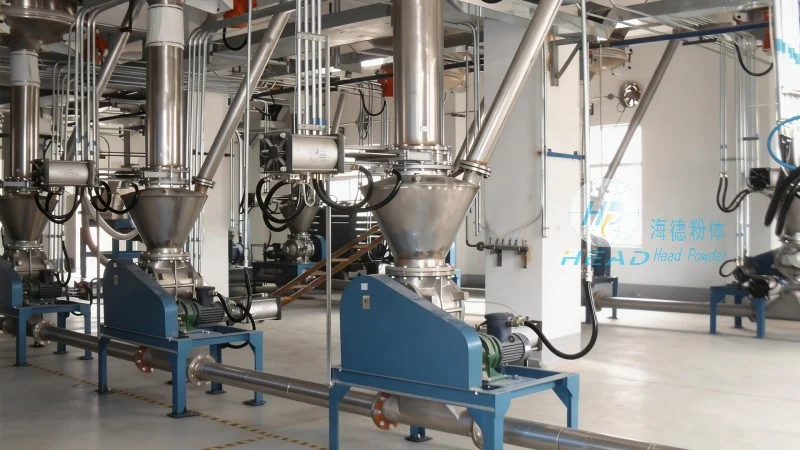
Reliability is a top priority in the design of HeadPowder's coal and coke powder pneumatic conveying systems. The use of high-quality components and robust construction ensures that the systems operate consistently over long periods with minimal downtime. The air recirculation system not only reduces energy consumption but also minimizes the wear on the blower and other components, extending their service life. Regular maintenance is straightforward, with easy access to components for inspection and replacement. The company provides comprehensive maintenance services and spare parts availability, ensuring that clients can maintain the system's performance and longevity. This focus on reliability and maintenance makes the systems a cost-effective choice for industries that require continuous operation and minimal interruptions.
Conclusion
In summary, the coal and coke powder pneumatic conveying systems offered by Shandong HeadPowder Engineering Co., Ltd. represent a reliable and efficient solution for bulk material transport in industrial applications. By leveraging advanced engineering and high-quality components, these systems provide consistent performance and low maintenance, making them a preferred choice for industries that require safe and effective handling of coal and coke powders. The systems are designed to meet the specific needs of each client, ensuring optimal performance and cost-effectiveness in a variety of industrial settings.