

The Working Principle and Features of Dust-Free Closed Powder Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free, airtight powder pneumatic conveying systems. These systems are engineered to efficiently transport powders and bulk materials in a controlled, enclosed environment, ensuring minimal contamination and optimal operational safety. This article delves into the core working principle and key features of such equipment, highlighting how they address the challenges of traditional open-air powder handling.
Understanding the Working Principle of Dust-Free Pneumatic Conveying Systems
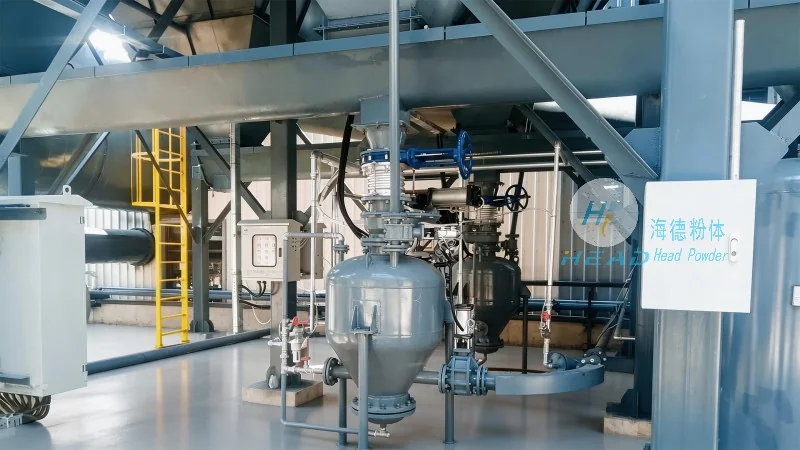
The fundamental principle behind dust-free, closed powder pneumatic conveying is the use of pressurized or vacuum air to move material through a sealed pipeline system. Unlike traditional open systems that expose powders to the air, these advanced machines maintain an airtight environment, preventing dust emissions and cross-contamination. The process typically involves several key components: a material hopper for storage, a conveying line with sealed connections, and a control system to regulate air flow and pressure. When the system is activated, compressed air is introduced into the pipeline, creating a flow that draws or pushes the powder from the hopper to the discharge point. The sealed design ensures that all material is contained within the system, making it ideal for applications requiring high purity and environmental compliance.
Key Features of Dust-Free Closed Powder Pneumatic Conveying Equipment
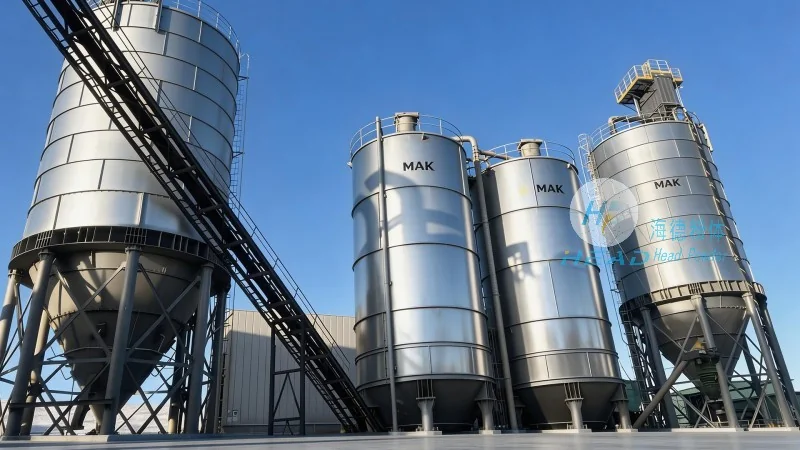
HeadPowder's dust-free pneumatic conveying systems are distinguished by several critical features that enhance performance and reliability. Firstly, the airtight construction minimizes dust leakage, which is crucial for maintaining product quality and adhering to industrial hygiene standards. This design also reduces the risk of material degradation caused by exposure to moisture or air, extending the shelf life of sensitive powders. Secondly, the systems offer high efficiency in material transport, with the ability to handle a wide range of powder types, from fine powders to bulk solids, without clogging or blockages. The adjustable air pressure and flow rate settings allow for precise control over the conveying speed, ensuring consistent and uniform material delivery. Additionally, the enclosed nature of the system enhances safety by preventing the release of hazardous dust particles into the workplace, thereby reducing health risks for operators. The robust construction and durable materials used in the equipment ensure long-term durability and low maintenance requirements, making them cost-effective solutions for industrial applications.
Applications and Benefits in Industrial Settings
Dust-free, closed powder pneumatic conveying equipment from HeadPowder is widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and cement production. In the pharmaceutical industry, for example, the sealed system prevents contamination of active ingredients, ensuring product safety and compliance with regulatory standards. In food processing, it maintains the purity of ingredients and prevents cross-contamination between different products. The systems also contribute to environmental sustainability by reducing waste and minimizing the need for additional cleaning or disposal of dust. The benefits extend to operational efficiency, as the enclosed design reduces downtime caused by cleaning and maintenance, while the precise control over material flow optimizes production processes. Overall, these systems provide a reliable and efficient solution for handling powders in a controlled environment, supporting the needs of modern industrial operations.
Conclusion and Company Overview
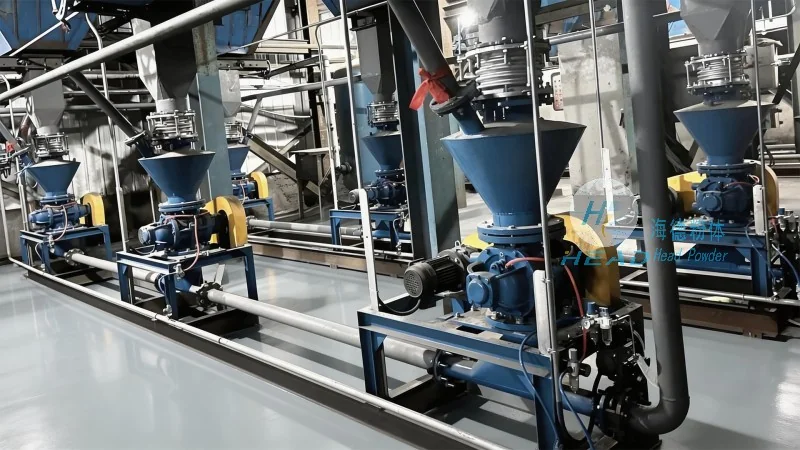
HeadPowder Engineering Co., Ltd., based in Shandong, China, is dedicated to providing innovative and high-quality dust-free pneumatic conveying solutions. By leveraging advanced engineering and rigorous quality control, the company ensures that its equipment meets the highest standards of performance and reliability. The working principle and features of these systems, as outlined above, demonstrate their effectiveness in addressing the challenges of traditional powder handling while offering significant advantages in efficiency, safety, and environmental compliance. For industries requiring precise and controlled material transport, HeadPowder's dust-free, airtight pneumatic conveying equipment is a superior choice, supporting the seamless operation of modern production processes.