

Principles and Application Scenarios of Dust-Free and Airtight Powder Handling Systems
HeadPowder, a leading provider in the field, specializes in the design and implementation of advanced dust-free and airtight powder handling systems. These systems are engineered to ensure safe, efficient, and contamination-free transfer of powders in various industrial applications. The core principle behind such systems lies in creating a sealed environment that prevents the release of dust particles into the surrounding air, thereby maintaining a clean and safe working environment.
Core Principles of the Powder Handling System
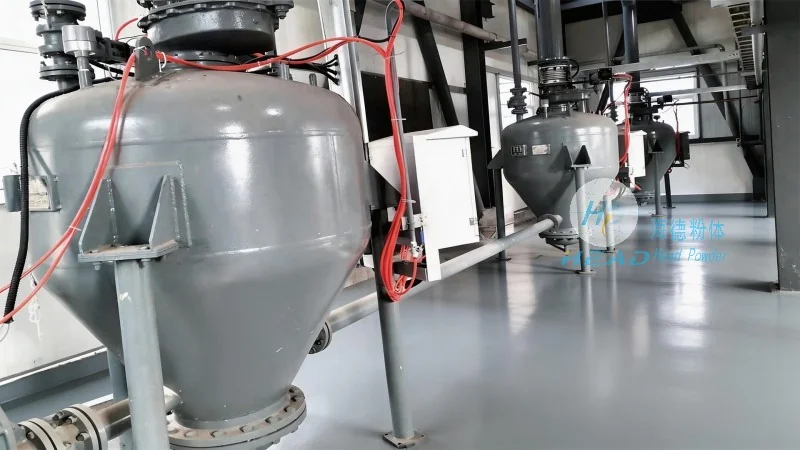
The fundamental principle of a dust-free and airtight powder handling system is the creation of a closed loop or sealed pathway for powder movement. This is achieved through the integration of components such as rotary valves, pneumatic conveying lines, and dust collection units. The system operates by drawing powder from a storage silo or hopper into a conveying line under controlled pressure, ensuring that all powder particles remain contained within the system. The absence of open hoppers or unsealed transfer points is crucial to prevent dust emissions and maintain product purity. Additionally, the system incorporates filtration and air purification mechanisms to further enhance the containment of particulate matter, ensuring compliance with industrial hygiene standards and environmental regulations.
Key Components and Their Functions
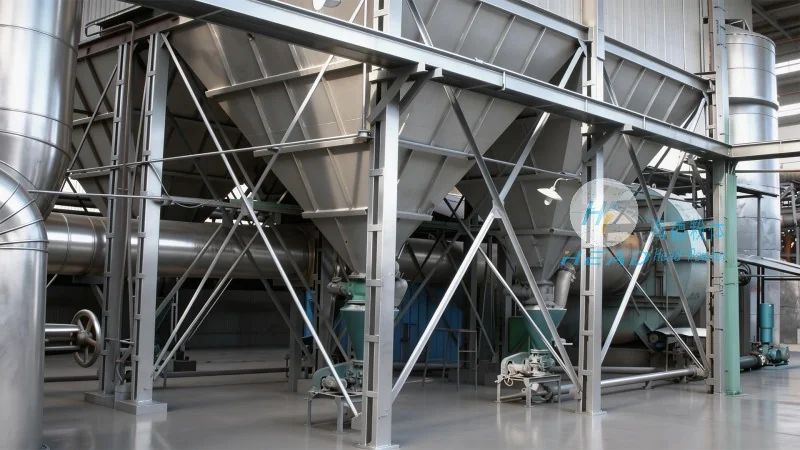
Several critical components work in tandem to ensure the effective operation of the powder handling system. The primary components include: storage silos or hoppers equipped with airtight lids and level indicators; rotary airlocks or valves that control the flow of powder into and out of the conveying system; pneumatic conveying lines that use compressed air to transport powder from one location to another; and dust collection systems such as cyclones or bag filters that capture any particles that may escape the main system. Each component is designed to minimize the risk of dust leakage and to maintain the integrity of the powder being handled. For instance, the rotary airlock valve acts as a seal between the storage vessel and the conveying line, preventing backflow and ensuring that only a controlled amount of powder is released at a time. The pneumatic conveying lines are typically made of materials resistant to corrosion and abrasion, such as stainless steel or polyethylene, to withstand the abrasive nature of many powders. The dust collection units are strategically placed to capture any particles that may be generated during the transfer process, thereby preventing contamination of the surrounding environment and ensuring that the powder remains in a clean state.
Application Scenarios and Industry Use Cases
The dust-free and airtight powder handling systems developed by HeadPowder are applicable across a wide range of industries where powder handling is critical. In the pharmaceutical industry, these systems are essential for handling active pharmaceutical ingredients (APIs) and excipients, as even a small amount of contamination can affect the efficacy and safety of the final product. The systems ensure that the powders remain sterile and free from particulate matter, which is crucial for maintaining product quality and regulatory compliance. In the food and beverage industry, similar systems are used to handle ingredients such as flour, sugar, and spices, ensuring that the products remain free from dust and contaminants that could affect taste or safety. The chemical industry also benefits from these systems when handling powders such as chemicals, pigments, and catalysts, as the sealed environment prevents chemical reactions with the air and maintains the purity of the materials. Additionally, in the manufacturing of cosmetics and personal care products, the systems are used to handle powders like talc, silica, and other additives, ensuring that the final products are free from impurities and meet stringent quality standards. Each of these applications leverages the core principles of the system to maintain product integrity and operational safety.
Advantages of Implementing Dust-Free and Airtight Systems
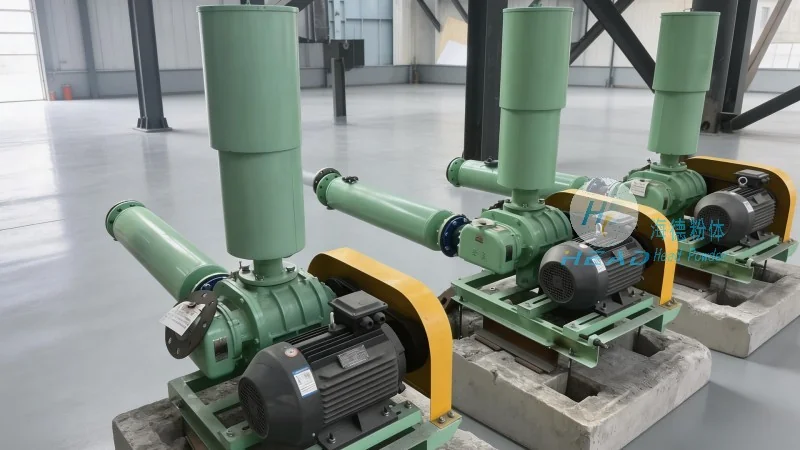
Adopting a dust-free and airtight powder handling system offers numerous advantages for industrial operations. Firstly, it significantly improves workplace safety by reducing the exposure of personnel to airborne dust particles, which can cause respiratory issues and other health problems. The sealed environment also minimizes the risk of dust explosions, which are a major concern in many powder handling processes. Secondly, the system enhances product quality by preventing contamination from external sources and maintaining the purity of the powder throughout the handling process. This is particularly important in industries where product consistency and regulatory compliance are paramount. Thirdly, the system improves operational efficiency by reducing downtime caused by dust-related maintenance and cleaning. The sealed design also reduces the need for frequent cleaning of equipment and the surrounding area, as the risk of dust accumulation is minimized. Furthermore, the system can lead to cost savings by reducing the need for additional filtration and cleaning equipment, as well as by minimizing waste due to product contamination. Overall, the implementation of these systems provides a comprehensive solution to the challenges associated with powder handling, ensuring both safety and efficiency in industrial operations.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable company specializing in the design, manufacturing, and installation of advanced dust-free and airtight powder handling systems. With a focus on innovation and adherence to industry standards, HeadPowder has established itself as a trusted partner for businesses seeking to enhance their powder handling processes. The company's systems are tailored to meet the specific needs of various industries, ensuring that clients receive customized solutions that address their unique challenges. By leveraging the core principles of sealed environments and efficient powder transfer, HeadPowder's systems provide a reliable and effective solution for maintaining product quality and operational safety. As the demand for clean and efficient powder handling continues to grow, HeadPowder remains committed to providing cutting-edge solutions that meet the evolving needs of the industry.