

Principle and Working Scene Characteristics of Negative Pressure Dilute Phase Powder Conveying Syste
HeadPowder, a leading provider in the field of powder handling technology, specializes in advanced conveying solutions that ensure efficient and reliable transport of bulk powders. This article delves into the fundamental principles of negative pressure dilute phase powder conveying systems, exploring their operational mechanisms and the specific working environments where they excel.
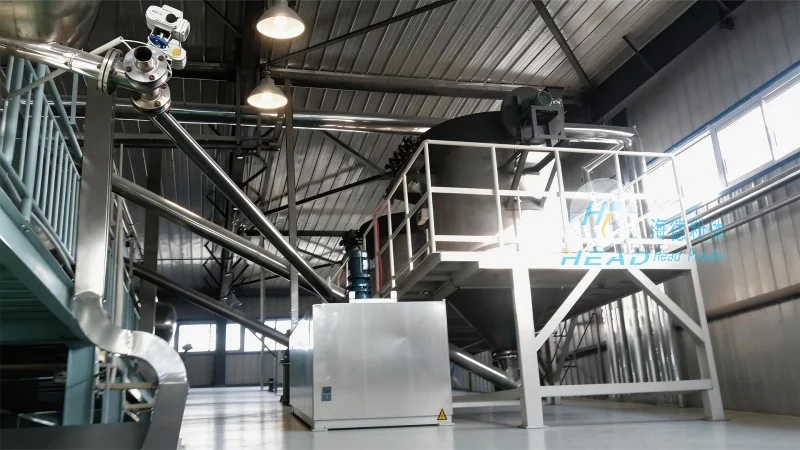
Core Principles of Negative Pressure Dilute Phase Conveying
The negative pressure dilute phase conveying system operates on the principle of creating a low-pressure environment within the conveying line, which draws the powder material from the source and transports it to the destination. Unlike positive pressure systems that push material through a pipeline, negative pressure systems utilize suction to move the powder, often with the assistance of a carrier gas such as air or nitrogen. This approach minimizes the risk of dust emissions and ensures a cleaner, more controlled transport process. The system typically consists of a suction fan, a conveying line, a material feed hopper, and a discharge unit. The suction fan generates the negative pressure, while the carrier gas flows through the line, carrying the powder particles in a dilute phase—meaning the powder is dispersed as individual particles rather than forming a dense plug. This dilute phase ensures efficient gas-particle interaction, enhancing the conveying efficiency and reducing the likelihood of blockages.
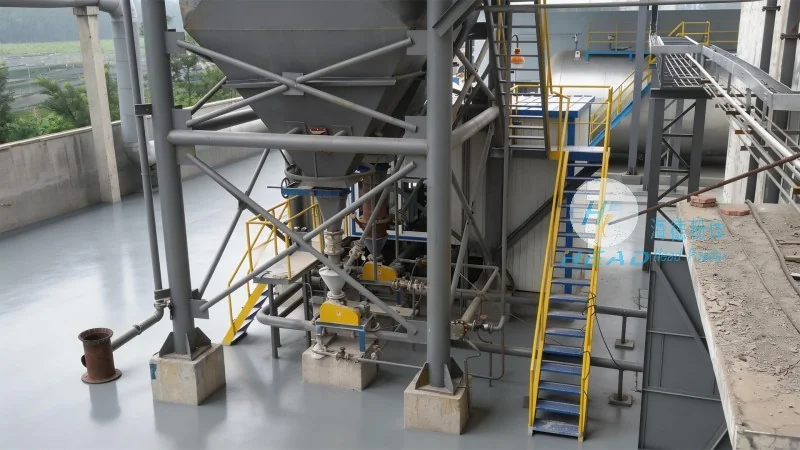
Working Scene Characteristics and Applications
Negative pressure dilute phase powder conveying systems are particularly well-suited for applications where dust control and material cleanliness are critical. These systems are commonly employed in industries such as pharmaceuticals, food processing, and chemical manufacturing, where the transport of powders like active pharmaceutical ingredients (APIs), food additives, or fine chemicals requires stringent contamination control. The low-pressure operation also makes these systems ideal for handling sensitive materials that could be damaged by high-pressure forces or for applications where the receiving end of the system is at a lower elevation than the source, as the negative pressure can effectively pull the material uphill without the need for additional mechanical assistance.
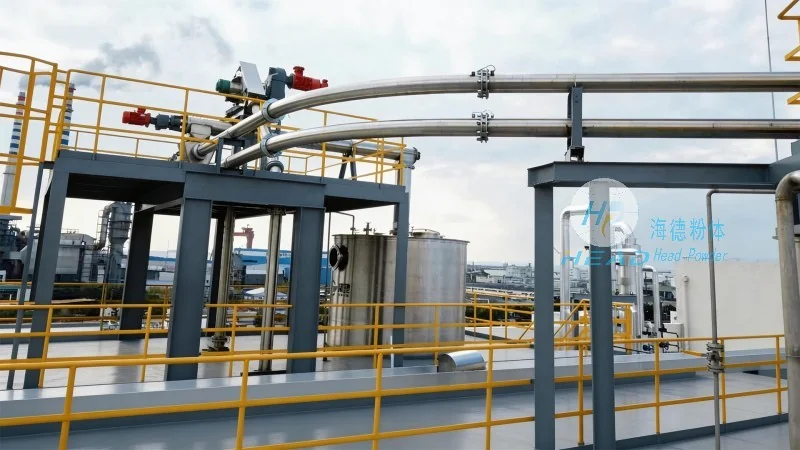
Advantages of Negative Pressure Dilute Phase Conveying
One of the key advantages of negative pressure dilute phase conveying is its superior dust containment. By operating under negative pressure, the system draws air and powder particles into the conveying line, preventing dust from escaping into the surrounding environment. This is crucial in industries where air quality regulations are strict or where product purity must be maintained. Additionally, the dilute phase operation reduces the risk of material buildup and blockages, as the powder particles are kept in suspension by the carrier gas. This leads to higher conveying efficiency and lower maintenance requirements compared to dense phase or positive pressure systems. Another advantage is the flexibility in system design, as negative pressure systems can be easily integrated with existing infrastructure, and they can handle a wide range of powder types, from fine powders with low bulk density to coarse powders with higher bulk density.
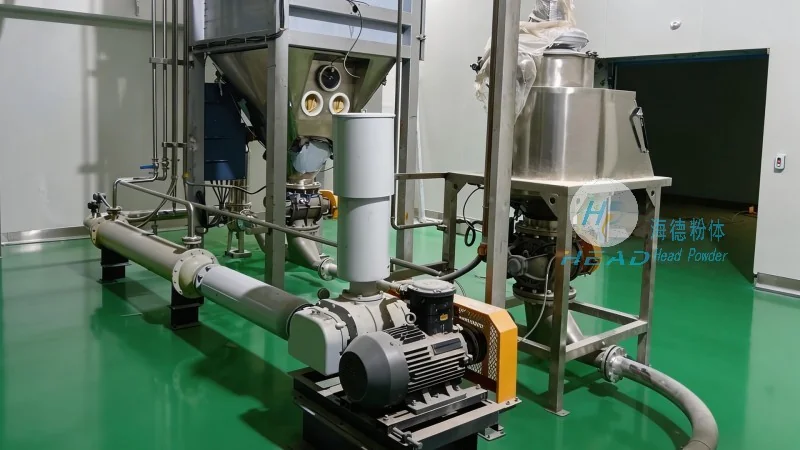
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, with its headquarters in Shandong, China, is a reputable engineering company dedicated to developing and manufacturing advanced powder handling solutions. The company specializes in customizing negative pressure dilute phase conveying systems to meet the specific needs of various industries, ensuring optimal performance and reliability. With a focus on innovation and quality, HeadPowder provides comprehensive support, from system design and installation to maintenance and after-sales service, helping clients achieve efficient and safe powder transport in their operations.