

Principles and Application Scenarios of Automatic Quantitative Powder Transport Systems
Automatic quantitative powder transport systems represent a critical advancement in industrial material handling, offering precise control and efficient operation for various powder processing applications. These systems are designed to handle a wide range of powders, from fine chemicals to bulk materials, ensuring accurate dosing and reliable transport. The core of such systems lies in their ability to integrate advanced technology with practical engineering solutions, addressing the unique challenges of powder handling in different industrial settings.
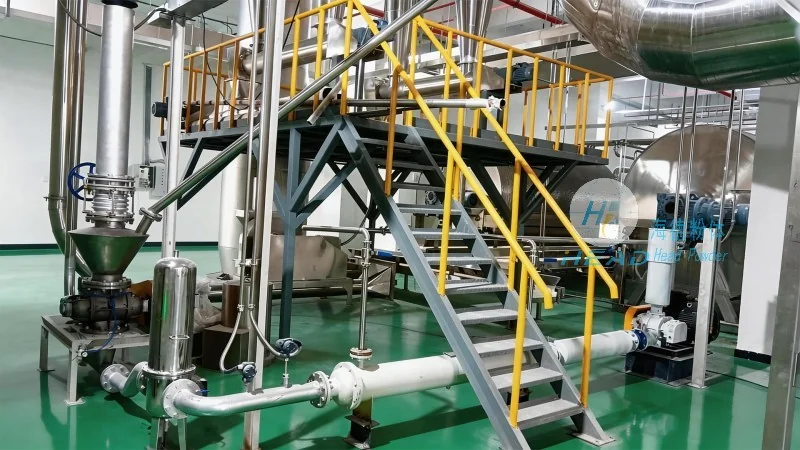
Core Principles of Automatic Quantitative Powder Transport Systems
The fundamental principle behind automatic quantitative powder transport systems is the precise measurement and controlled delivery of powder materials. This is achieved through a combination of sensors, control mechanisms, and mechanical components that work in tandem to maintain accuracy and consistency. Key components typically include powder feeders, conveyors, and dosing mechanisms, each optimized to handle specific powder characteristics. The systems often employ feedback control loops to adjust the flow rate in real-time, ensuring that the output matches the set target parameters. This precision is crucial for applications where even minor variations can impact product quality or process efficiency.
Key Features and Technical Advantages
Modern automatic quantitative powder transport systems are equipped with several advanced features that enhance their performance and reliability. One of the most significant advantages is the integration of digital control systems, which allow for easy programming and adjustment of dosing parameters. This flexibility enables users to adapt the system to different powder types and processing requirements without extensive reconfiguration. Additionally, many systems incorporate safety features such as overload protection and material detection sensors, ensuring safe operation and preventing equipment damage. The use of high-quality materials in construction, such as stainless steel and corrosion-resistant components, further contributes to the durability and longevity of the equipment. These technical advancements collectively contribute to improved productivity and reduced operational costs in industrial settings.
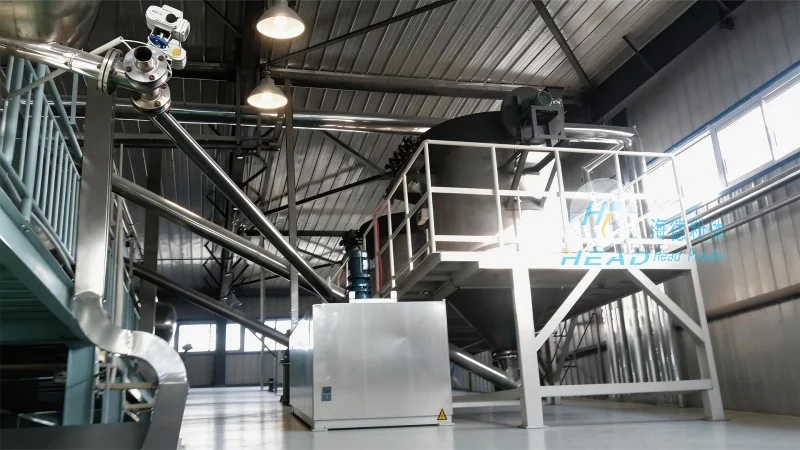
Application Scenarios and Industry Use Cases
Automatic quantitative powder transport systems find widespread application across multiple industries, each with distinct requirements for powder handling. In the pharmaceutical industry, for example, these systems are essential for the precise dosing of active pharmaceutical ingredients (APIs) and excipients, ensuring compliance with stringent quality standards. The food and beverage sector also relies on such systems for handling ingredients like flour, sugar, and spices, where consistency is vital for product quality and consumer safety. In the chemical and petrochemical industries, these systems are used for transporting bulk chemicals and reagents, where accurate measurement is critical for reaction control and process optimization. Furthermore, in the manufacturing of cosmetics and personal care products, automatic powder transport systems help maintain the purity and consistency of raw materials, contributing to the final product's quality. Each application leverages the system's ability to deliver consistent, repeatable dosing, which is essential for meeting industry standards and customer expectations.
Operational Efficiency and Process Integration
The integration of automatic quantitative powder transport systems into existing production lines significantly enhances operational efficiency. By automating the powder handling process, these systems reduce the need for manual intervention, minimizing human error and labor costs. The consistent and accurate dosing provided by the systems ensures that downstream processes, such as mixing or compounding, operate smoothly without interruptions or quality issues. This leads to improved overall process reliability and reduced downtime. Additionally, the systems can be integrated with other industrial automation equipment, such as PLCs (Programmable Logic Controllers) and SCADA (Supervisory Control and Data Acquisition) systems, allowing for centralized monitoring and control. This integration enables real-time data collection and analysis, facilitating process optimization and predictive maintenance. The result is a more streamlined and efficient production environment, where material handling is a seamless part of the overall workflow.
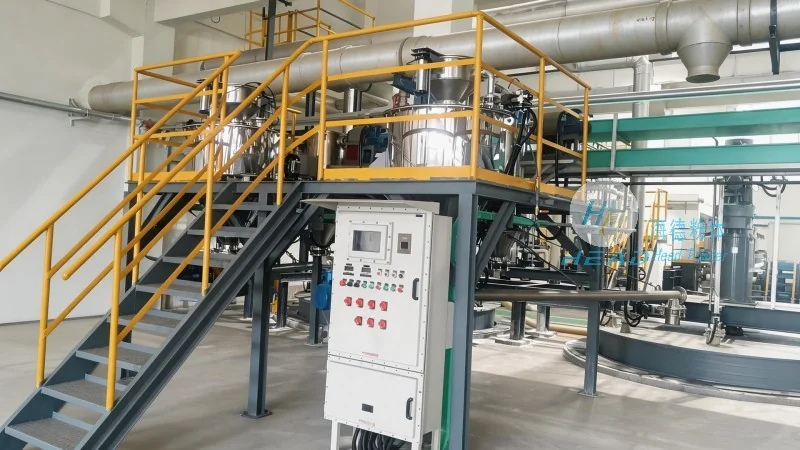
Customization and Scalability for Diverse Needs
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, offers a range of automatic quantitative powder transport systems tailored to meet the specific needs of different industries. The company's products are designed with flexibility in mind, allowing for customization based on the customer's requirements. Whether it's a small-scale system for laboratory use or a large-scale system for industrial production, HeadPowder provides solutions that can be scaled to fit the application. The systems are engineered to handle various powder characteristics, including different particle sizes, densities, and flowability, ensuring optimal performance. The company's commitment to quality and innovation is reflected in the advanced technology and robust construction of their equipment. By working closely with clients, HeadPowder ensures that the final solution not only meets but exceeds the expectations for precision, reliability, and efficiency. This approach has made HeadPowder a trusted partner for businesses seeking to enhance their powder handling capabilities.
Conclusion and Future Outlook
Automatic quantitative powder transport systems play a vital role in modern industrial operations, providing the precision and efficiency needed to handle powders reliably. The principles and features discussed highlight the advanced technology and practical applications that make these systems indispensable in various industries. As industries continue to demand higher standards of quality and productivity, the importance of such systems will only grow. The integration of automation and digital control in these systems ensures that they remain relevant and effective in the evolving industrial landscape. For businesses looking to improve their powder handling processes, investing in an automatic quantitative powder transport system from a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. can lead to significant benefits in terms of accuracy, efficiency, and overall operational performance.