

Operation Process and Working Principle of Cement Fly Ash Mineral Powder Pneumatic Conveying System
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, installation, and maintenance of advanced pneumatic conveying systems tailored for handling cement fly ash and other mineral powders. These systems are crucial in modern industrial applications, ensuring efficient material transport while maintaining product quality and operational safety.
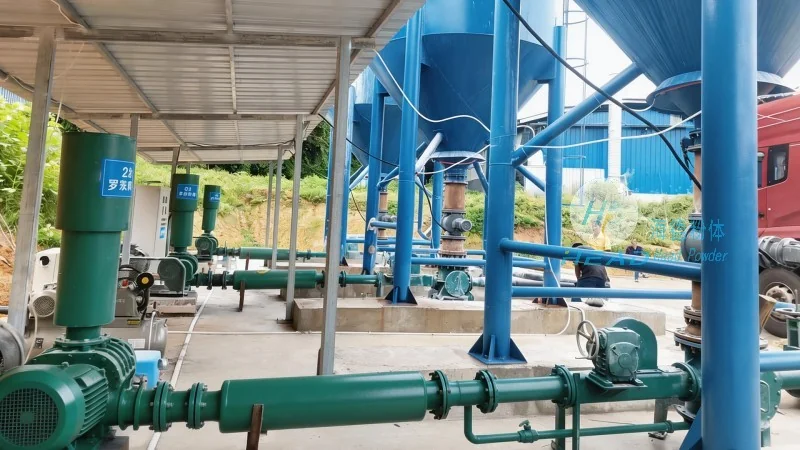
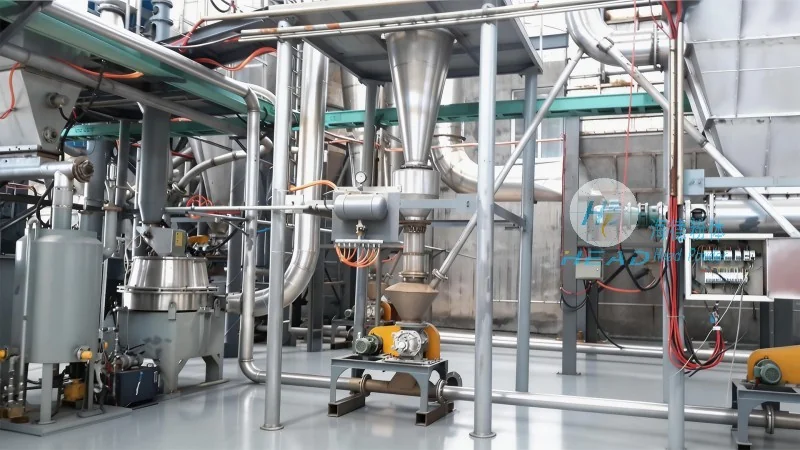
Working Principle of the Pneumatic Conveying System
The core of the system involves the use of air as the conveying medium to transport bulk powders through a network of pipes. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into a pipeline. A blower or compressor generates the necessary airflow, creating a pressure differential that propels the powder particles forward. The system may employ different conveying modes, such as dilute-phase or dense-phase, depending on the material characteristics and application requirements. Dilute-phase conveying uses higher air velocities to move the material in a dispersed state, while dense-phase conveying employs lower velocities with higher air-to-material ratios to ensure gentle handling and prevent particle degradation.
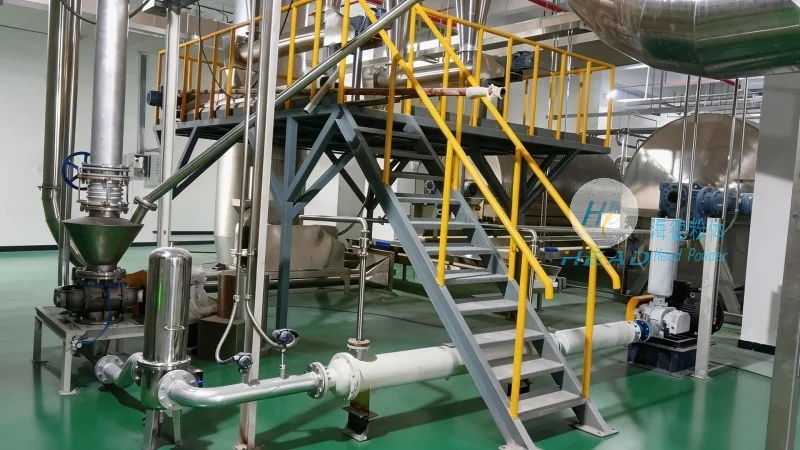
Operation Process of the System
The operation of the pneumatic conveying system for cement fly ash and mineral powders involves several key steps. First, the material is stored in a silo or hopper, from which it is fed into the conveying line via a rotary valve or screw feeder. The feeder controls the flow rate to match the system's capacity. The blower then starts, generating the required airflow to transport the material. As the powder travels through the pipeline, it may pass through various components like bends, filters, or separators to maintain system efficiency and prevent blockages. At the destination, the material is discharged into a receiving hopper or storage tank. The system's control panel monitors parameters such as pressure, flow rate, and air temperature, allowing for real-time adjustments to optimize performance and ensure consistent operation.
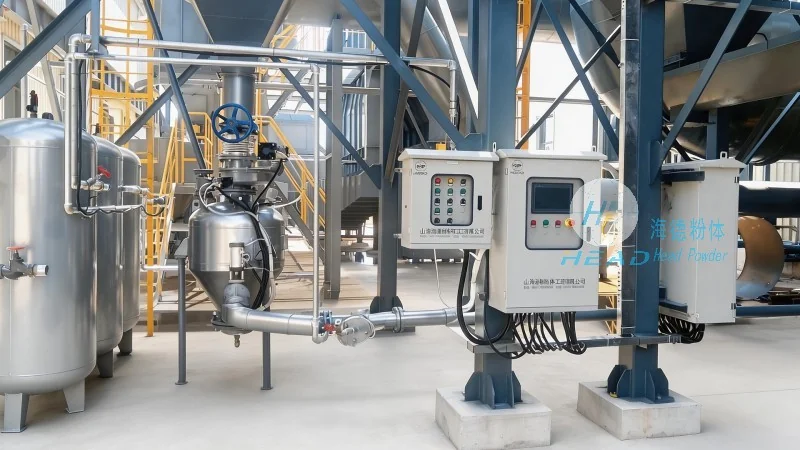
Key Features and Benefits
HeadPowder's pneumatic conveying systems for cement fly ash and mineral powders offer several advantages. These include high efficiency in material transport, reduced labor costs due to automated operation, and improved safety by minimizing manual handling of powders. The systems are designed to handle various particle sizes and moisture contents, ensuring compatibility with different industrial processes. Additionally, the use of air as the conveying medium eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and extending the system's lifespan. The systems also contribute to environmental benefits by reducing dust emissions and improving overall operational hygiene.