

Operation Process and Working Principle of Ash Material Conveying System Equipment
For industrial facilities dealing with ash material handling, the efficiency and reliability of the conveying system are critical to overall operational performance. The ash material conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is designed to meet the demanding requirements of modern waste management and material transport applications. This system integrates advanced engineering principles and robust construction to ensure safe, efficient, and continuous operation in various industrial settings.
System Overview and Core Components
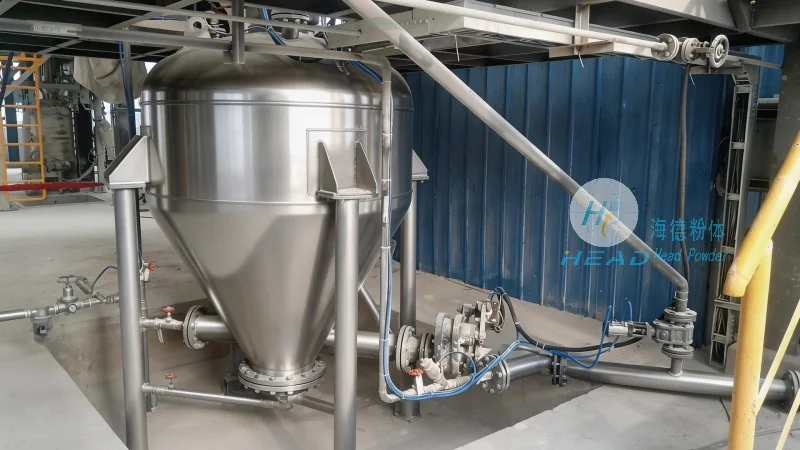
The ash material conveying system is a comprehensive solution that includes key components such as feed hoppers, conveyor belts, drive mechanisms, and control systems. Each component is engineered to work in harmony, ensuring seamless material flow from the source to the disposal or processing point. The system is built with durability in mind, using high-quality materials that can withstand the abrasive nature of ash and other similar materials. This design minimizes maintenance needs and maximizes operational uptime, which is essential for maintaining productivity in industrial operations.
Operation Process: Step-by-Step Workflow
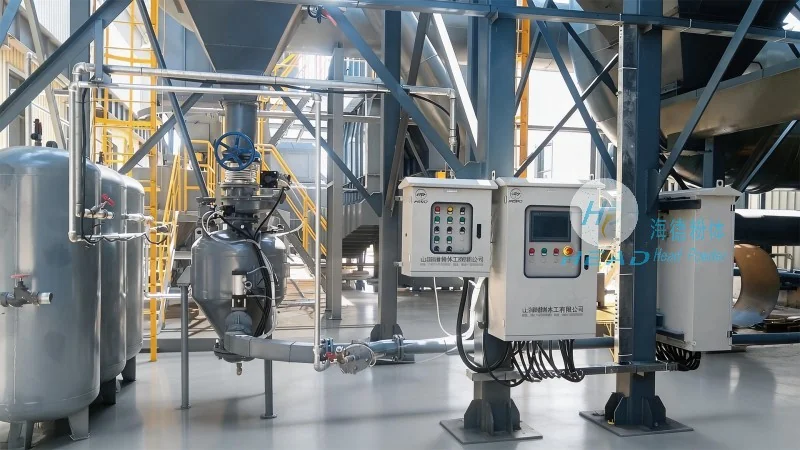
The operation of the ash material conveying system follows a systematic workflow that ensures consistent and reliable material transport. The process begins with the ash being deposited into the feed hopper, where it is collected and prepared for transport. From the hopper, the material is transferred to the conveyor belt via a series of rollers or feed mechanisms. The conveyor belt, powered by an electric motor and drive system, moves the ash through the system at a controlled speed. As the material travels along the belt, it is guided by idlers and tensioning devices to maintain proper alignment and prevent slippage. At the discharge end, the ash is released into the designated container or processing unit. The entire process is monitored by an integrated control system that adjusts speed and flow based on real-time conditions, ensuring optimal performance and preventing system overload or blockages.
Working Principle: Mechanical and Control Integration
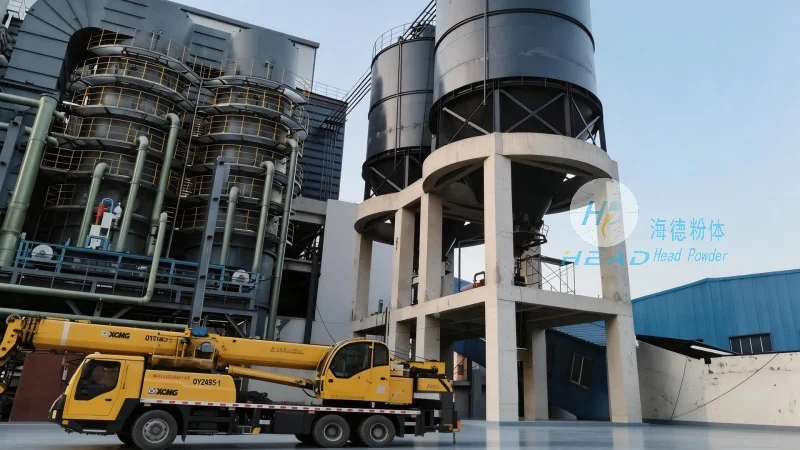
The working principle of the ash material conveying system combines mechanical power transmission with advanced control technology to achieve precise material handling. The core mechanism involves the use of a belt conveyor, where the ash is carried on the surface of the belt. The drive system, typically an electric motor connected to a gearbox, provides the necessary torque to move the belt at a consistent speed. The control system, which may include sensors and programmable logic controllers (PLCs), monitors parameters such as belt tension, speed, and material level. These sensors send signals to the PLC, which adjusts the motor speed or other parameters to maintain optimal operation. For example, if the material level in the hopper increases, the control system may increase the conveyor speed to prevent overflow. Conversely, if the material flow decreases, the system may reduce speed to avoid belt damage. This integration of mechanical and electronic components ensures that the system operates efficiently and safely under varying conditions.
Technical Advantages and Applications
The ash material conveying system offers several technical advantages that make it suitable for a wide range of industrial applications. One of the key advantages is its high capacity and continuous operation, which is ideal for large-scale waste management facilities. The system's robust construction and use of wear-resistant materials reduce maintenance costs and extend the service life of the equipment. Additionally, the system's modular design allows for easy installation and customization to fit specific site requirements. These features make the system a reliable choice for industries such as power plants, cement factories, and waste treatment facilities, where efficient ash handling is crucial for operational efficiency and environmental compliance.
Conclusion: Reliable Solution for Ash Material Handling
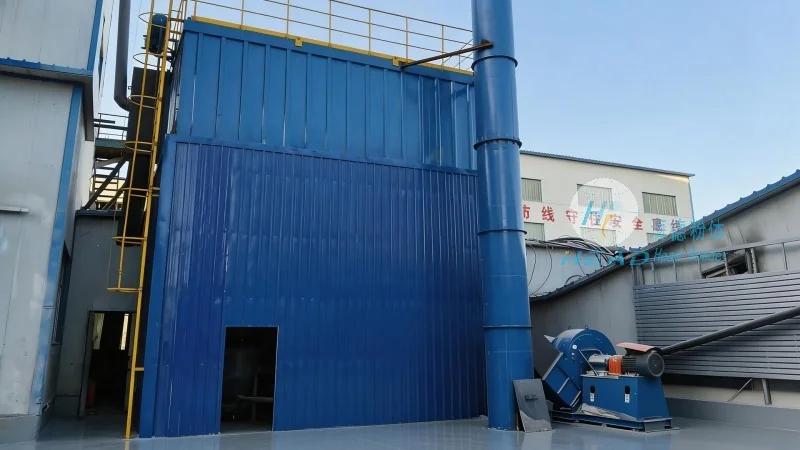
Shandong HeadPowder Engineering Co., Ltd. provides a high-performance ash material conveying system that combines advanced technology with durable construction to meet the demands of modern industrial applications. The system's operation process and working principle are designed to ensure efficient, safe, and reliable material transport, while its technical advantages make it a cost-effective solution for various industries. By integrating mechanical and control systems, the equipment maintains optimal performance under varying conditions, reducing downtime and operational costs. For facilities requiring reliable ash handling solutions, the ash material conveying system from HeadPowder is a proven choice that enhances operational efficiency and supports sustainable waste management practices.