

Operation Process and Working Principle of Stone Coal Material Handling System Equipment
Stone coal material handling systems are essential components in industrial operations, particularly in environments where the transportation of stone coal is required. These systems are designed to efficiently move stone coal from one location to another, ensuring smooth and continuous material flow. The equipment used in such systems is engineered to handle the specific characteristics of stone coal, including its size, density, and abrasive properties. By understanding the operation process and working principles of these systems, users can better appreciate their functionality and the benefits they offer in industrial applications.
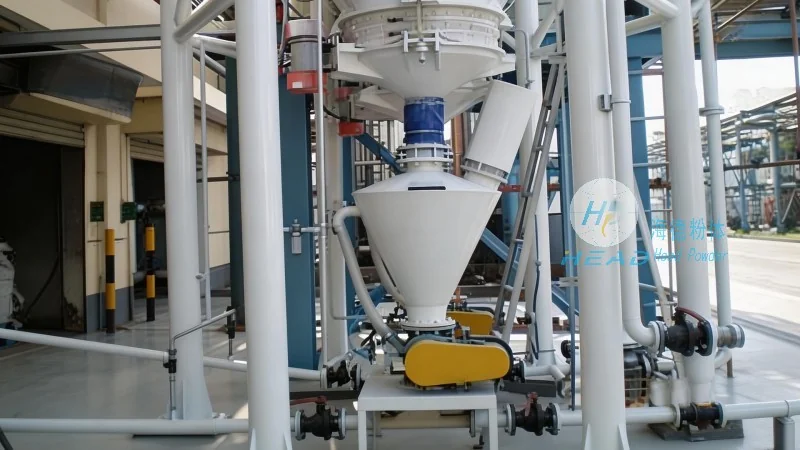
About Shandong HeadPowder Engineering Co., Ltd.
Headpowder, the professional manufacturer behind these advanced material handling systems, is a leading company based in Shandong, China. With years of experience in the engineering and manufacturing of industrial equipment, Headpowder specializes in providing high-quality solutions for material handling challenges. The company's commitment to innovation and quality has established it as a trusted name in the industry, delivering reliable and efficient equipment that meets the diverse needs of its clients. Headpowder's facilities and expertise are dedicated to developing and producing top-tier material handling systems, ensuring that customers receive products that are both effective and durable.
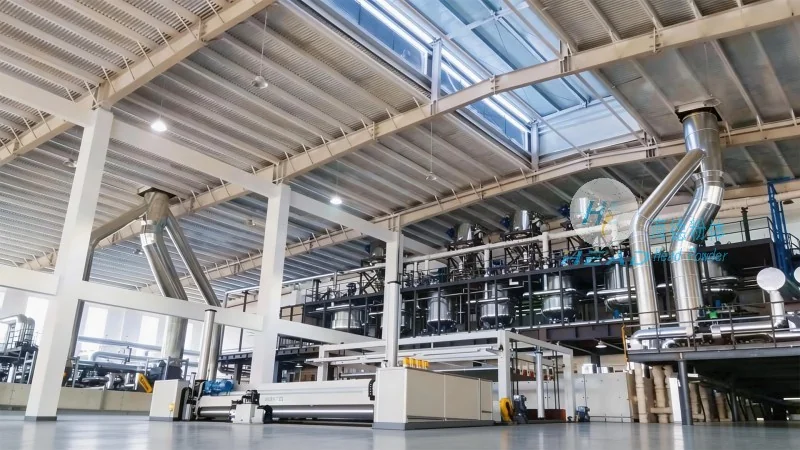
Key Components of the Stone Coal Material Handling System
The stone coal material handling system typically consists of several key components that work together to facilitate the transportation of stone coal. These components include feeders, conveyors, and control systems, each playing a crucial role in the overall operation. The feeders are responsible for uniformly feeding the stone coal into the system, ensuring a consistent flow rate. The conveyors, which may be of various types such as belt conveyors or screw conveyors, then transport the stone coal through the system. Control systems monitor and regulate the operation of these components, maintaining optimal performance and preventing issues such as blockages or overloads. Each component is carefully designed to handle the specific characteristics of stone coal, ensuring efficient and safe operation.
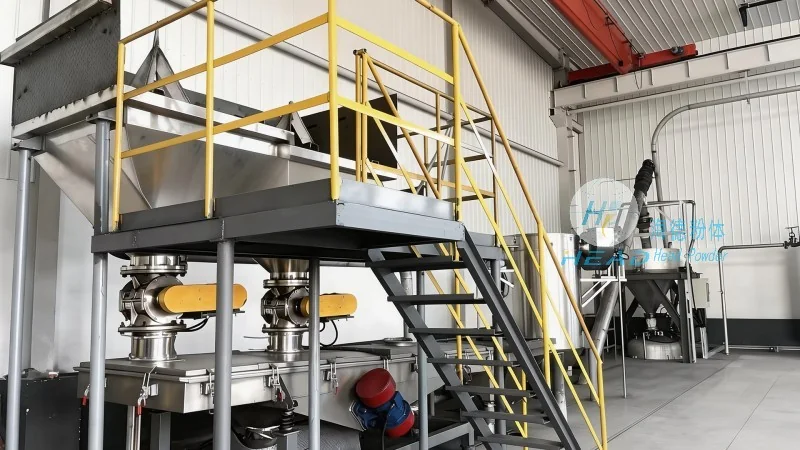
Operation Process of the Stone Coal Material Handling System
The operation process of the stone coal material handling system begins with the intake of stone coal. The material is fed into the system through a hopper or feeder, where it is then transported to the conveyor. The conveyor moves the stone coal along its path, possibly elevating it to a higher level or transporting it horizontally. As the stone coal moves through the system, it may pass through additional components such as screens or classifiers, which can be used to separate different sizes of stone coal. The system is equipped with sensors and controls that monitor the flow rate and position of the material, ensuring that the operation remains stable and efficient. When the stone coal reaches its destination, it is discharged from the system, completing the transportation process. The entire operation is designed to be continuous and automated, minimizing the need for manual intervention and maximizing productivity.
Working Principle of the Stone Coal Material Handling System
The working principle of the stone coal material handling system is based on the mechanical movement of the material through the system. The feeders use gravity or mechanical force to move the stone coal into the conveyor. The conveyor, typically a belt conveyor, uses friction to move the material along its surface. The speed and tension of the belt are carefully controlled to ensure that the stone coal is transported at an optimal rate without causing excessive wear or damage. The control system uses sensors to detect the level of material in the hopper and the speed of the conveyor, adjusting the feed rate as needed to maintain a consistent flow. This closed-loop control system ensures that the operation is stable and efficient, even under varying load conditions. The system is also designed to handle abrasive materials like stone coal, with components such as the conveyor belt and rollers being made of durable materials to withstand the wear and tear caused by the material.
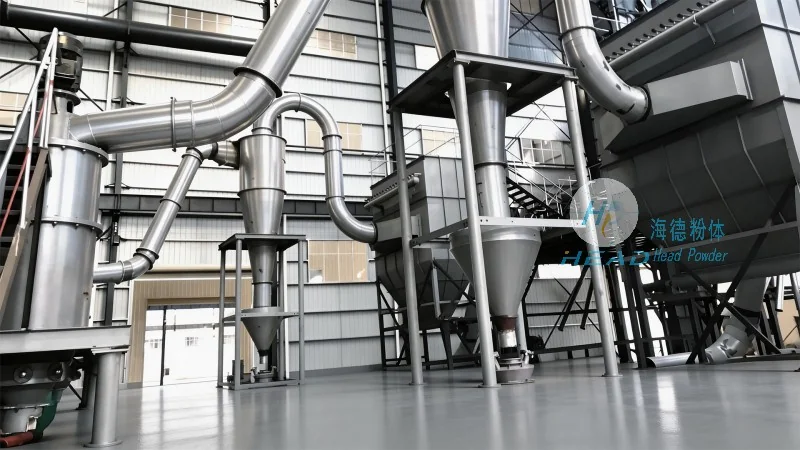
Benefits and Applications of the Stone Coal Material Handling System
The stone coal material handling system offers numerous benefits in industrial applications. Its efficient design allows for the continuous and reliable transportation of stone coal, reducing downtime and increasing productivity. The system's ability to handle abrasive materials makes it suitable for a wide range of industries, including mining, construction, and power generation. The automated operation reduces the need for manual labor, improving safety and reducing labor costs. Additionally, the system's modular design allows for easy integration with other industrial equipment, making it a versatile solution for various material handling needs. The system is also designed to be energy-efficient, minimizing operational costs while maintaining high performance. Overall, the stone coal material handling system is a critical component in modern industrial operations, providing an effective and reliable solution for the transportation of stone coal.