

Operation Process and Working Principle of Soda Ash Material Pneumatic Conveying Line
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and implementation of advanced pneumatic conveying systems tailored for handling soda ash materials. These systems are engineered to efficiently transport bulk soda ash from storage silos or production lines to processing facilities, ensuring smooth and reliable material flow in industrial applications.
Characteristics of Soda Ash Materials and Their Impact on Conveying Systems
Soda ash, also known as sodium carbonate (Na₂CO₃), is a white crystalline powder widely used in various industries, including glass manufacturing, chemical production, and water treatment. Its physical properties, such as fine particle size, hygroscopic nature, and potential for dust generation, require specialized pneumatic conveying solutions to maintain material integrity and operational safety. The material's density and flow characteristics also influence the selection of conveying methods, such as dilute-phase or dense-phase systems, to optimize performance and minimize equipment wear.
Operation Process of the Pneumatic Conveying Line
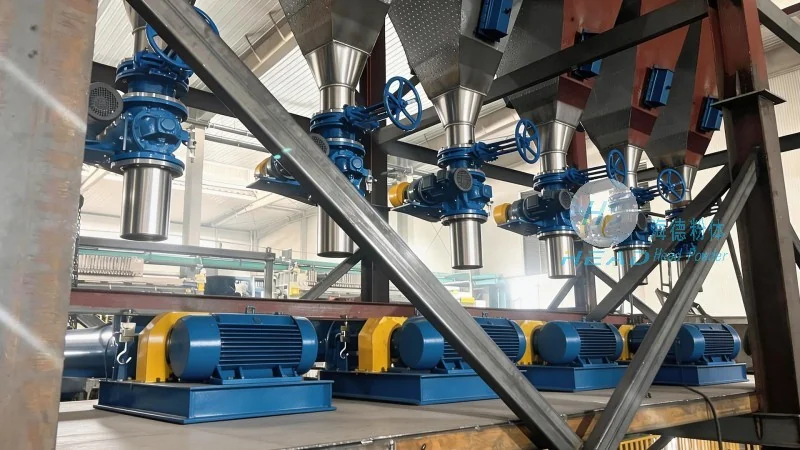
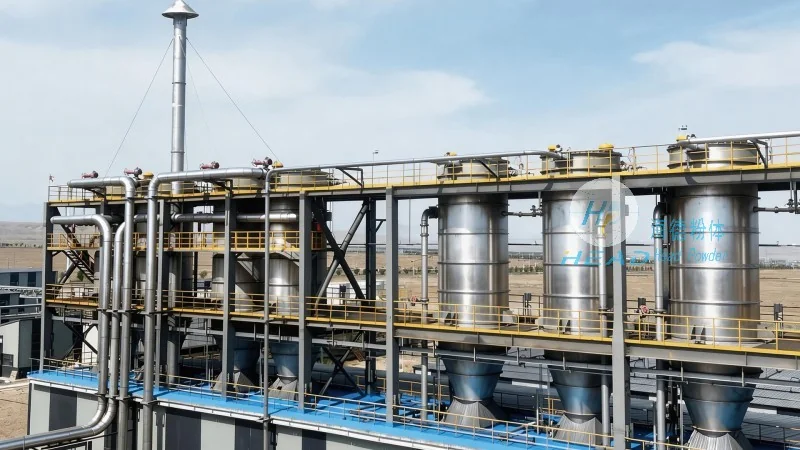
The operation of a soda ash material pneumatic conveying line typically involves several key steps, each designed to ensure efficient and safe material transport. The process begins with the material being fed from a storage silo or hopper into the conveying system. A blower or compressor generates the necessary air pressure to create a flow of air and material through the pipeline. The material is then suspended in the air stream and transported to the destination point, such as a processing unit or a storage tank. At the receiving end, the material is separated from the air using a cyclone separator or a filter, and the air is either recirculated or discharged safely. Throughout the process, the system monitors pressure, flow rate, and material level to maintain optimal performance and prevent blockages or other operational issues.
Working Principle of the Pneumatic Conveying System
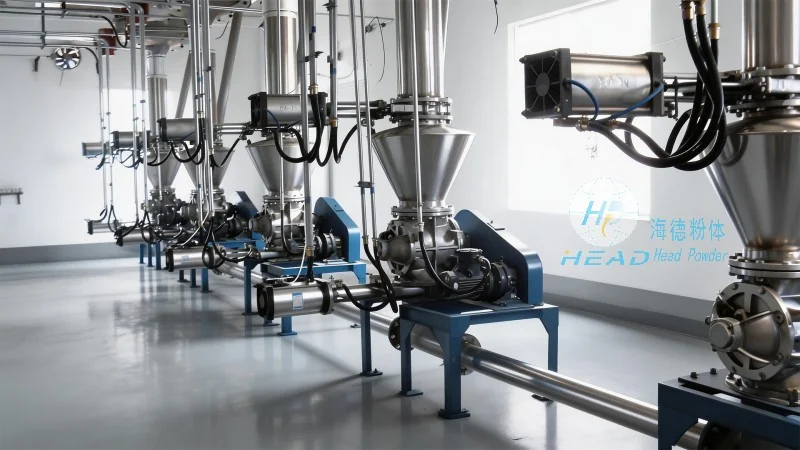
The core working principle of the soda ash pneumatic conveying line relies on the interaction between air and the material particles. In a dilute-phase system, the material is carried in a low concentration of particles within the air stream, allowing for high-speed transport over long distances. The system uses a positive displacement blower to create a consistent air flow, which pulls the material into the pipeline through a feeder. The feeder, often a rotary valve or a star feeder, controls the material flow rate to match the air velocity, ensuring stable operation. In a dense-phase system, the material is conveyed at a higher concentration, with the air flow used to push the material through the pipeline, reducing the risk of material degradation and blockages. The system's design, including the type of blower, pipeline diameter, and feeder design, is tailored to the specific characteristics of soda ash to achieve efficient and reliable transport.
Key Features and Advantages of the System
HeadPowder's soda ash material pneumatic conveying lines offer several advantages that make them ideal for industrial applications. These systems are designed to handle the hygroscopic and fine-particle nature of soda ash, preventing material clumping and ensuring consistent flow. The use of high-quality materials and components, such as stainless steel pipelines and corrosion-resistant blower parts, enhances durability and reduces maintenance costs. The system's modular design allows for easy integration with existing production lines, minimizing downtime during installation. Additionally, the automated control system provides real-time monitoring and adjustment, ensuring optimal performance and reducing the risk of operational errors.
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer specializing in the development of advanced pneumatic conveying systems. With years of experience in the industry, the company has built a strong reputation for delivering high-quality, reliable solutions tailored to the specific needs of its clients. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses in various industries, including chemical manufacturing, glass production, and water treatment. HeadPowder's team of experts works closely with clients to understand their requirements and provide customized solutions that meet their operational and performance goals.