

What is an Organic Salt Material Pneumatic Conveyor? And What Are Its Design Principles?
Organic salt material pneumatic conveyors are specialized equipment designed for the efficient and safe transportation of organic salt materials in industrial settings. These systems utilize pneumatic principles to move bulk materials through a network of pipes and ducts, offering advantages such as minimal contamination, reduced labor costs, and the ability to handle materials in enclosed environments. The design of these conveyors is tailored to the unique properties of organic salt materials, ensuring optimal performance and reliability.
Key Components of Organic Salt Pneumatic Conveyors
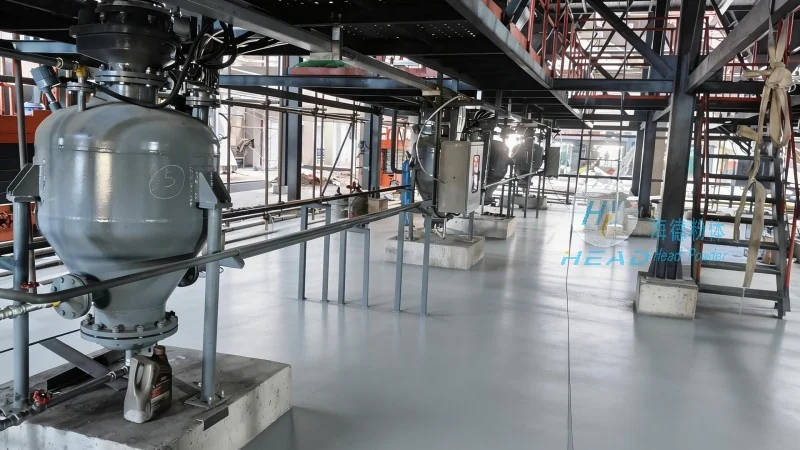
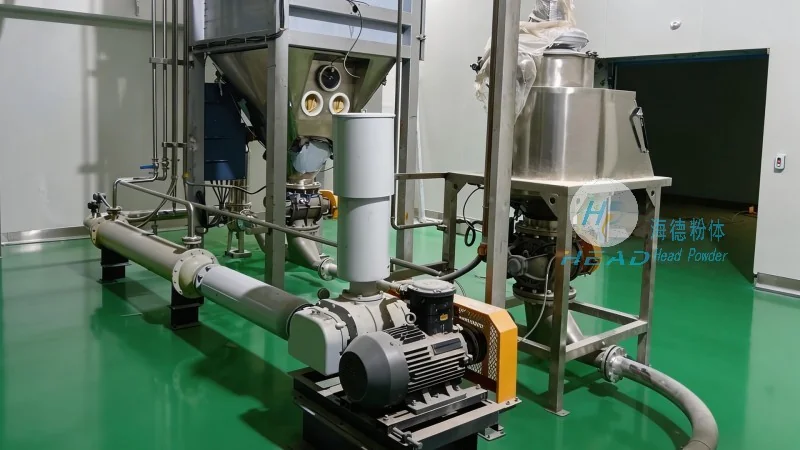
The core components of an organic salt material pneumatic conveyor include the material hopper, feeder, air compressor, conveying pipes, and discharge unit. The material hopper is responsible for storing the organic salt, while the feeder controls the flow rate of the material into the system. The air compressor generates the necessary air pressure to propel the material through the pipes. The conveying pipes are typically made of durable materials like stainless steel or corrosion-resistant alloys to withstand the chemical properties of organic salts. The discharge unit collects the material at the end of the conveyor system.
Design Principles for Organic Salt Material Conveyors
The design principles for organic salt material pneumatic conveyors focus on several critical factors: material flow rate, air pressure requirements, and system efficiency. Engineers must consider the bulk density and flow characteristics of the organic salt to determine the appropriate air velocity and pressure needed for effective conveying. The system is designed to maintain a consistent flow of material, minimizing blockages and ensuring smooth operation. Additionally, the design incorporates features to prevent material degradation, such as avoiding high temperatures or excessive friction that could affect the quality of the organic salt.
Advantages of Using Organic Salt Pneumatic Conveyors
Organic salt material pneumatic conveyors offer several advantages over traditional mechanical conveyors. One of the primary benefits is the ability to handle materials in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important for organic salts, which may be prone to dusting or have health hazards associated with inhalation. Another advantage is the reduced need for maintenance, as pneumatic systems have fewer moving parts compared to mechanical systems. This leads to lower operational costs and increased uptime. Furthermore, the flexibility of pneumatic conveyors allows for easy integration into existing production lines, enabling seamless material transfer between different stages of processing.

Applications in Industrial Settings
Organic salt material pneumatic conveyors are widely used in various industrial applications, including food processing, pharmaceutical manufacturing, and chemical production. In the food industry, these systems are used to transport organic salts like sodium chloride or potassium chloride, ensuring that the materials remain free from contamination and maintain their quality. In pharmaceutical manufacturing, the closed system design is crucial for maintaining sterile conditions and preventing cross-contamination. In chemical production, the ability to handle corrosive or abrasive organic salts is essential, and pneumatic conveyors provide a reliable solution for these challenging materials.
Customization and Scalability
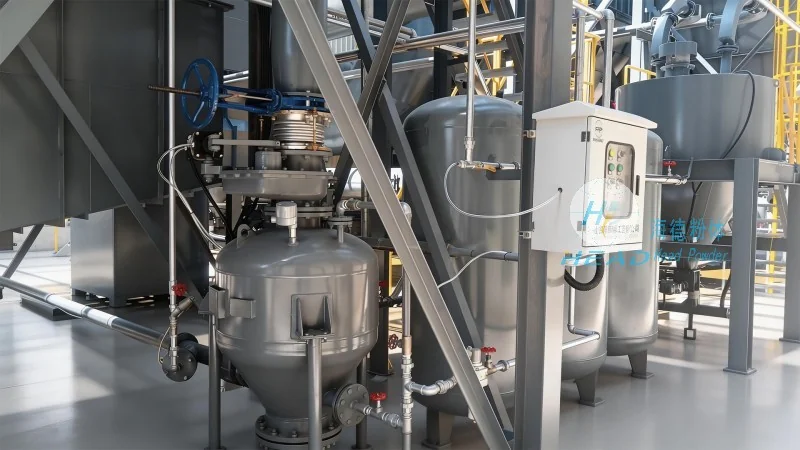
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized organic salt material pneumatic conveyors to meet the specific needs of clients. The company, commonly known as headpowder, offers a range of solutions tailored to different production capacities and material types. Their engineering team works closely with clients to understand their operational requirements and develop a conveyor system that maximizes efficiency and performance. The conveyors can be scaled to accommodate small-scale operations as well as large industrial facilities, ensuring that clients receive a solution that fits their unique needs.
Quality Assurance and Maintenance
HeadPowder places a strong emphasis on quality assurance and maintenance for their organic salt material pneumatic conveyors. The company uses high-quality materials and components to ensure the durability and longevity of the equipment. Regular maintenance is recommended to keep the system operating at peak performance, including checking air pressure, cleaning the conveying pipes, and inspecting the feeder and discharge units. By following proper maintenance procedures, clients can extend the lifespan of their conveyor systems and minimize downtime. The company also provides technical support and training to clients to ensure that they can operate and maintain the equipment effectively.