

Working Principle and Features of Bulk Storage Material Handling Equipment
For industrial operations that involve the storage and movement of bulk materials, efficient material handling equipment is crucial. This article explores the working principle and key features of bulk storage material handling equipment, providing insights into how these systems enhance operational efficiency and reliability in various industrial settings.
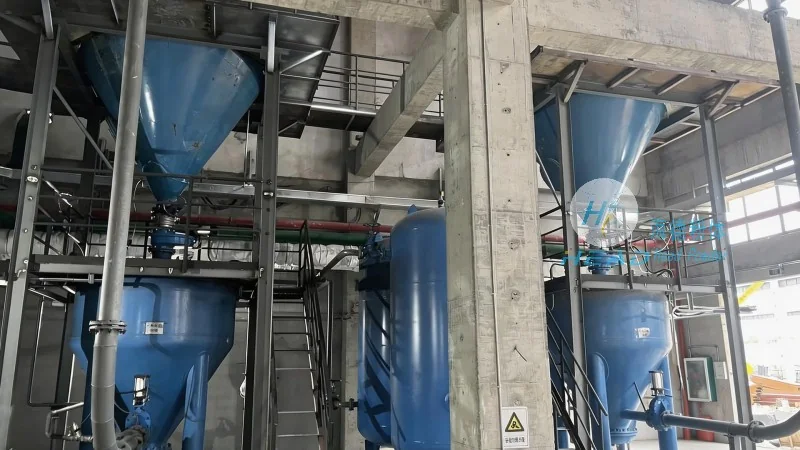
Introduction to Bulk Storage Material Handling Equipment
Bulk storage material handling equipment is designed to manage the flow of bulk materials from storage to processing or distribution points. These systems are integral to industries such as mining, agriculture, food processing, and manufacturing, where large volumes of raw materials need to be handled safely and efficiently. The equipment typically includes components like silos, hoppers, conveyors, and feeding mechanisms, all working in tandem to ensure smooth material transfer.
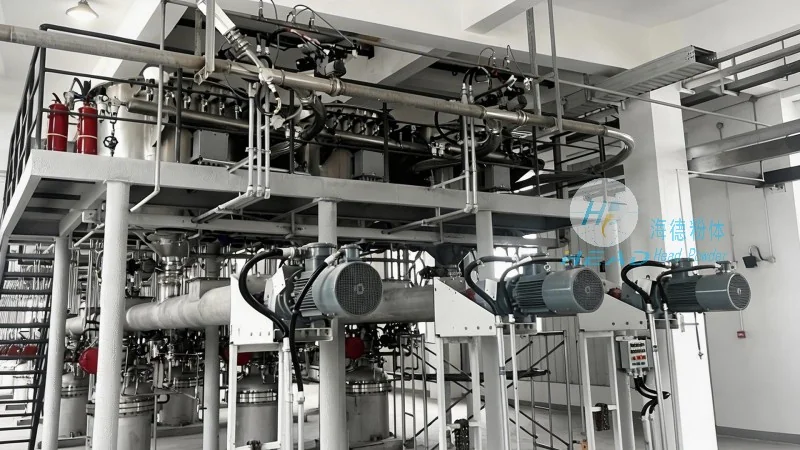
Working Principle of the Equipment
The core working principle of bulk storage material handling equipment revolves around the controlled movement of bulk materials through a series of mechanical and hydraulic systems. The process generally begins with the storage of materials in a silo or hopper, where the material is held under controlled conditions. When material is needed for processing or transport, a feeding mechanism, such as a rotary valve or screw conveyor, is activated to release the material into a conveyor system. The conveyor then transports the material to the desired location, such as a processing unit or a loading area. The entire system is often equipped with sensors and control systems to monitor flow rates, levels, and operational status, ensuring optimal performance and preventing issues like overfilling or blockages.
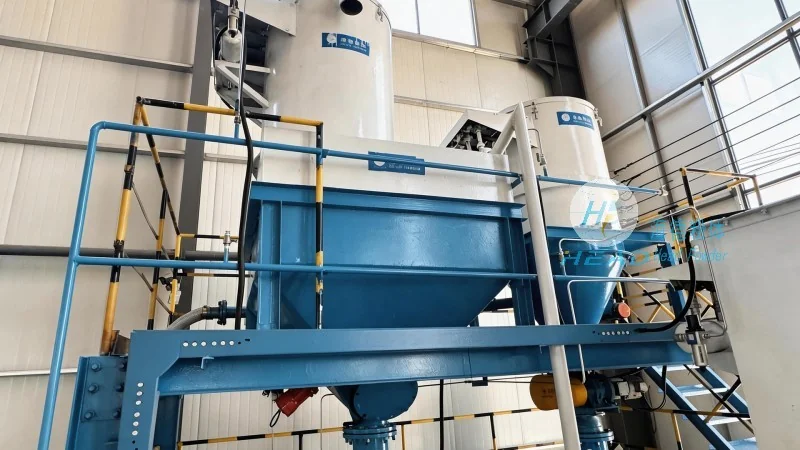
Key Features of the Equipment
Modern bulk storage material handling equipment is characterized by several key features that enhance its functionality and reliability. One of the primary features is the use of durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the harsh conditions of bulk material handling. This ensures longevity and minimal maintenance. Another important feature is the integration of advanced control systems, including programmable logic controllers (PLCs) and sensors, which allow for precise control over material flow, level monitoring, and system diagnostics. Additionally, many systems are designed with modular components, enabling easy maintenance and upgrades without disrupting overall operations. The equipment also often includes safety features like emergency stop buttons, overload protection, and interlocks to prevent accidents and ensure operator safety.
Application Scenarios and Benefits
Bulk storage material handling equipment is widely used in various industrial applications. In the mining industry, it is used to transport ore from storage silos to processing plants. In agriculture, it helps in the storage and distribution of grains and other bulk crops. In food processing, it ensures the safe and hygienic handling of raw materials, maintaining product quality. The benefits of these systems include increased productivity through automated material handling, reduced labor costs, improved safety due to automated controls, and enhanced material flow control. Additionally, the equipment helps in minimizing material loss and contamination, which is critical in industries where product quality is paramount.
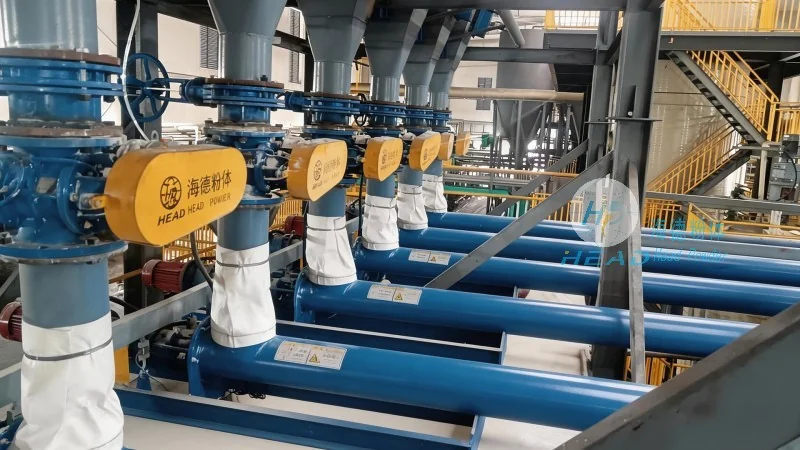
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of bulk storage material handling equipment. The company is based in Shandong, China, and has established itself as a trusted provider of high-quality material handling solutions for various industrial sectors. HeadPowder specializes in designing and manufacturing equipment tailored to the specific needs of clients, ensuring that each system is optimized for efficiency, durability, and safety. The company’s commitment to innovation and customer satisfaction has made it a preferred choice for businesses seeking reliable material handling solutions. With a focus on research and development, HeadPowder continuously improves its products to meet the evolving demands of the industry, providing comprehensive support from design and installation to maintenance and after-sales service.