

Working Principle and Features of Intelligent Unpacking Material Handling Equipment
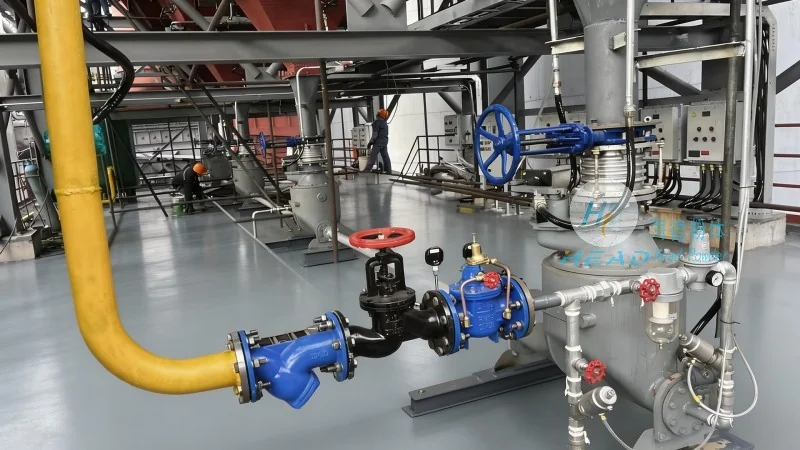
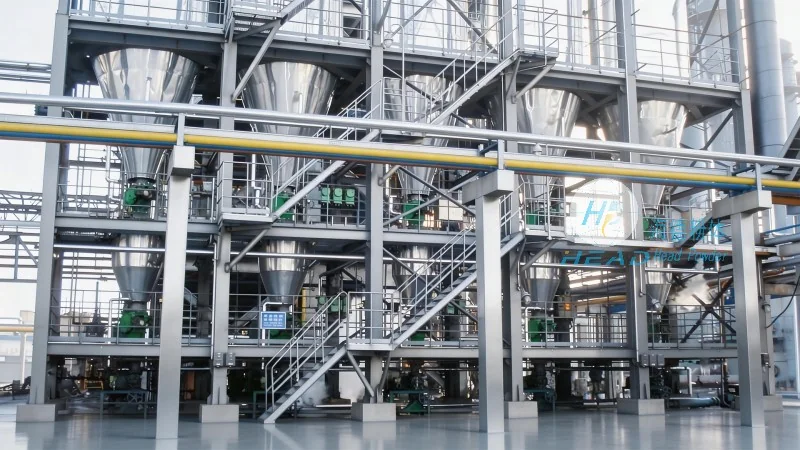
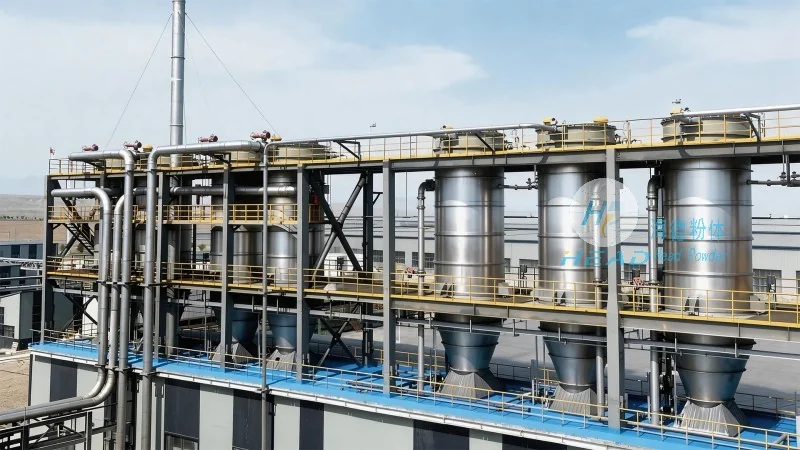
Intelligent unpacking material handling equipment operates through a series of integrated processes designed to efficiently transfer bulk materials from their original packaging to subsequent processing or storage stages. The core working principle involves the sequential steps of material reception, unpacking, sorting, and conveyance. Upon arrival at the equipment, bulk materials are typically fed into a hopper or loading chamber. This initial stage ensures a consistent flow of material into the system. The equipment then utilizes advanced mechanisms, such as automated cutting, tearing, or opening of packaging, to release the internal contents. This unpacking process is often facilitated by sensors and actuators that detect packaging types and adjust the operation accordingly. Once the material is unpacked, it is transferred to a conveyor system or sorting mechanism. The conveyance stage may involve belt conveyors, roller conveyors, or automated guided vehicles (AGVs), depending on the specific application and material characteristics. The entire process is controlled by a centralized system, which monitors parameters like flow rate, temperature, and material density to maintain optimal performance. This integrated approach ensures that the equipment can handle a wide range of materials, including powders, granules, and bulk solids, with high efficiency and minimal human intervention.
Key Features of Intelligent Unpacking Material Handling Equipment
Intelligent unpacking material handling equipment is characterized by several advanced features that enhance its functionality and operational efficiency. One of the primary features is its adaptability to various packaging types. The equipment is equipped with modular components that can be easily reconfigured to handle different packaging materials, such as plastic bags, cardboard boxes, or metal drums. This flexibility reduces downtime and maintenance costs, as operators can switch between different configurations without extensive retooling. Another notable feature is the integration of real-time monitoring and control systems. Advanced sensors and data acquisition systems provide continuous feedback on key performance indicators (KPIs), including material flow rate, unpacking efficiency, and system health. This data is processed by a central control unit, which can automatically adjust operational parameters to optimize performance. The equipment also incorporates safety features, such as emergency stop buttons, collision detection sensors, and automated shut-off mechanisms, to ensure operator safety and prevent equipment damage. Additionally, the system is designed for easy maintenance and service. Modular components allow for quick replacement of worn parts, reducing maintenance downtime. The equipment may also include self-diagnostic capabilities, which can identify potential issues and alert maintenance personnel before they escalate into major problems. These features collectively contribute to the high reliability and low operational costs of the intelligent unpacking material handling equipment.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of intelligent material handling solutions. With a strong commitment to innovation and quality, the company specializes in designing and manufacturing equipment tailored to the needs of various industries, including pharmaceuticals, food processing, and chemical manufacturing. HeadPowder's products are engineered to meet stringent industry standards and regulatory requirements, ensuring compliance with safety and environmental regulations. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder's team of engineers and technicians work closely with clients to understand their specific requirements and develop customized solutions that enhance operational efficiency and productivity. The company's focus on research and development ensures that its products remain at the forefront of technological advancements, providing clients with reliable and efficient material handling solutions.