

Working Principle and Features of Cathode Material Material Handling Equipment
For companies in the lithium battery industry, the efficient and reliable handling of cathode material is crucial to production efficiency and product quality. As a leading manufacturer of material handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-performance solutions for the transportation and processing of cathode materials. This article will explore the working principles and key features of our material handling equipment, offering insights into how these systems enhance operational efficiency in battery production lines.

Working Principle of Cathode Material Material Handling Equipment
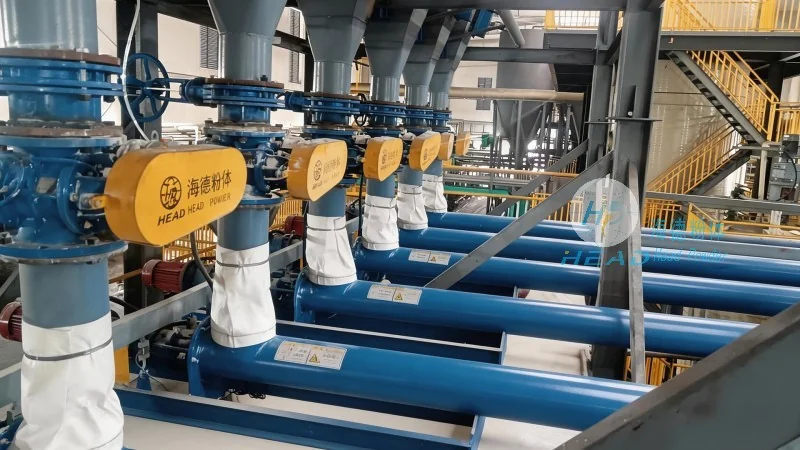
At the core of our material handling systems is a design that integrates advanced engineering with practical application. The equipment typically operates through a combination of mechanical components, such as conveyor belts, screw conveyors, and vibrating feeders. These components work in tandem to transport cathode powders from storage silos to processing units, ensuring a smooth and continuous flow of material. The working principle involves several key steps: material is first fed into the system from a hopper or storage tank, then conveyed through a series of channels or tubes, and finally delivered to the next stage of production. This process is often controlled by a programmable logic controller (PLC), which monitors and adjusts the speed and direction of the conveyor based on real-time production needs. The system is designed to minimize material degradation and loss, maintaining the integrity of the cathode material throughout the handling process.
Key Features of the Material Handling Equipment
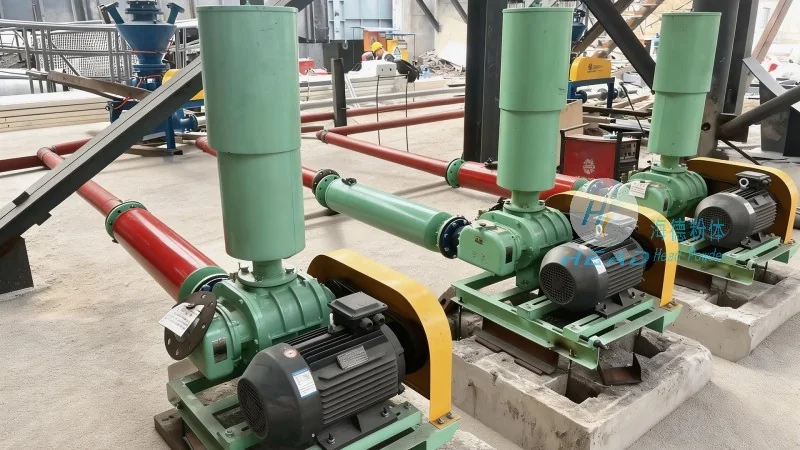
Our material handling equipment for cathode materials is engineered with several distinctive features that set it apart in the industry. First, the equipment is built with high-quality materials, such as stainless steel and corrosion-resistant alloys, to withstand the harsh chemical environment of battery production. This ensures durability and long service life, reducing maintenance costs for our clients. Second, the system incorporates advanced control technology, including sensors and automation controls, which enable precise control over material flow and prevent overloading or blockages. This not only enhances safety but also improves production consistency. Third, the design is modular and customizable, allowing us to adapt the equipment to the specific needs of different production lines. Whether it's a small-scale laboratory setup or a large-scale industrial production facility, our equipment can be tailored to meet the requirements. Additionally, the equipment is equipped with dust collection and filtration systems to maintain a clean and safe working environment, which is essential for both personnel and equipment. These features collectively contribute to a more efficient, reliable, and cost-effective material handling solution for cathode materials.
Application in Battery Production
The material handling equipment plays a vital role in the battery production process, particularly in the preparation of cathode materials. The smooth transport of raw materials, such as lithium cobalt oxide (LCO), lithium nickel manganese cobalt oxide (NMC), and other cathode powders, is critical for achieving uniform mixing and consistent battery performance. By ensuring that materials are delivered at the right speed and in the correct quantity, our equipment helps to minimize variations in product quality. This is especially important in the modern battery industry, where high energy density and long cycle life are key performance indicators. The equipment also supports the integration of automated production lines, allowing for seamless coordination between material handling and subsequent processing steps. This integration enhances overall production efficiency and reduces the risk of bottlenecks in the workflow. Furthermore, the equipment's ability to handle different types of cathode materials without degradation makes it a versatile solution for various battery chemistries, from lithium-ion to emerging technologies like solid-state batteries.
Advantages for Clients
For businesses operating in the battery sector, investing in high-quality material handling equipment from Shandong HeadPowder Engineering Co., Ltd. offers several advantages. The primary benefit is improved operational efficiency, as the equipment reduces downtime and increases the throughput of cathode materials. This directly translates to higher production output and better profitability. Additionally, the equipment's reliability minimizes maintenance interruptions, allowing for continuous operation and reducing the need for frequent repairs. The use of advanced technology also leads to better product quality, as the consistent handling of materials ensures uniformity in the final battery products. This can enhance the reputation of the company and open up new market opportunities. Furthermore, the modular design of our equipment allows for easy upgrades and modifications as production needs evolve, providing long-term value. The company's commitment to quality and customer service ensures that clients receive not only a product but also comprehensive support throughout the equipment's lifecycle. This includes technical assistance, maintenance services, and ongoing training to maximize the equipment's performance. By choosing our material handling equipment, clients can focus on their core business while we handle the complexities of material transport, ensuring a smooth and efficient production process.
Conclusion
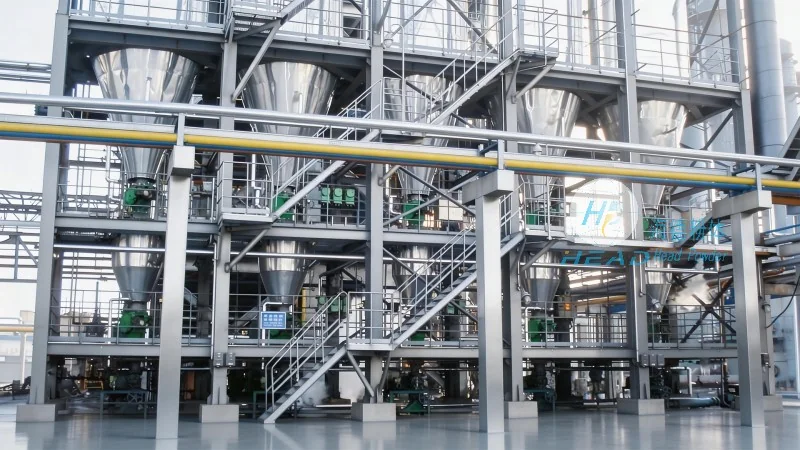
In conclusion, the working principle and features of cathode material material handling equipment from Shandong HeadPowder Engineering Co., Ltd. are designed to meet the demanding requirements of modern battery production. The integration of advanced mechanical and control systems, combined with high-quality materials and customization options, makes our equipment a reliable and efficient solution for transporting cathode materials. By enhancing production efficiency, ensuring product quality, and reducing operational costs, our material handling systems contribute to the success of battery manufacturers. As a trusted partner in the industry, we continue to innovate and provide tailored solutions that address the evolving needs of the battery sector. Whether you are a new entrant or an established player in the market, our equipment can help you achieve your production goals and stay competitive in the global battery industry.